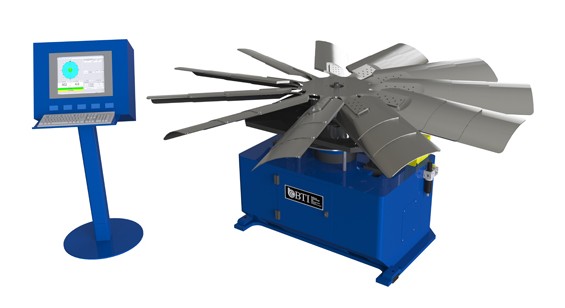
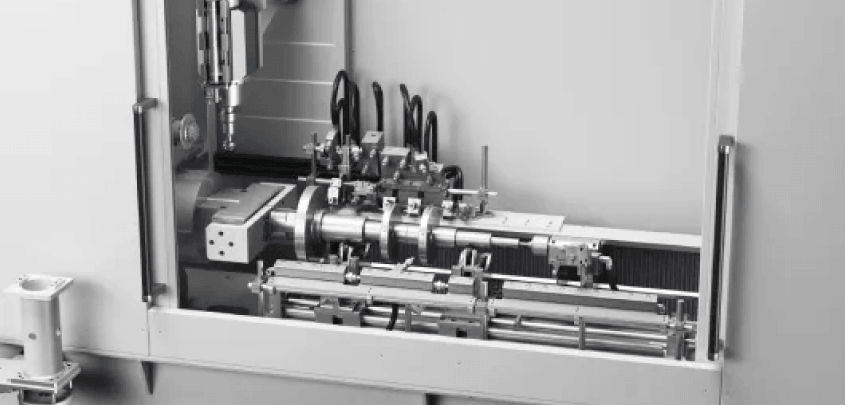
BTI engineers and manufactures a complete line of machine tools for all part types and sizes, as well as all production rates and levels of automation.
Balance Technology designs and builds purpose-built machines: machines that remove metal from a specific part, in a specific place, for a specific reason, usually because a measurement told them to. Manual, fully automated, or somewhere in between.
These are not general-purpose machining centers, and we do not compete with them. A machining center is built to do many things to many parts. A purpose-built machine tool is built to do one thing to one family of parts, faster, in less floor space, and with the measurement that governs the cut built into the same machine.
Machining That Answers to a Measurement
Most of the machine tools we build exist because a measurement has to be turned into a cut.
Balance correction machining. The balancer determines how much material to remove and where, and a correction station removes it by drilling, milling, grinding, punching or turning in the same machine, on the same fixture, followed by a verification spin. The cut is only as good as the axis it is referenced to, which is why correction is a machine tool problem and a measurement problem at the same time.
Mass centering. A forging is measured to find its true mass axis, then center drilled on that axis rather than on its nominal geometric one. Every subsequent machining operation then starts from the axis the part will actually spin about. On crankshafts in particular, this keeps counterweight machining inside its envelope and drastically reduces the correction the balancer has to make later.
Corrective machining after gaging. A gage measures the part and a machining station takes it to size, with the measurement closing the loop rather than a fixed program running open loop.
Straightening and runout correction. Measure, calculate, correct, verify: the same closed loop, executed by a press or peening head rather than a cutter. See shaft straighteners.
Special Purpose Machines
We also build machine tools that are simply dedicated rather than measurement-driven: an operation your part needs that no catalog machine does well, at a rate a general-purpose machine cannot reach.
- Dedicated drilling, milling, boring and tapping stations
- Center drilling machines
- Facing, chamfering and deburring machines
- Grinding and honing stations
- Broaching and keyway operations
- Slotting, notching and punching
- Multi-spindle stations where several features are cut simultaneously
- Machining stations integrated into automated assembly lines
Why a Purpose-Built Machine Instead of a Machining Center
Cycle time. A dedicated machine performs its operation without tool changes, without repositioning and without the generality that costs a machining center seconds on every cycle. On a high-volume part, seconds decide whether you need one machine or three.
Floor space and capital per part. One dedicated station doing one operation at rate is smaller and cheaper than a machining center doing the same work slower.
Integration with measurement. This is the real argument. When the machining is governed by a measurement, the measurement and the cut want to share a fixture, a datum scheme and a control system. Bolting a gage onto a machining center is a compromise; designing the two together is not.
The operator. A dedicated machine has a dedicated interface. Load, cycle, unload. The training burden is a fraction of a programmable machining center’s, which matters in plants where the workforce turns over.
Where a Machining Center Is the Better Answer
If your part mix is varied, your volumes are moderate, and the machining is not tied to an in-process measurement, buy a machining center. It will be cheaper, more flexible, and supportable by people other than us. We would rather tell you that at the start than build you a machine you will outgrow or underuse.
Purpose-built wins on stable, high-volume families, on tight cycle times, and above all where the cut is determined by a measurement made in the same machine.
How We Build Them
The fixture first. As with everything we build, the datum scheme comes before the station layout. A cut referenced to the wrong axis is wrong no matter how precisely it was executed, and on measurement-driven machining the fixture is what makes the measurement and the cut agree. Where the part drawing uses geometric dimensioning and tolerancing, the fixture is built to simulate the datums that drawing calls out.
Rigidity sized to the cut. Base, ways and spindle are specified for the actual cutting loads, not scaled from a similar machine.
Servo control of the axes that matter, so that correction amounts calculated by the measurement system are executed directly rather than approximated.
Chip and coolant management designed in from the start. On a combined measurement and machining machine this is not a detail. Chips and mist in a measurement station are how a good machine becomes an unreliable one.
Controls and data. One control system, one record per part, with machining parameters and measurement results in the same record.
What We Need to Quote One
- Part drawings, with datums and the tolerances on the features to be machined
- The operation required, and what governs it: a fixed program or a measurement
- Material, hardness and condition
- Part size, weight and the range across the family
- Required throughput and takt time
- Whether measurement and verification are required in the same machine
- How parts arrive and leave
- Floor space, utilities, and plant standards for controls and safety
Frequently Asked Questions
Do you build standalone machine tools, or only correction stations?
Both. Most of our machining work is part of a measurement-driven machine, but we build dedicated special purpose machines on their own where the application justifies it.
Can you add a machining station to a machine we already own?
Frequently. Adding automatic correction to a balancer that currently only measures is one of the more common upgrades we do. See BTI rebuilds and retrofits, or competitor rebuilds for machines built by others.
Which correction method should we use?
It depends on the material, the amount of correction, the surface you can remove from, and whether chips are acceptable.
- Drilling is fast and removes a lot
- Milling gives a controlled, cosmetically better result
- Grinding suits hardened surfaces
- Punching and riveting suit sheet and fabricated parts
- Weight addition suits parts you cannot cut into
We will recommend based on your part, and we will explain the tradeoff rather than just state a conclusion.
Can measurement and machining really share one machine without the chips causing problems?
Yes, when the machine is designed for it, with separated stations, sealed measurement areas, directed coolant and chip evacuation, and cleaning before measurement where the part demands it. It is a design problem with known solutions, and it is one of the reasons a combined machine should be designed as one machine rather than assembled from two.
Can you integrate a machining station into an assembly line?
Yes. Machining operations embedded in automated assembly systems, including sizing, facing, drilling after a press operation, are common in the machines we build.
Including static and dynamic balancing equipment, dimensional gages, mass centering equipment, eddy current crack detection systems, surface finish measurement equipment, NVH equipment (noise vibration and harshness), functional test stands, spinners, motor testers, and resonant frequency measurement systems.
We also engineer and manufacture specialized test systems, including torque-to-turn, backlash, end play, and destructive test equipment.
Additionally, BTI’s unique ability to combine the aforementioned technologies into one fully integrated system enables our clients to reduce capital expenditures, increase product quality, and minimize floor space requirements. There is no need for costly conveyors and escapements to connect independent machines together; nor do you need to train operators on multiple machines. There is one seamless, easy-to-use operator interface with unprecedented networking, statistical, and diagnostic capability.
Whether you need a fully integrated, combined technology system (e.g., a balancer/gage/NVH combo) or an independent machine tool, let our team of mechanical, electrical, and software engineers design and build a configured-to-order system for you.
If you don’t see the product you are looking for, or have specific questions, please contact us.
Other solutions
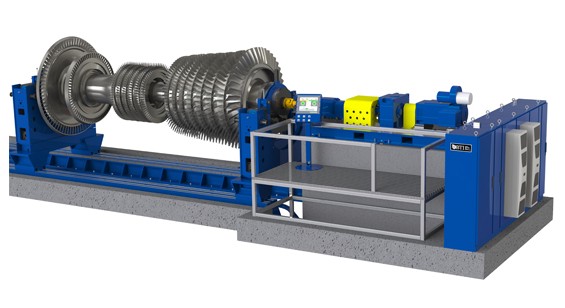
200,000 lb Capacity Horizontal Balancer for Steam and Gas Turbines
200,000 lb Capacity Horizontal Balancer for Steam and Gas Turbines
View More
30,000 RPM Automatic Spin Tester for Induction & Permanent Magnet Electric ...
30,000 rpm Automatic Spin Tester for Induction & Permanent Magnet Electric Vehicle Rotors.
View More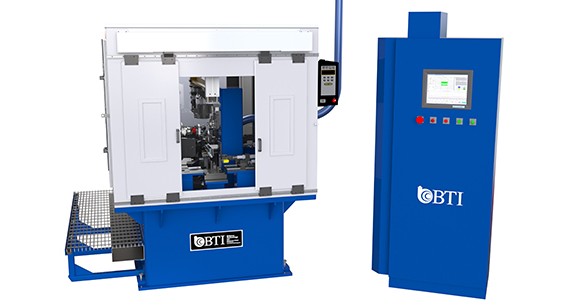
300,000 RPM Turbocharger Balancer, Wheel Milling
Fully-Automatic 300,000 rpm High Speed Turbo Charger Assembly Balancer with Automatic Compressor Wheel Milling & Drilling Correction. Featuring Servo Controlled Air Drive System, Oil...
View More
300,000 RPM Turbocharger Core Assembly 2 Plane Balancer
4,000 to 300,000 rpm Low and High Speed Turbo Charger Core Assembly 2 Plane Balancer with Touch Up Grinder, Featuring Pulsation Measurement & “G”...
View More
5-Station Armature Balancer with 2 Plane Contour
6-Second (600 part per hour) Fully Automatic 5-Station Armature Balancer with 2 Plane Contour or V-Cut Mill Correction
View More
5-Station Torque Convertor Assembly Balancer
Fully Automatic 5-Station Torque Convertor Assembly Balancer with Automatic Variable and Fixed Length Weight Making and Weld Correction, featuring Automatic Walking Beam Transfer, Oil...
View More
6-Station Armature Balancer w/ Axial Drill Correction
220 Part Per Hour Fully-Automatic 6-Station Armature Balancer Featuring Dual Axial Drill Correction, Walking-Beam Transfer, Overhead Belt Drive and Part Sorting
View More
Induction & Permanent Magnet Rotor Cell
Automated Induction & Permanent Magnet Electric Rotor Cell Featuring two 6-Station balancers, six 30,000 rpm Automatic Spin Testers and Four Robots
View More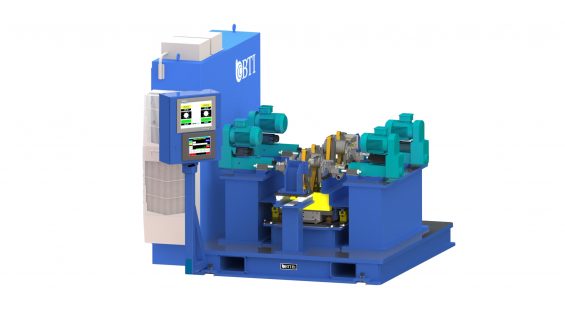
Automatic 2-Station Induction Balance Solution
Automatic 2-Station Induction & Permanent Magnet Electric Rotor Cell Featuring two Independent Balance Stations, Dual Drills on Each Station, Scissor […]
View More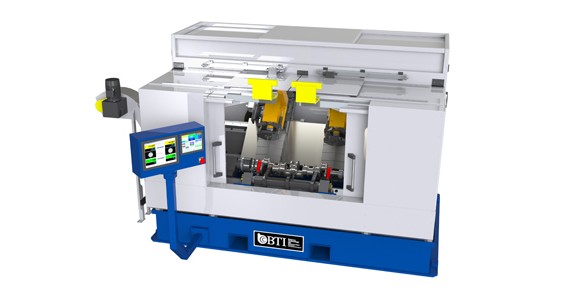
Automatic Crankshaft Balancer with Dual Servo MQL Drill Correction
Fully Automatic Crankshaft Balancer with Dual Servo MQL Drill Correction and Overhead Gantry Load Screen reader support enabled. Fully Automatic Crankshaft Balancer with Dual...
View More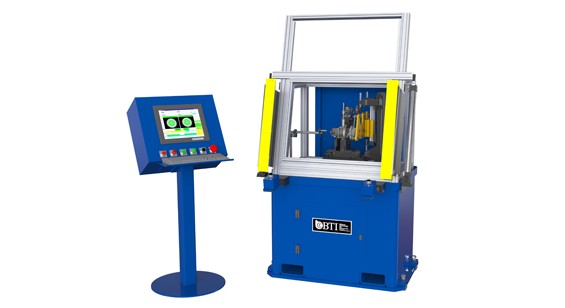
Low Speed Turbocharger CHRA Assembly Balancer
Automatic Low Speed Turbo Charger CHRA Core Assembly Balancer with Dual Drive Technology, Featuring both Belt and Servo Controlled Air Drive Systems as well...
View More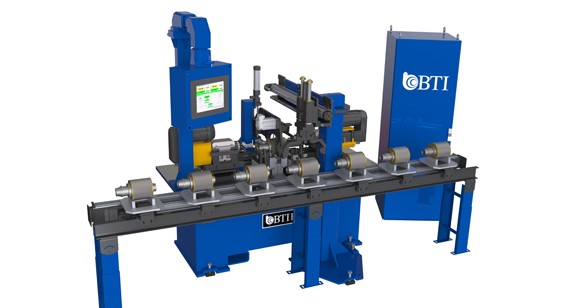
Automatic Permanent Magnet Rotor Balancer
Fully Automatic Permanent Magnet Rotor Balancer, featuring Automatic 2-Plane Axial Drill Correction, Pneumatic Pick and Place Transfer, and Palletized Part Conveyance
View More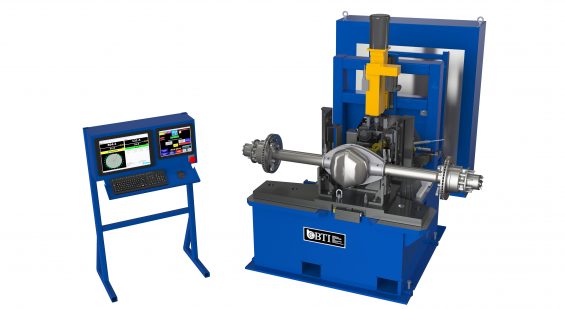
Automatic Rear Axle Balancer With Automatic Drill Correction
1000 lb Fully Automatic Rear Axle Balancer Featuring Automatic Drill Correction and Part Marking
View More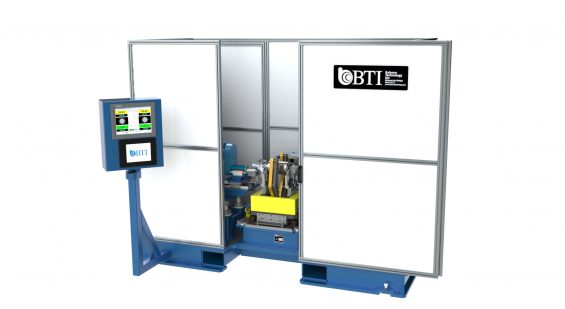
Automatic Single Station Induction & Permanent Magnet Electric Rotor Cell F...
Automatic Single Station Induction & Permanent Magnet Electric Rotor Cell Featuring Dual Drills and Scissor Belt Drive
View More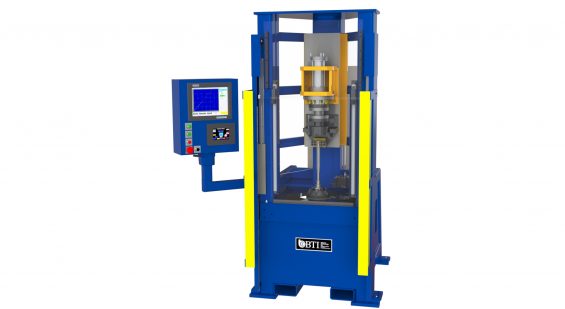
Automatic Torsional Test Stand for Steering Column Tulip Assemblies
Automatic Torsional Test Stand for Steering Column Tulip Assemblies.
View More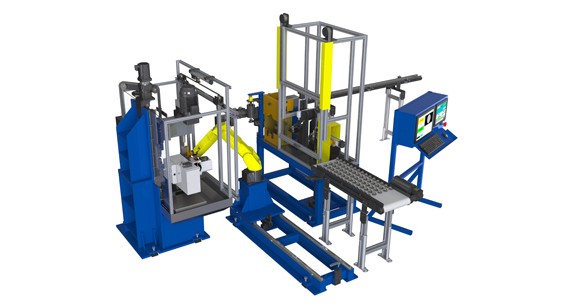
Automatic Turbocharger Compressor Wheel
Fully Automatic Turbo Charger Compressor Wheel Cell Featuring Automatic 2-Plane Mill Correction, Dimensional Gaging, Eddy Current Surface Defect Detection, 2D Laser Marking, Robotic Part...
View More
Balancer with Elevator Mill Correction Station
Single station Brake Rotor Balancer with Elevator Load/Unload and Onboard BTI Mill Correction Station. Featuring Dimensional Gaging of Key Attributes such as Flatness, Parallelism,...
View More
Bench-top Horizontal Balancer for Measuring Unbalance
Bench-top Horizontal Balancer for Measuring Unbalance of Computer Hard Drive Disc Reader Heads
View More
Brake Rotor Bore Gage with Temperature Compensation and Auto Feedback to Upstrea...
Brake Rotor Bore Gage with Temperature Compensation and Auto Feedback to Upstream Machining Operations
View More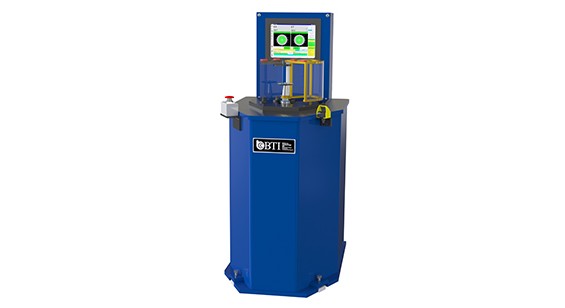
BTI’s Patented Spindle-Less CAT, BT & HSK Tool Holder Balancer
BTI’s Patented Spindle-Less CAT, BT & HSK Tool Holder Balancer
View More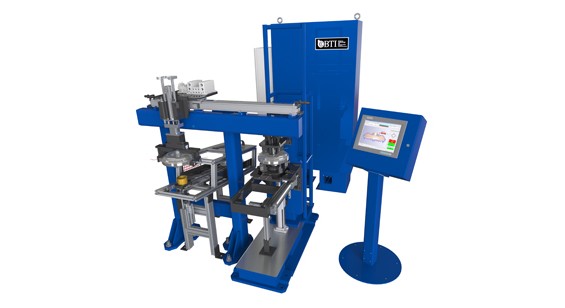
Combination Machine Featuring Dimensional Gaging
Fully-Automatic Combination Machine Featuring Dimensional Gaging and Surface Roughness Measurement of Torque Converter Assemblies
View More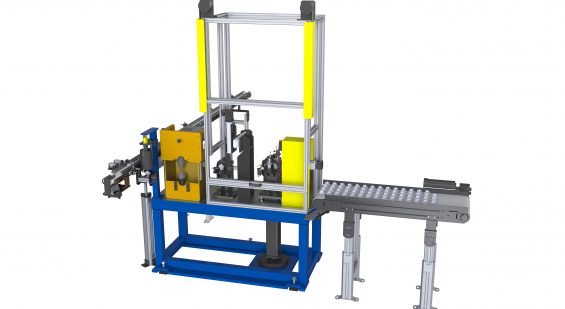
Compressor Wheel Cell Gaging & Surface Detection
Fully Automatic Turbo Charger Compressor Wheel Cell Featuring Dimensional Gaging, Eddy Current Surface Defect Detection, 2D Laser Marking and Conveyance
View More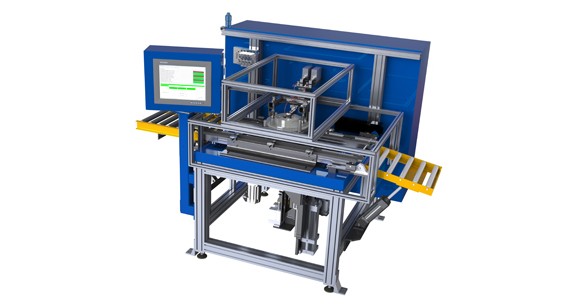
Crack Detection Brake Rotors System
Fully-Automatic Eddy Current Crack Detection System for Brake Rotors
View More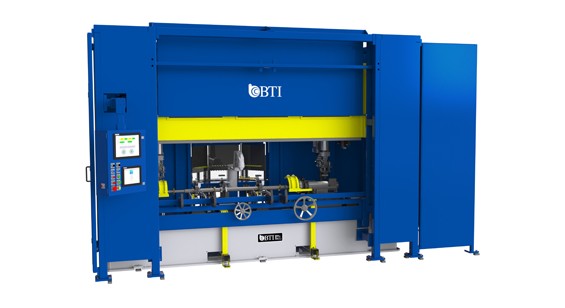
Driveshaft Balancer with Automatic Spot Weld Correction
Fully Automatic 1, 2, and 3 Piece Driveshaft Balancer with Automatic Spot Weld Correction via Magazine Feed Weights, featuring Auto Guard Doors, 5-Plane Balance...
View More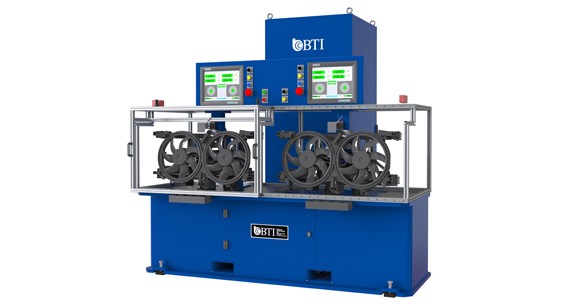
Dual Engine Fan Balancer
Two Station Dual Engine Cooling Fan Balancer Featuring Advanced Blade Counting, Speed and Direction Verification System and Electrical Motor & PWM Function Tests
View More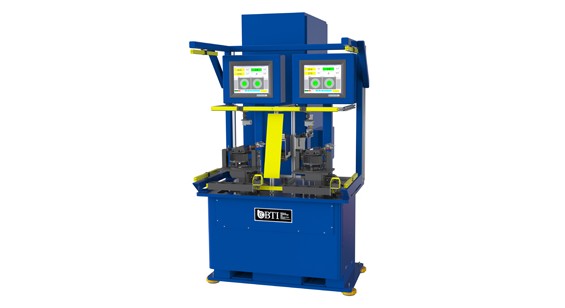
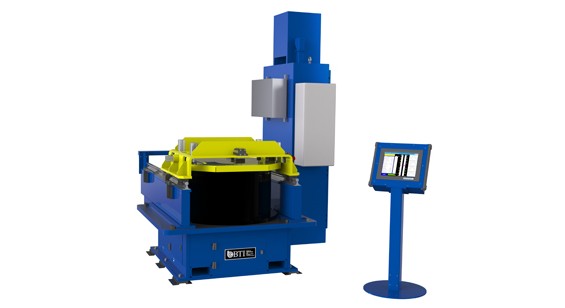
Durability Tester for Grinding Wheels
Semi-Automatic High Speed Durability Tester for Grinding Wheels
View More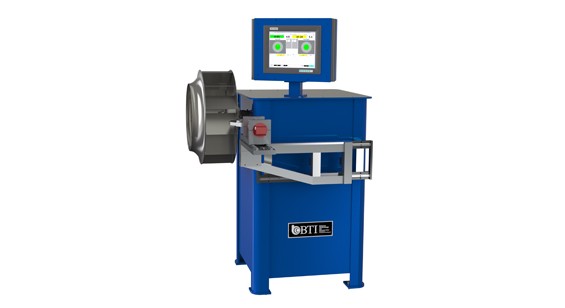
Dynamic Aluminum Fan Balancer with Automatic Rivet Correction
Dynamic Aluminum Fan Balancer with Automatic Rivet Correction
View More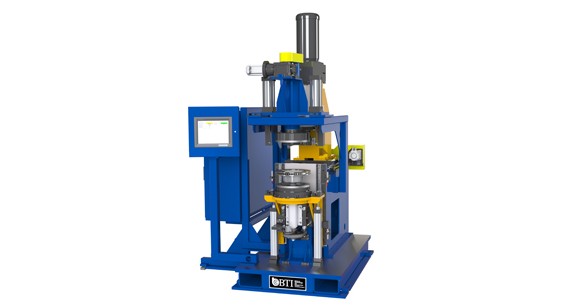
Dynamic Brake Rotor Balancer
Semi-Automatic Single Station Dynamic Brake Rotor Balancer with Automatic Mill Correction
View More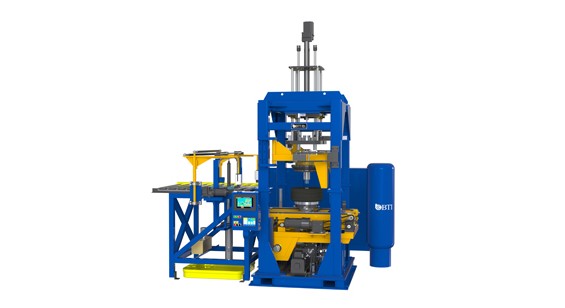
Dynamic Tire Inflator Balancer with Bead Lubrication
Fully Automatic Dynamic Tire Inflator Balancer with Bead Lubrication, Laser Gaging, and Ink Stamp Marking
View More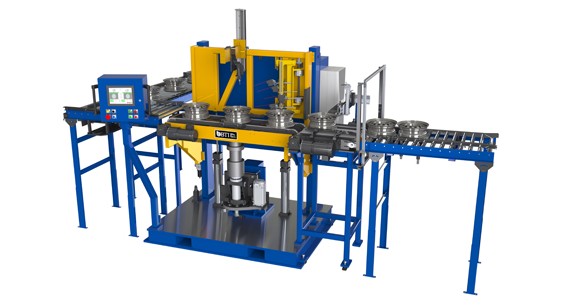
Dynamic Wheel Combination Machine
Fully Automatic Dynamic Wheel Combination Machine featuring Part Identification, Axial and Radial Laser Gaging, and Balance Audit with Orient and Mark
View More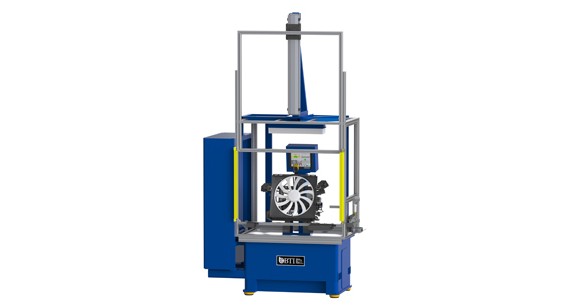
Engine Cooling Fan Module Balancer and Motor Tester
Engine Cooling Fan Module Balancer and Motor Tester
View More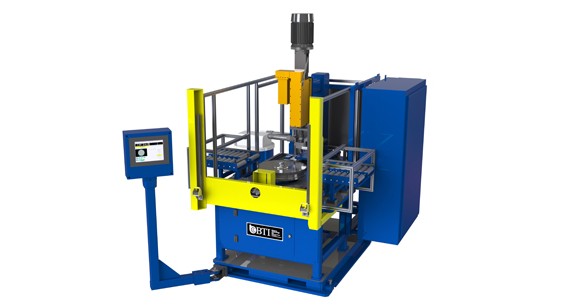
Flywheel Balancer with Automatic Drill Correction
Semi-Automatic Flywheel Balancer with Automatic Drill Correction, Ring Gear Sensor, and Load Assist Elevator
View More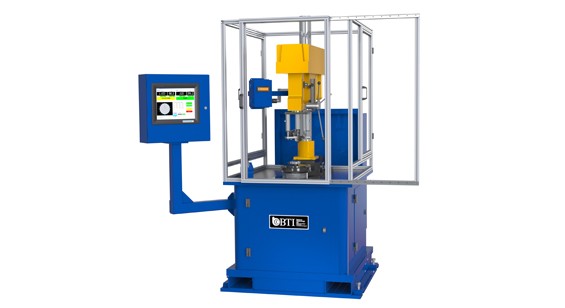
Flywheel Balancer with Manual Drill Correction
Flywheel Balancer with Manual Drill Correction Featuring Drill Depth Readout
View More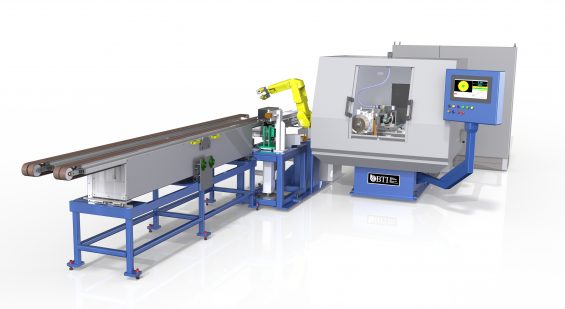
Shaft & Wheel Balancer, Laser Mapping & CBN Grinding
Full Automatic Shaft & Wheel Balancer with Laser Mapping, CBN Grinding, High Pressure Coolant, Ultra-Sonic Part Contact Sensor, Conveyance & Robot Load/Unload
View More
Fully Automatic 5-Station Armature Balancer with 2 Plane Contour
6-Second (600 part per hour) Fully Automatic 5-Station Armature Balancer with 2 Plane Contour or V-Cut Mill Correction
View More
Fully Automatic RDM Balancer and NVH Combination
Fully Automatic RDM Balancer and NVH Combination featuring Drill Correction, Laser Gaging, Drive Shaft Hung Mass Simulation, and Advanced Clutch Conditioning Technology
View More
Rear Axle Balancer with Automatic Drill Correction
Fully Automatic Rear Axle Balancer featuring Automatic Drill Correction, Part Marking, and RFID Traceability
View More
Fully Automatic Rear Drive Module Balancer
Fully Automatic Rear Drive Module Balancer Featuring Automatic Drill Correction, Part Marking, and RFID Traceability
View More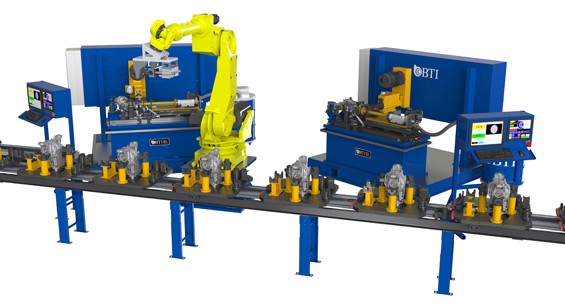
Fully Automatic Rear Drive Module Cell featuring Two Drill Correction Balancers
Fully Automatic Rear Drive Module Cell featuring Two Drill Correction Balancers, Robot with Dual End Effectors, Palletized Part Conveyance, Master Part Housing Stations, Part...
View More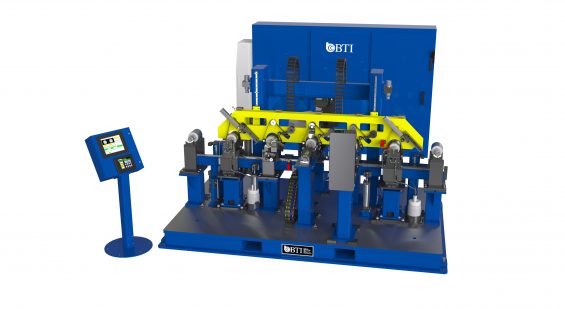
Fully Automatic Six Station Induction & Permanent Magnet Electric Motor Rot...
Fully Automatic Six Station Induction & permanent Magnet Electric Motor Rotor Balancer Featuring Overhead Belt Drive System, Two Drill Correction Stations, Chip Containment and...
View More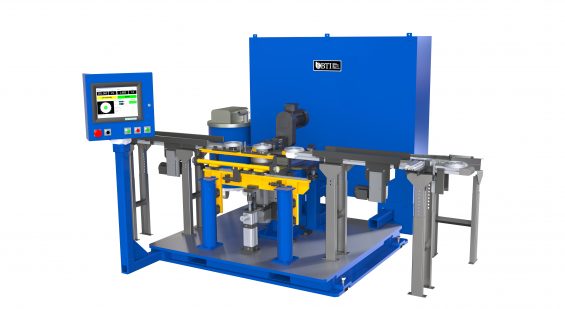
Fully Automatic Stator Balancer with Mill Correction and Walking-Beam Transfer
Fully Automatic Stator Balancer with Mill Correction and Walking-Beam Transfer
View More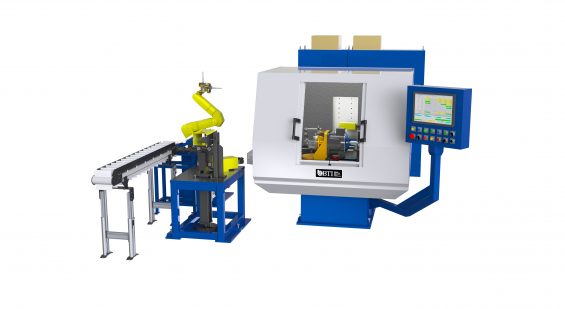
Fully Automatic Turbocharger Shaft & Wheel Cell
Fully Automatic Turbo Charger Shaft & Wheel Cell Featuring Automatic 2-Plane CBN Wet Grind Correction, Dimensional Gaging, Robotic Part Handling, and Conveyance
View More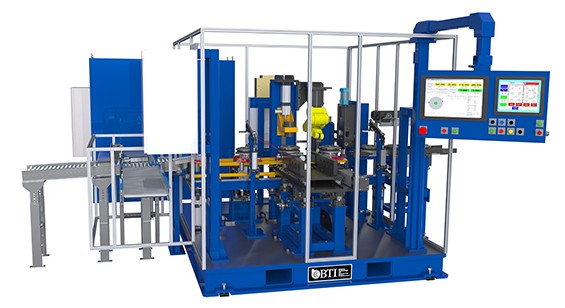
5-Station Turbine Damper Assembly Balancer
Fully-Automatic 5-Station Turbine Damper Assembly Balancer with Automatic Variable & Fixed Length Weight Making, Featuring Projection Weld Correction and Part Sorting
View More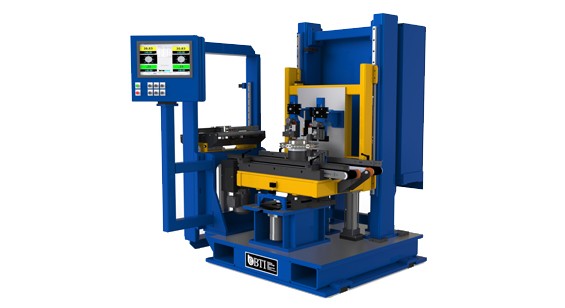
Fully-Automatic Brake Rotor Combination Bore & Multi-Attribute Gage
Fully-Automatic Brake Rotor Combination Bore & Multi-Attribute Gage Featuring Temperature Compensation and Auto Feedback to Upstream Machining Operations
View More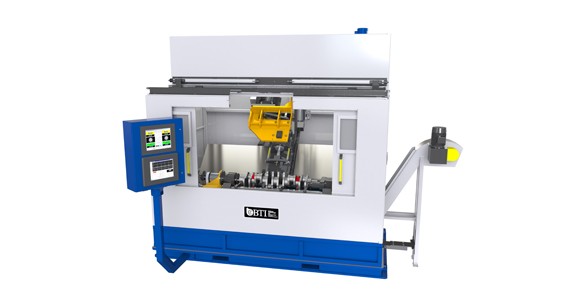
Crankshaft Balancer, Spindle Drill & Gantry Load
Fully-Automatic Crankshaft Balancer with High Pressure Coolant Through The Spindle Drill Correction and Overhead Gantry Load
View More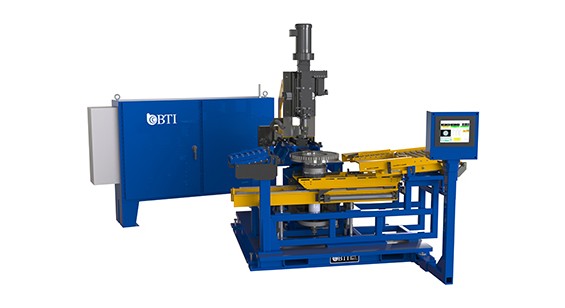
Fully-Automatic Heavy Duty Flywheel Balancer with Automatic Drill Correction and...
Fully-Automatic Heavy Duty Flywheel Balancer with Automatic Drill Correction and Load/Unload Assist Elevator
View More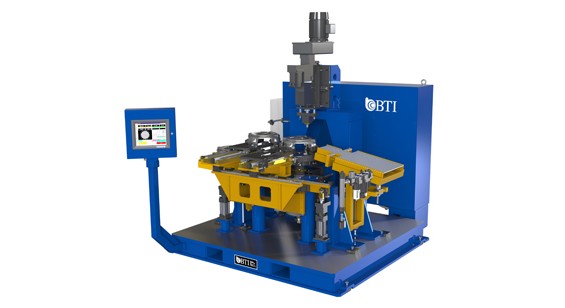
Fully-Automatic Large Clutch Housing Balancer with Automatic Drill Correction
Fully-Automatic Large Clutch Housing Balancer with Automatic Drill Correction
View More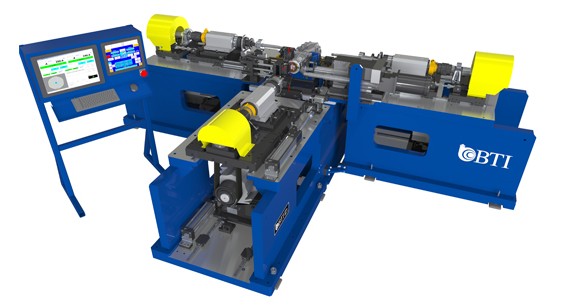
RDM Balancer & NVH Combination w/ Drill Correction
Fully-Automatic RDM Balancer & NVH Combination. Featuring Drill Correction, Laser Gaging, Drive Shaft Hung Mass Simulation and Advanced Clutch Conditioning Technology
View More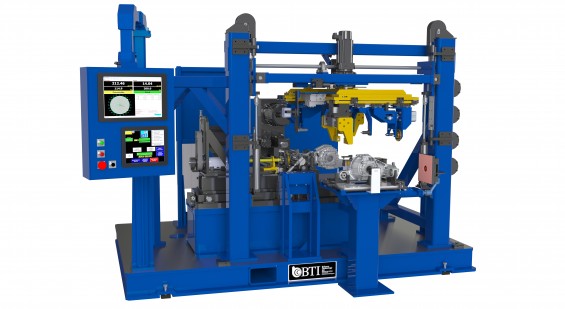
Fully-Automatic RDM Balancer Featuring Automatic Mill or Drill Correction
Fully-Automatic RDM Balancer Featuring Automatic Mill or Drill Correction, 180 Degree Rotary Load/Unload Station, Vision System to Detect Part Orientation, Part ID Scanner &...
View More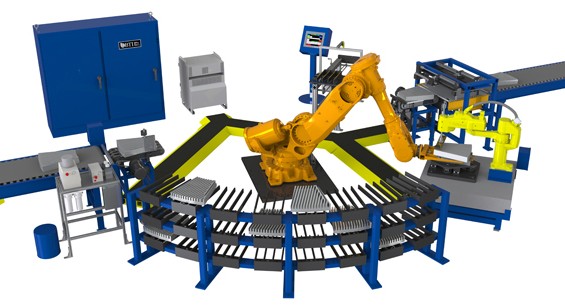
Fully-Automatic Refiner Plate Cell
Fully-Automatic Refiner Plate Cell Featuring Gaging and C.G. Measurement of Individual Plates for Predictive Balance Optimization when Assembled Per the Cell’s Advanced Sequencing and...
View More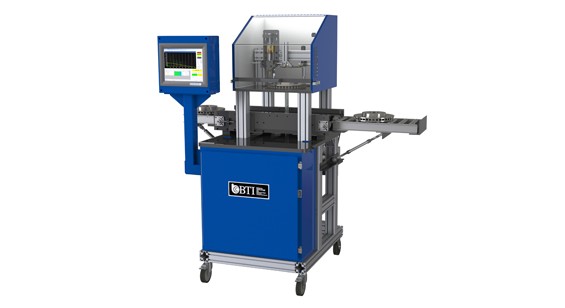
Fully-Automatic Resonant Frequency Measurement Station
Fully-Automatic Resonant Frequency Measurement Station
View More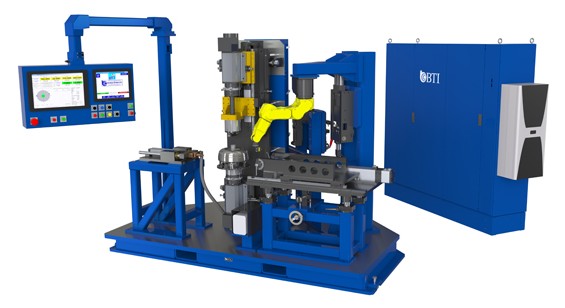
Single Station Torque Convertor Balancer
Fully-Automatic Single Station Torque Convertor Assembly Balancer with Automatic Variable and Fixed Length Weight Making and Weld Correction. Featuring Dual Motorized Spindles for Low...
View More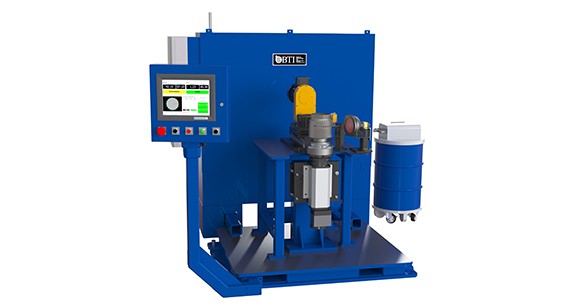
Transmission Clutch Housing Balancer, Drill Correction
Fully-Automatic Transmission Clutch Housing Balancer with Automatic Radial Drill Correction and Chip Containment System
View More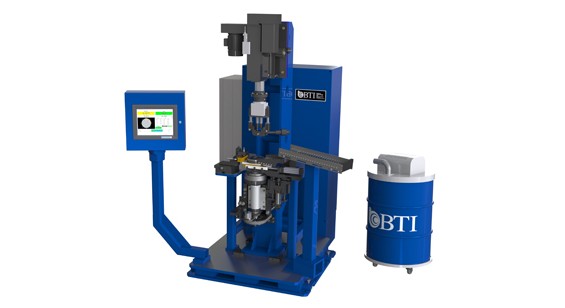
Harmonic Vibration Damper Balancer
Semi-Automatic Harmonic Vibration Damper Balancer with Automatic Servo Drill Correction, Featuring V-groove Dimensional Gaging, Auto Unload and Chip Containment
View More
High Speed Assembly Balancer for Automotive Industry
Automatic High Speed Turbo Charger CHRA Core Assembly Balancer with Touch Up Grinder, Oil Pumping with Flow & Temperature Monitoring […]
View More
High Speed Turbocharger Core Assembly 2 Plane Balancer
300,000 rpm High Speed Turbo Charger Core Assembly 2 Plane Balancer with Automatic Mill and Drill Correction, Featuring Pulsation Measurement, “G” Measurement, RPM sweep,...
View More
Horizontal Healthcare Fan / Blower Assembly Balancer
Horizontal Healthcare Fan / Blower Assembly Balancer with Programable Power Supply and Quick Connect Wire Harness.
View More
Horizontal Speedometer/Tachometer Needle Balancer
Horizontal Speedometer/Tachometer Needle Balancer
View More
HVAC Fan Module Balancer and Motor Testing
Dual Station HVAC Fan Module Balancer Featuring Blade Counting, Motor Testing and Segmented Weight Correction
View More
Impeller Balancer with Automatic Mill correction and Laser Gaging of Axial Run-O...
Impeller Balancer with Automatic Mill correction and Laser Gaging of Axial Run-Out
View More
Low- and High-Speed Turbocharger Core Assembly 2 Plane Balancer
4,000 to 300,000 rpm Low- and High-Speed Turbo Charger Core Assembly 2 Plane Balancer with Touch-Up Grinder, featuring Pulsation Measurement, “G” Measurement, and Oil...
View More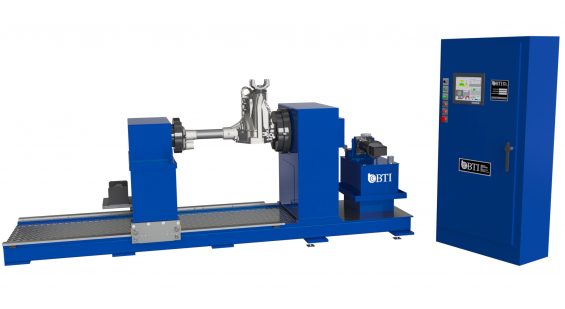
Manual Torsional Test Stand for Front Axle Assemblies
Manual Torsional Test Stand for Front Axle Assemblies.
View More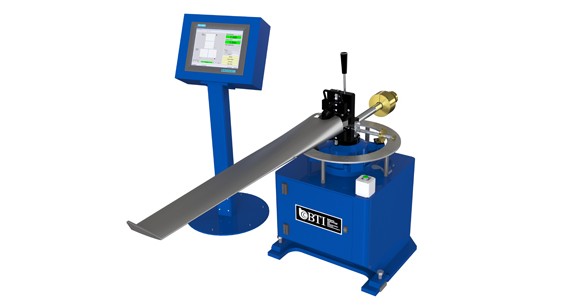
Moment Balancer for Helicopter Blades and Propellers
Moment Balancer for Helicopter Blades and Propellers
View More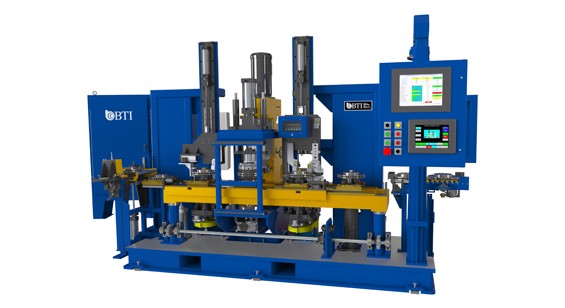
Multi-Station Combination Brake Rotor Machine
Fully Automatic Multi-Station Combination Brake Rotor Machine featuring Balancing with Mill Correction, Dimensional Gaging, Surface Finish Measurement, Eddy Current Crack Detection, and Part Marking
View More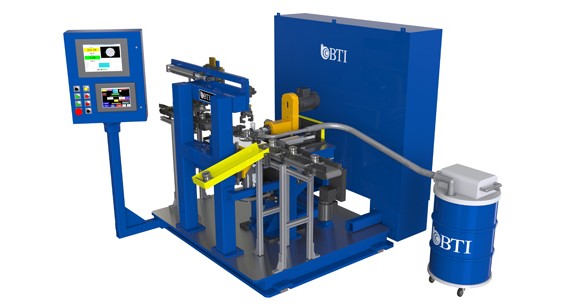
Multi-Station Flange Balancer with Correction Mill
Multi-Station Flange Balancer with Correction Mill
View More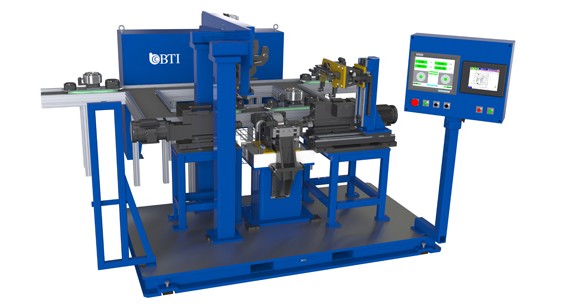
Multi-Station Magnetized Electric Armature Balancer
Fully Automatic Multi-Station Magnetized Electric Armature Balancer featuring Palletized Part Conveyance, Dual-Axial Drill Correction, and Heavy Spot Ink Marking
View More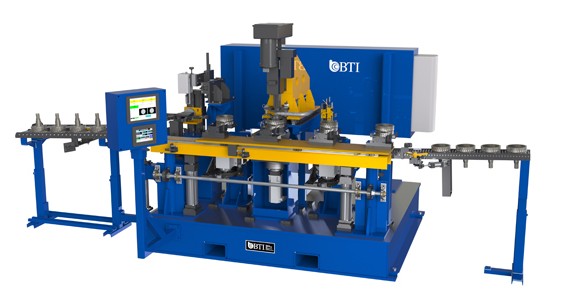
Multi-Station Transmission Carrier Combination Machine
Fully Automatic Multi-Station Transmission Carrier Combination Machine featuring Dimensional Gaging, Balancing with Automatic Drill Correction, Part Orientation Flipper, and Pin Stamp Marker
View More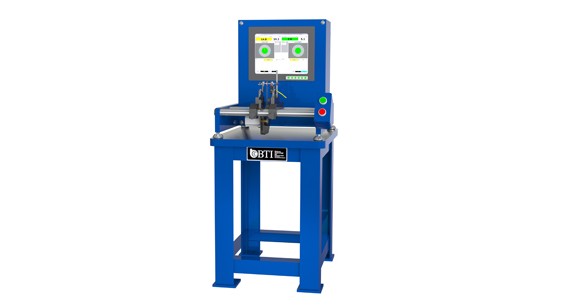
PC Cooling Fan Module Assembly Balancer with Motor Testing
PC Cooling Fan Module Assembly Balancer with Motor Testing
View More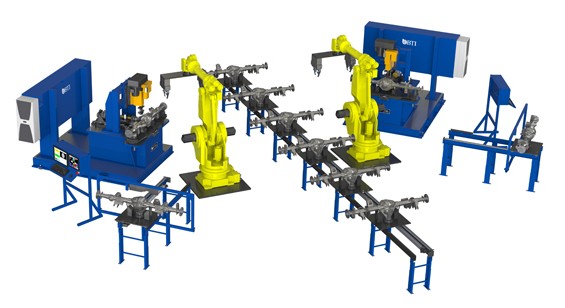
Rear Axle Cell featuring Two Drill Correction Balancers
Fully Automatic Rear Axle Cell featuring Two Drill Correction Balancers, Two Robots, Palletized Part Conveyance, Master Part Housing Stations, Part Marking, and RFID Traceability
View More
Replacement PC’s & PLC’s for all Brands and Models
Replacement PC’s & PLC’s for all Brands and Models
View More
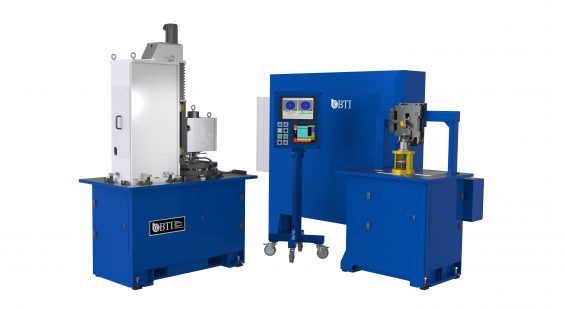
Semi Automatic Two Station Turbine Wheel Mass Center and Audit Machine
Semi Automatic Two Station Turbine Wheel Mass Center and Audit Machine
View More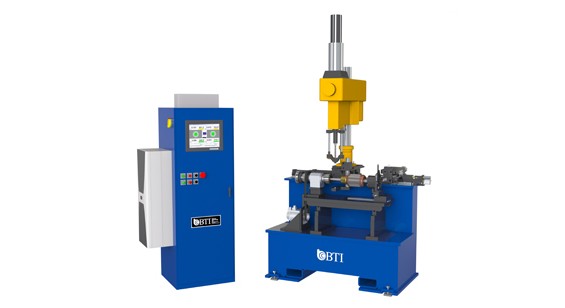
Semi-Automatic Armature Balancer, Drill Correction
Semi-Automatic Armature Balancer with Automatic Drill Correction and Automatic Servo-Controlled Commutator Lathe
View More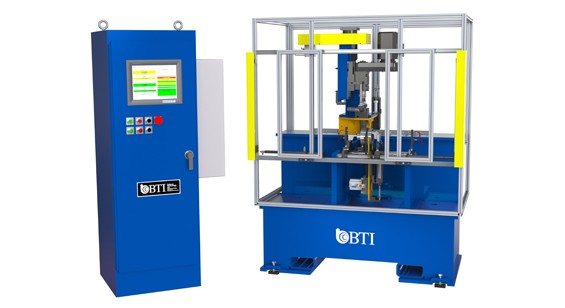
Semi-Automatic Clutch Housing Balancer with Automatic Drill Correction and Chip ...
Semi-Automatic Clutch Housing Balancer with Automatic Drill Correction and Chip Containment
View More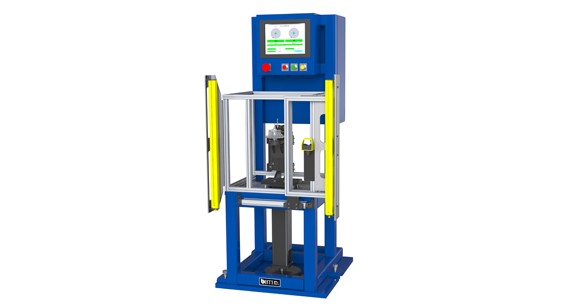
Semi-Automatic Compressor Wheel Air Bearing Audit Station
Semi-Automatic Compressor Wheel Air Bearing Audit Station Featuring Servo Controlled Whisper Drive Technology
View More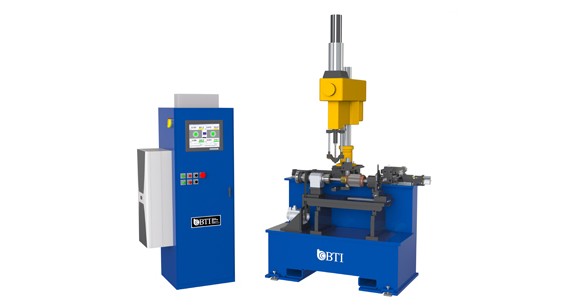
Semi-Automatic Crankshaft Balancer, Hook End Drive
Semi-Automatic Crankshaft Balancer Featuring Hook End Drive, Automatic Drill Correction, Paint Marker and Chip Containment System
View More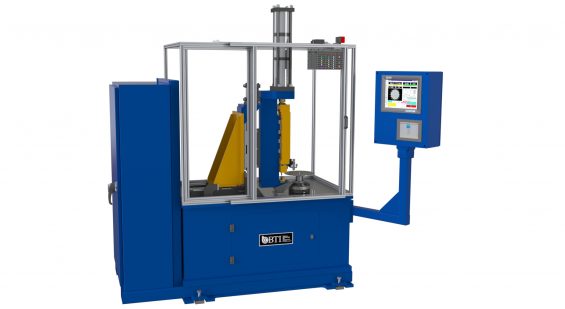
Semi-Automatic Drive Plate Balancer with Punch Correction and Slug Containment
Semi-Automatic Drive Plate Balancer with Punch Correction and Slug Containment.
View More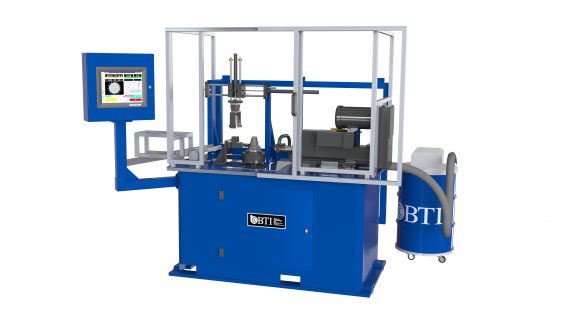
Semi-Automatic Flange Balancer with Mill Correction and Auto-Unload
Semi-Automatic Flange Balancer with Mill Correction and Auto-Unload.
View More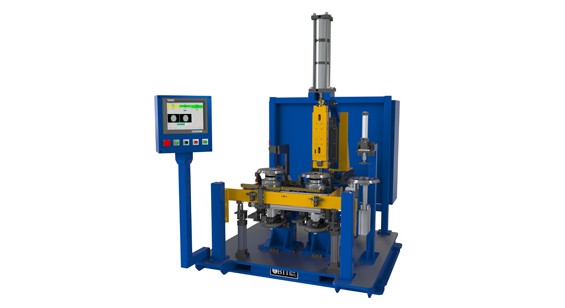
Semi-Automatic Flywheel Balancer
Semi-Automatic Flywheel Balancer with Automatic Pierce Correction, Slug Collection System, Pin Stamp Marking, Radial & Axial Dimensional Gaging
View More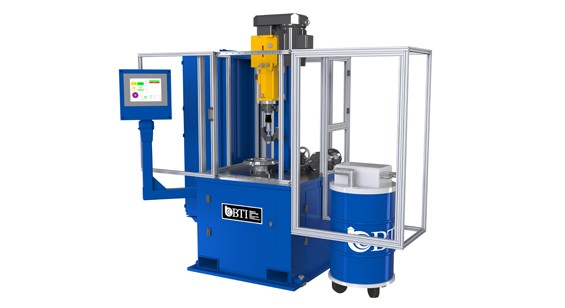
Semi-Automatic Flywheel Balancer with Automatic Drill Correction
Semi-Automatic Flywheel Balancer with Automatic Drill Correction
View More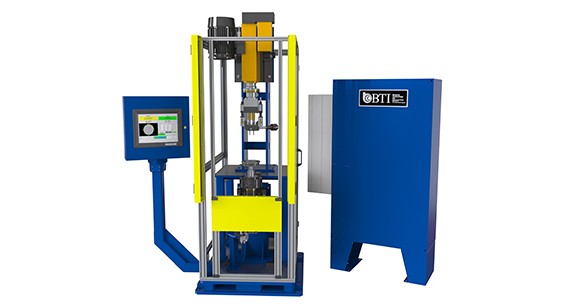
Semi-Automatic Harmonic Damper Balancer with Automatic Dual Drill Correction
Semi-Automatic Harmonic Damper Balancer with Automatic Dual Drill Correction and Vacuum Chip Removal
View More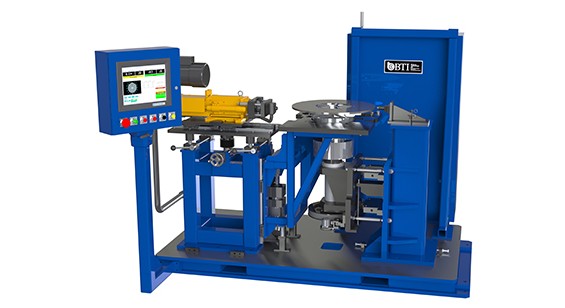
Semi-Automatic Heavy Duty Unvented Brake Rotor Balancer
Semi-Automatic Heavy Duty Unvented Brake Rotor Balancer with Automatic Radial Drill Correction and Load/Unload Assist Elevator
View More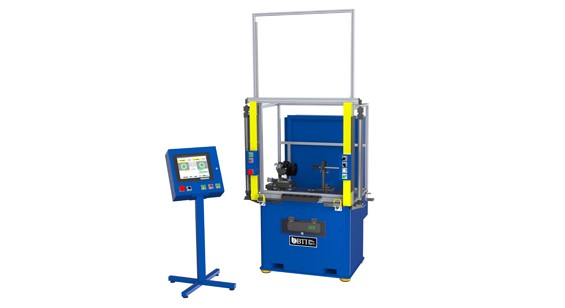
Semi-Automatic HVAC Fan Module Balancer
Semi-Automatic HVAC Fan Module Balancer Featuring Quick Disconnect Tooling for Multiple Part Models, Blade Counting, Motor Testing and Segmented Weight Correction
View More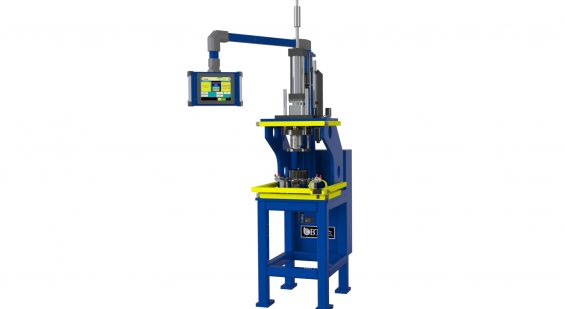
Semi-Automatic HVAC Fan Wheel / Motor Press Station
Semi-Automatic HVAC Fan Wheel / Motor Press Station. Capable of Pressing to both a Force and a Distance.
View More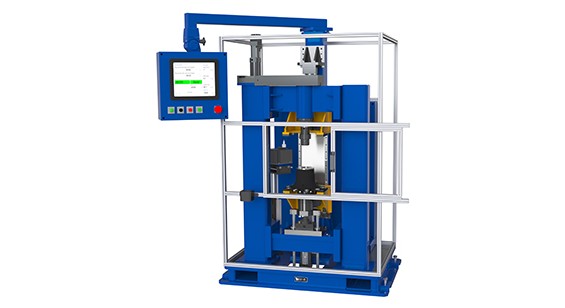
Semi-Automatic Rear Brake Hub Dynamic Axial Endplay and Bore Gage
Semi-Automatic Rear Brake Hub Dynamic Axial Endplay and Bore Gage
View More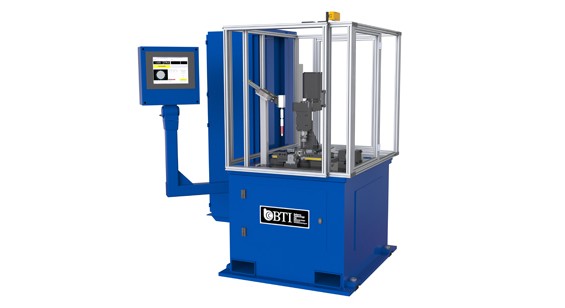
Semi-Automatic Reaction Carrier Balancer with Automatic Mill Correction and Part...
Semi-Automatic Reaction Carrier Balancer with Automatic Mill Correction and Part Marking
View More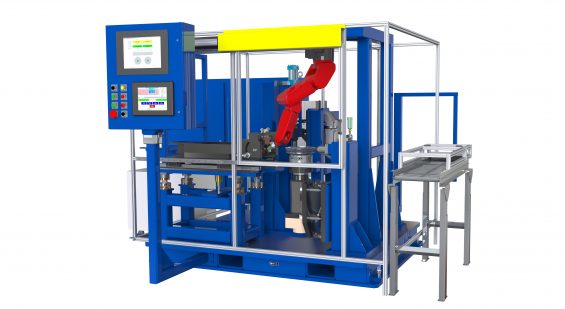
Semi-Auto Single Station Torsional Damper Balancer
Semi-Automatic Single Station Dynamic Torsional Damper Balancer with Automatic Projection Weld Correction
View More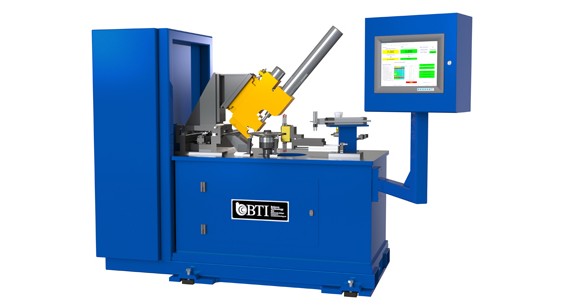
Semi-Automatic Torsional Damper Combination Machine
Semi-Automatic Torsional Damper Combination Machine Featuring Balancing with Automatic Pierce Correction, Dimensional Gaging, Part Marking, Rivet and Disallowed Area Sensing
View More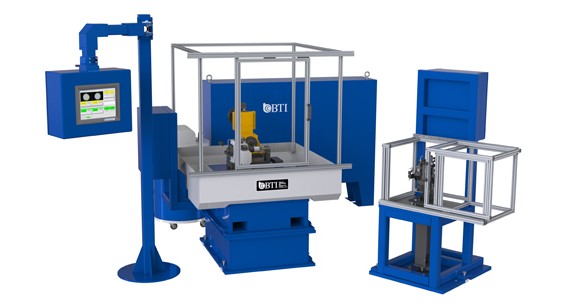
Semi-Automatic Turbocharger Compressor Wheel Balance
Semi-Automatic Turbo Charger Compressor Wheel Balance Cell Featuring Air-Bearing Measurement Technology and Automatic Mill Correction
View More
Semi-Automatic X-Ray Target Balancer
Semi-Automatic X-Ray Target Balancer with Automatic Servo Drill Correction Featuring Automatic Drill Changeover to Accommodate a Wide Varity of Parts without Operator Intervention
View More
Semi-Automatic Yoke Assembly Balancer
Semi-Automatic Yoke Assembly Balancer with Drill Correction and Chip Containment
View More
Snowmobile Clutch Balancer
Semi-Automatic Snowmobile Clutch Balancer with Automatic Axial & Radial Drill Correction
View More
Static Aircraft Tire Balancer with Load Assist Elevator
Static Aircraft Tire Balancer with Load Assist Elevator
View More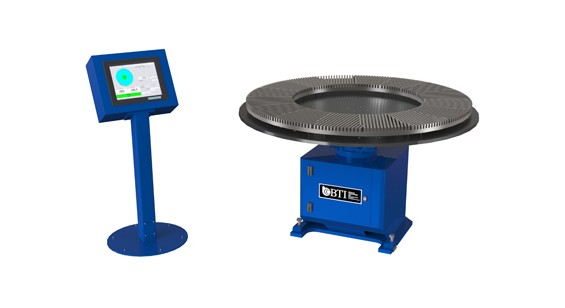
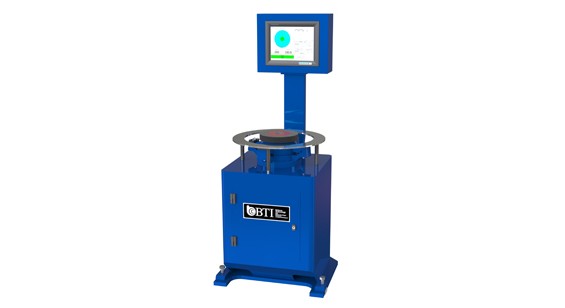
Static Grinding Wheel Audit Station with Pneumatic Tooling
Static Grinding Wheel Audit Station with Pneumatic Tooling
View More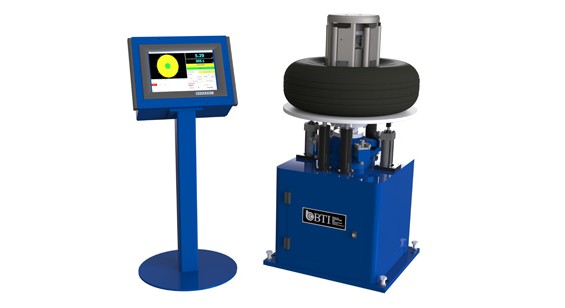
Static Tire Balancer with Pneumatic Paddle Style Tooling and Load Assist Elevato...
Static Tire Balancer with Pneumatic Paddle Style Tooling and Load Assist Elevator
View More
Torque Convertor Measure Station
Torque Convertor Measure Station Featuring Dual Motorized Spindles with Multiple Measurement Techniques (Static Internal, 180 Flip and Differential Measurement)
View More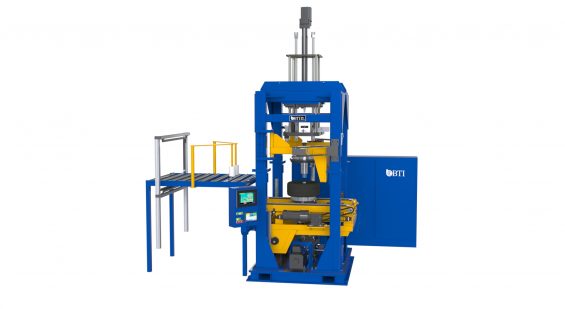
Truck Tire Inflator Balancer
Large Dynamic Truck Tire Inflator Balancer Featuring Radial & Lateral Laser Runout, Bead Lubrication, Load/Unload Elevator & Hot Stamp Unbalance Marking System.
View More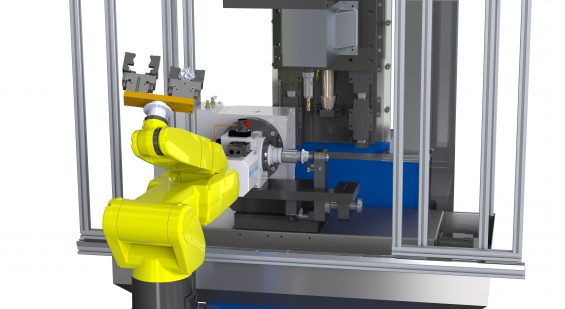
Turbocharger Compressor Wheel Balancer
Fully Automatic Turbo Charger Compressor Wheel Balancer with 2-Plane BTI Mill Correction Station Featuring Robotic Part handling
View MoreGet Started
Get in touch with us. We're here to assist you.
Connect with our measurement experts and get the technical guidance your application demands.