Manual, Semi-Automatic & Automatic Balancing Machines | BTI
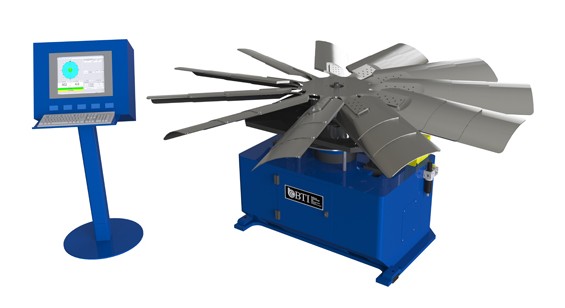
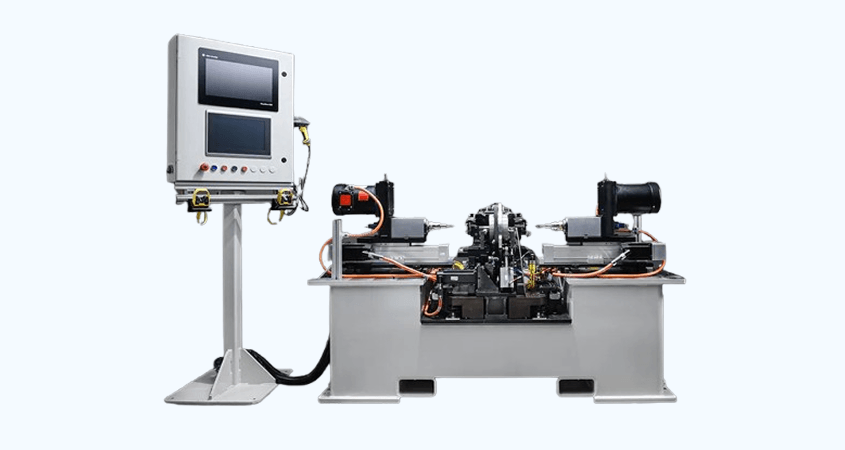
BTI engineers and manufactures a complete line of manual, semi-automatic, and fully automatic industrial balancing machines, all part types, production rates, and levels of automation. From static to dynamic, single-plane to multi-plane, hard-bearing to soft-bearing, and single-station to multi-station, BTI does it all.
- Horizontal Cradles
- Vertical Rotators
- Vertical Non-Rotators
- Overhung
- Platform Suspensions
- Air-Bearing Systems
What a Balancing Machine Does
A balancing machine measures the unbalance in a rotating part and tells you how much mass to add or remove, and where, to bring it inside tolerance. Unbalance exists when a rotor’s mass is not distributed symmetrically about its rotational axis. Spin that rotor and the offset mass produces a centrifugal force that rises with the square of rotational speed — double the speed and the force quadruples. That force is what shortens bearing life, loosens fasteners, fatigues mountings and produces the noise and vibration an operator feels. Balancing is the process of measuring it and correcting it, and a balancing machine is the instrument that makes the measurement repeatable enough to act on. BTI has been building these machines in Whitmore Lake, Michigan since 1968, for automotive, aerospace, power generation, defense and a dozen other industries.Static and Dynamic Balancing
The distinction is about correction planes, and it follows from the shape of the part. Static balancing corrects in a single plane. It suits parts that are large in diameter relative to their length — a disc, a flywheel, a fan wheel, a brake rotor, a grinding wheel. For these, one correction plane is enough because the unbalance acts essentially in one plane already. Dynamic balancing corrects in two or more planes. Any part with meaningful length along its axis — a crankshaft, a driveshaft, a motor rotor, a turbine assembly — can carry unbalance that produces a couple as well as a force. Correcting that requires measurement and correction in two planes, which is what a dynamic balancing machine does. If a part is longer than roughly its own diameter, assume dynamic. The ISO balance tolerance calculator takes the number of correction planes as an input for exactly this reason.Hard-Bearing and Soft-Bearing Machines
Both measure unbalance. They differ in where the machine runs relative to the resonant frequency of its own suspension.| Type | How it works | Where it fits |
|---|---|---|
| Hard-bearing | Runs below the suspension’s resonant frequency. Measurement is derived from force, so the machine is calibrated permanently and holds calibration across parts. | Mixed part families, job shops, MRO, low-to-moderate volume with frequent changeover |
| Soft-bearing | Runs above resonance. Measurement is derived from displacement, so the machine is calibrated per part setup using a known test mass. | Dedicated production of one part family, and very low residual tolerances |
Machine Platforms
The platform follows the part geometry and how the part has to be held. The correction method follows the material and where there is room to add or remove mass.| Platform | How the part is held | Typical components |
|---|---|---|
| Horizontal cradle (H) | Shaft-type parts supported at their journals | Crankshafts, driveshafts, armatures, rotor assemblies |
| Vertical rotator (VR) | Parts held and driven about a vertical axis | Torque converters, turbochargers, pump rotors, wheels |
| Vertical non-rotator (VNR) | Disc-shaped parts measured without full rotation | Brake rotors and drums, flywheels, clutches, fan wheels |
| Platform suspension (P) | Assemblies carried on a suspended platform | Cooling modules, complete assemblies, irregular parts |
Levels of Automation
| Level | What it does | Where it fits |
|---|---|---|
| Manual | Operator loads, runs and corrects. Lowest cost, widest part range. | MRO, remanufacturing, job shops, low volume |
| Semi-automatic | Machine measures and positions; operator loads and performs correction. | Moderate volume, several part families |
| Fully automatic | Load, measure, correct and unload without operator intervention, integrated into the line. | Production programs at takt time |
Balance Tolerance and ISO 21940-11
Balance tolerances are set by ISO 21940-11, which superseded ISO 1940-1. The standard assigns a balance quality grade G by component type, and the permissible residual specific unbalance follows from that grade and the service speed: eper = (G × 60) ÷ (2π × n) where eper is permissible residual specific unbalance in g·mm/kg, G is the balance quality grade in mm/s, and n is the service speed in rev/min. Permissible residual unbalance is then U = eper × m, divided across the correction planes.| Grade | Typical components |
|---|---|
| G 630 | Crankshaft drives of large slow marine diesel engines |
| G 250 | Crankshaft drives of rigidly mounted fast four-cylinder diesel engines |
| G 100 | Crankshaft drives of fast diesel engines with six or more cylinders |
| G 40 | Car wheels, wheel rims and wheel sets |
| G 16 | Driveshafts and cardan shafts with special requirements |
| G 6.3 | Fans, flywheels, pump impellers, normal electric armatures |
| G 2.5 | Gas turbine rotors, turbochargers, machine-tool drives |
| G 1 | Precision spindles and small high-speed rotors |
| G 0.4 | Precision grinder spindles — the tightest grade in the standard |
Correction Methods
| Method | Where it fits |
|---|---|
| Drill | Cast and forged parts with material available to remove |
| Mill | Controlled removal on a defined correction band, suited to volume |
| Grind | Hardened or finished surfaces, including turbine and spindle hardware |
| Weld-on weight | Driveshafts, torque converters and fabricated assemblies |
| Clip-on or press-on weight | Wheel and tire assemblies |
| Adhesive and applied weight | Plastics, coated parts and finished assemblies |
How a Machine Gets Specified
Sizing works from the tooling and the part together, not the part alone. Tooling is not specified until the part prints are reviewed and the fixture is concepted, and the heavier the tooling-plus-part assembly is relative to the class, the less repeatable the measurement becomes. To quote a balancing machine, BTI needs the part print, the part weight, the service speed, the balance tolerance if one is specified, and the required production rate. Lead times are quoted in weeks at the time of quotation and move with current backlog. Tell BTI the part weight and BTI will name a class the same day.Rebuilds, Retrofits and Upgrades
A balancing machine that is not performing does not always need replacing. Where the mechanical base is sound, the measurement system and controls can be replaced for a fraction of the cost of a new machine. BTI does this for its own equipment and for machines built by other manufacturers. See BTI rebuilds and retrofits, competitor rebuilds and retrofits, and PC upgrades.Frequently Asked Questions
What is the difference between static and dynamic balancing?
Static balancing corrects in one plane and suits disc-shaped parts. Dynamic balancing corrects in two or more planes and is required for any part with meaningful length along its axis, because such parts can carry a couple as well as a force. As a rule of thumb, a part longer than its own diameter needs dynamic balancing.Should I buy a hard-bearing or soft-bearing machine?
Hard-bearing for a mixed part range, because it holds calibration across changeovers. Soft-bearing for dedicated production of one part family, or where the residual tolerance is tight enough that measurement resolution becomes the limiting factor.How do I know what balance tolerance my part needs?
ISO 21940-11 assigns a balance quality grade by component type and derives the tolerance from service speed and rotor mass. If the part print does not specify one, BTI works it out from the part and the duty.Can one balancing machine handle more than one part?
Yes, within a class. How wide that range can be depends on the tooling and on how much repeatability the application requires. MRO and remanufacturing shops routinely run a broad part range on a single machine.Does BTI service balancing machines made by other manufacturers?
Yes. Where the mechanical base is sound, BTI rebuilds and retrofits competitor equipment as well as its own.What information does BTI need to quote a balancing machine?
The part print, the part weight, the service speed, the balance tolerance if specified, and the required production rate. See balancing machines by industry or request a quote.Precision Measurement & Testing Equipment
In addition to static and dynamic balancing equipment, BTI also engineers and manufactures other types of industrial precision measurement and testing equipment, including dimensional gages, mass centering equipment, eddy current crack detection systems, surface finish measurement equipment, nvh equipment (noise vibration and harshness), functional test stands, spinners, motor testers, and resonant frequency measurement systems.
Specialized Test Systems
We also engineer and manufacture specialized test systems, including torque-to-turn, backlash, end play, and destructive test equipment.
Benefits of a Fully Integrated System
Additionally, BTI’s unique ability to combine the aforementioned technologies into one fully integrated system enables our clients to reduce capital expenditures, increase product quality, and minimize floor space requirements. There is no need for costly conveyors and escapements to connect independent machines together; nor do you need to train operators on multiple machines. There is one seamless, easy-to-use operator interface with unprecedented networking, statistical, and diagnostic capability.
Custom-Engineered Solutions
Whether you need a fully integrated, combined technology system (e.g., a balancer/gage/NVH combo) or independent machines, let our team of mechanical, electrical, and software engineers design and build a custom system for you.
If you don’t see the product you are looking for, or have specific questions, please contact us.
Other solutions
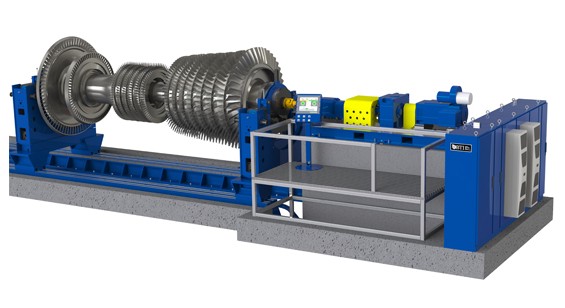
200,000 lb Capacity Horizontal Balancer for Steam and Gas Turbines
200,000 lb Capacity Horizontal Balancer for Steam and Gas Turbines
View More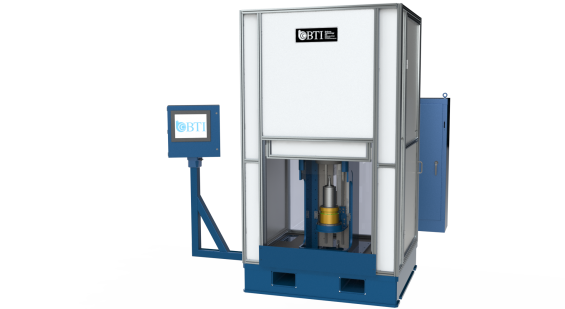
30,000 rpm Automatic Spin Tester for Induction & Permanent Magnet Electric ...
30,000 rpm Automatic Spin Tester for Induction & Permanent Magnet Electric Vehicle Rotors.
View More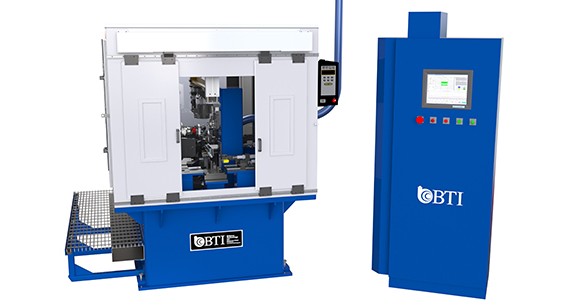
300,000 RPM Turbo Charger Balancer, Wheel Milling
Fully-Automatic 300,000 rpm High Speed Turbo Charger Assembly Balancer with Automatic Compressor Wheel Milling & Drilling Correction. Featuring Servo Controlled Air Drive System, Oil...
View More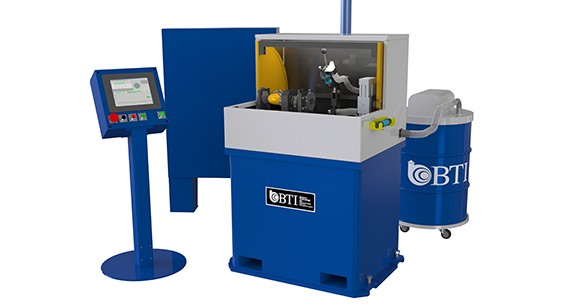
300,000 rpm Turbo Charger Core Assembly 2 Plane Balancer
4,000 to 300,000 rpm Low and High Speed Turbo Charger Core Assembly 2 Plane Balancer with Touch Up Grinder, Featuring Pulsation Measurement & “G”...
View More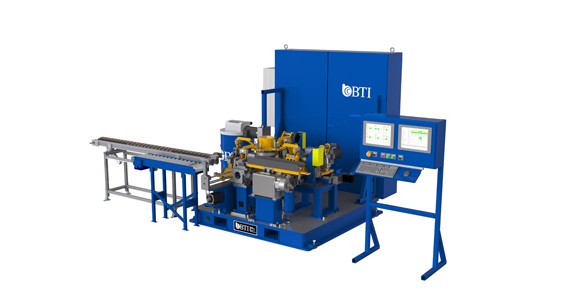
5-Station Armature Balancer with 2 Plane Contour
6-Second (600 part per hour) Fully Automatic 5-Station Armature Balancer with 2 Plane Contour or V-Cut Mill Correction
View More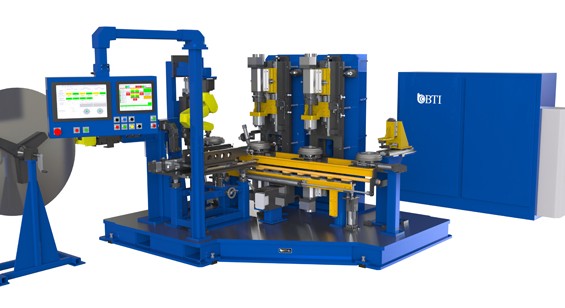
5-Station Torque Convertor Assembly Balancer
Fully Automatic 5-Station Torque Convertor Assembly Balancer with Automatic Variable and Fixed Length Weight Making and Weld Correction, featuring Automatic Walking Beam Transfer, Oil...
View More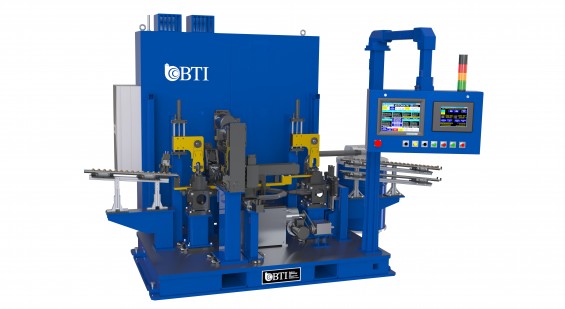
6-Station Armature Balancer w/ Axial Drill Correction
220 Part Per Hour Fully-Automatic 6-Station Armature Balancer Featuring Dual Axial Drill Correction, Walking-Beam Transfer, Overhead Belt Drive and Part Sorting
View More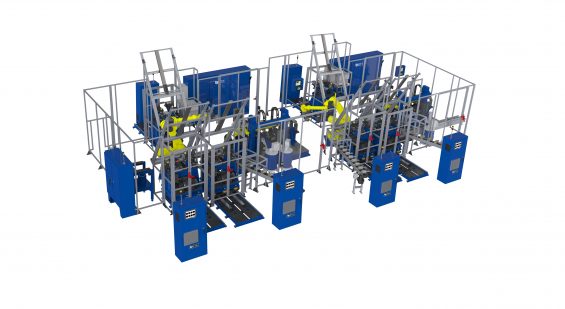
Induction & Permanent Magnet Rotor Cell
Automated Induction & Permanent Magnet Electric Rotor Cell Featuring two 6-Station balancers, six 30,000 rpm Automatic Spin Testers and Four Robots
View More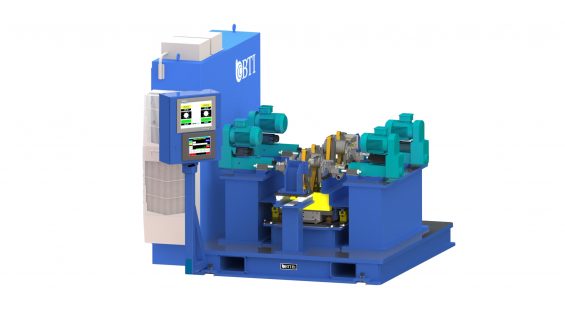
Automatic 2-Station Induction Balance Solution
Automatic 2-Station Induction & Permanent Magnet Electric Rotor Cell Featuring two Independent Balance Stations, Dual Drills on Each Station, Scissor […]
View More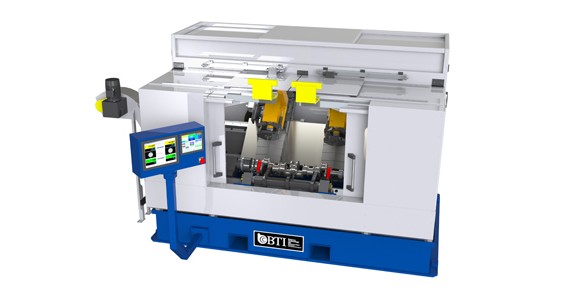
Automatic Crankshaft Balancer with Dual Servo MQL Drill Correction
Fully Automatic Crankshaft Balancer with Dual Servo MQL Drill Correction and Overhead Gantry Load Screen reader support enabled. Fully Automatic Crankshaft Balancer with Dual...
View More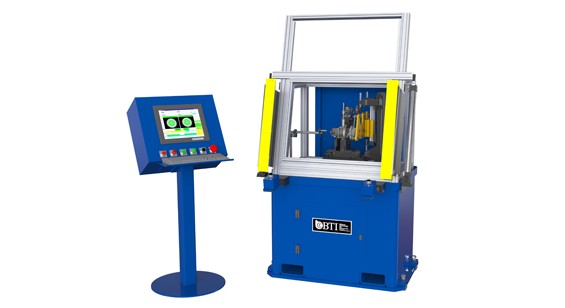
Low Speed Turbo Charger CHRA Assembly Balancer
Automatic Low Speed Turbo Charger CHRA Core Assembly Balancer with Dual Drive Technology, Featuring both Belt and Servo Controlled Air Drive Systems as well...
View More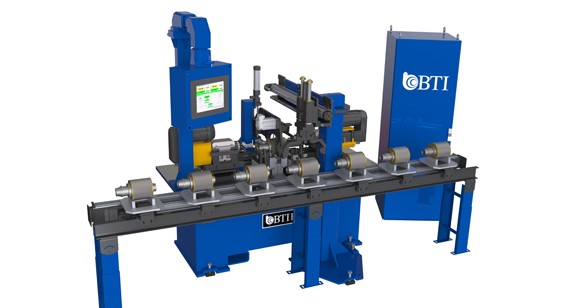
Automatic Permanent Magnet Rotor Balancer
Fully Automatic Permanent Magnet Rotor Balancer, featuring Automatic 2-Plane Axial Drill Correction, Pneumatic Pick and Place Transfer, and Palletized Part Conveyance
View More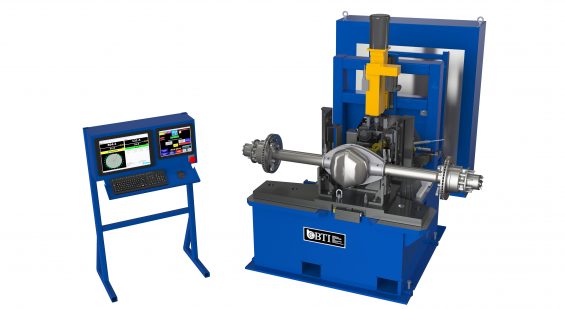
Automatic Rear Axle Balancer With Automatic Drill Correction
1000 lb Fully Automatic Rear Axle Balancer Featuring Automatic Drill Correction and Part Marking
View More
Automatic Single Station Induction & Permanent Magnet Electric Rotor Cell F...
Automatic Single Station Induction & Permanent Magnet Electric Rotor Cell Featuring Dual Drills and Scissor Belt Drive
View More
Automatic Torsional Test Stand for Steering Column Tulip Assemblies.
Automatic Torsional Test Stand for Steering Column Tulip Assemblies.
View More
Automatic Turbo Charger Compressor Wheel
Fully Automatic Turbo Charger Compressor Wheel Cell Featuring Automatic 2-Plane Mill Correction, Dimensional Gaging, Eddy Current Surface Defect Detection, 2D Laser Marking, Robotic Part...
View More
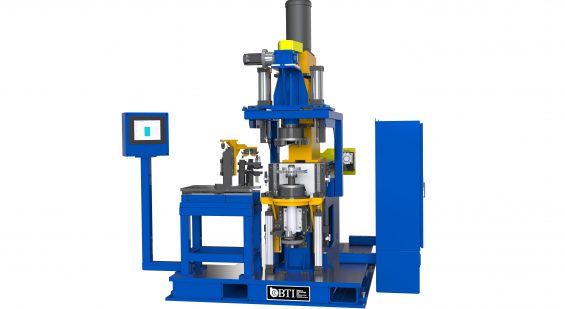
Balancer with Elevator Mill Correction Station
Single station Brake Rotor Balancer with Elevator Load/Unload and Onboard BTI Mill Correction Station. Featuring Dimensional Gaging of Key Attributes such as Flatness, Parallelism,...
View More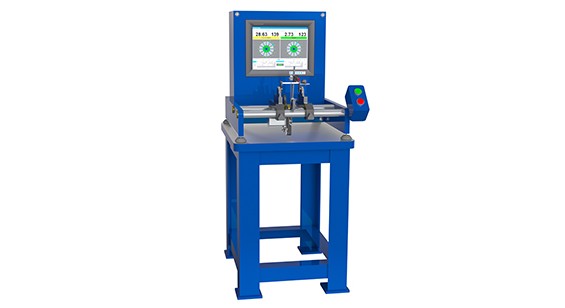
Bench-top Horizontal Balancer for Measuring Unbalance
Bench-top Horizontal Balancer for Measuring Unbalance of Computer Hard Drive Disc Reader Heads
View More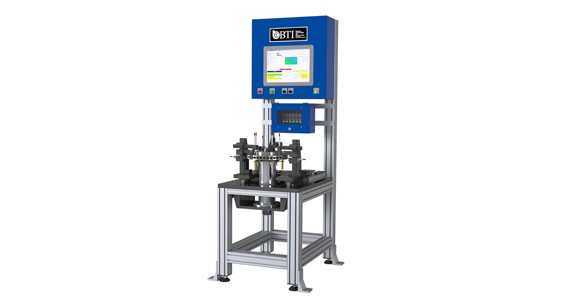
Brake Rotor Bore Gage with Temperature Compensation and Auto Feedback to Upstrea...
Brake Rotor Bore Gage with Temperature Compensation and Auto Feedback to Upstream Machining Operations
View More
BTI’s Patented Spindle-Less CAT, BT & HSK Tool Holder Balancer
BTI’s Patented Spindle-Less CAT, BT & HSK Tool Holder Balancer
View More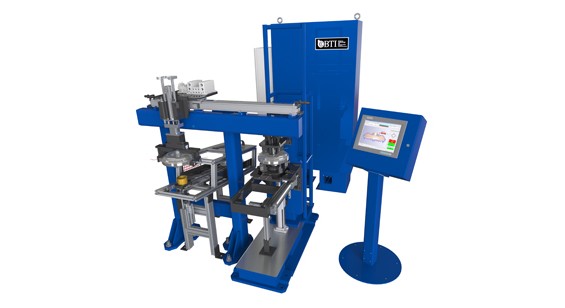
Combination Machine Featuring Dimensional Gaging
Fully-Automatic Combination Machine Featuring Dimensional Gaging and Surface Roughness Measurement of Torque Converter Assemblies
View More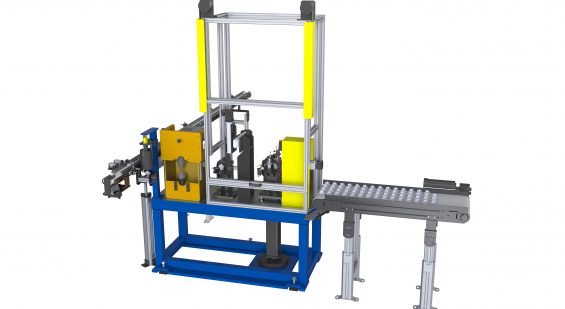
Compressor Wheel Cell Gaging & Surface Detection
Fully Automatic Turbo Charger Compressor Wheel Cell Featuring Dimensional Gaging, Eddy Current Surface Defect Detection, 2D Laser Marking and Conveyance
View More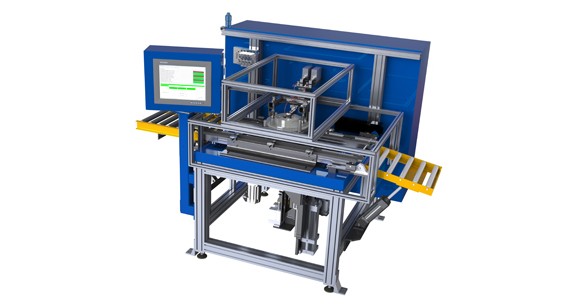
Crack Detection Brake Rotors System
Fully-Automatic Eddy Current Crack Detection System for Brake Rotors
View More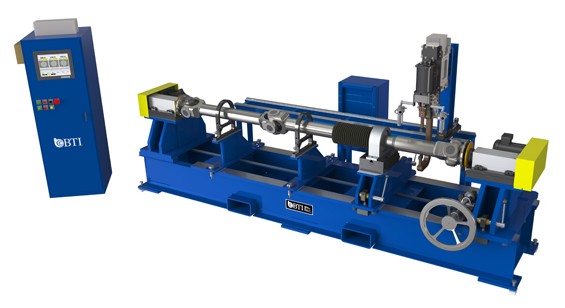
Driveshaft Balancer with Dual Servo Drives
1 or 2 Piece Driveshaft Balancer with Resistance Weld Correction Featuring Excessive Vibration Shutoff and Dual Servo Drives for Joint Loading and Maintenance
View More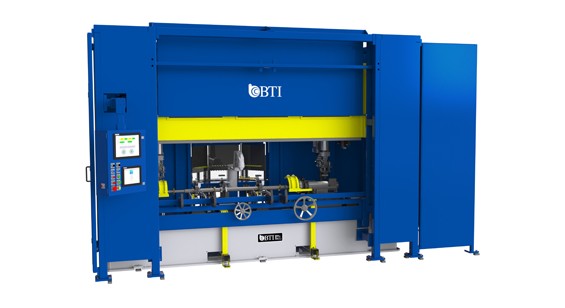
Driveshaft Balancer with Automatic Spot Weld Correction
Fully Automatic 1, 2, and 3 Piece Driveshaft Balancer with Automatic Spot Weld Correction via Magazine Feed Weights, featuring Auto Guard Doors, 5-Plane Balance...
View More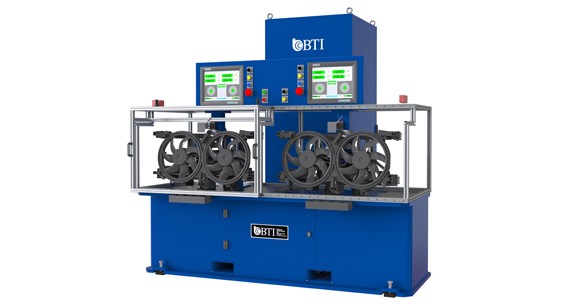
Dual Engine Fan Balancer
Two Station Dual Engine Cooling Fan Balancer Featuring Advanced Blade Counting, Speed and Direction Verification System and Electrical Motor & PWM Function Tests
View More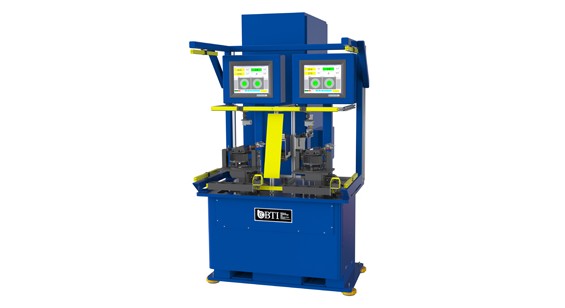
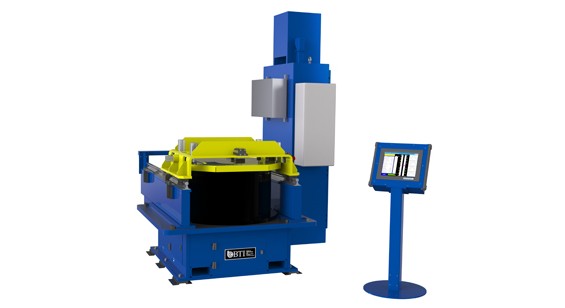
Durability Tester for Grinding Wheels
Semi-Automatic High Speed Durability Tester for Grinding Wheels
View More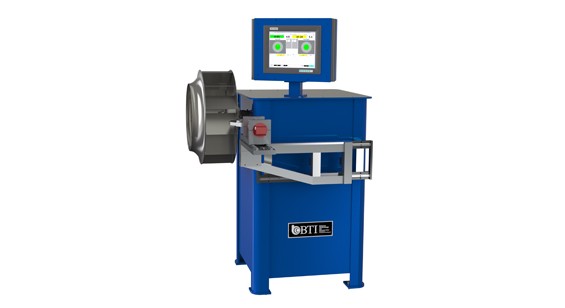
Dynamic Aluminum Fan Balancer with Automatic Rivet Correction
Dynamic Aluminum Fan Balancer with Automatic Rivet Correction
View More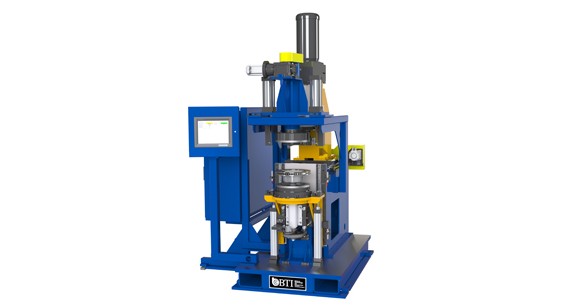
Dynamic Brake Rotor Balancer
Semi-Automatic Single Station Dynamic Brake Rotor Balancer with Automatic Mill Correction
View More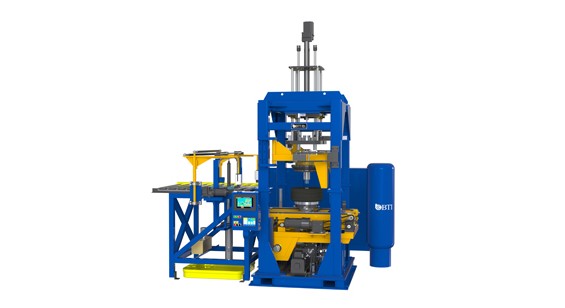
Dynamic Tire Inflator Balancer with Bead Lubrication
Fully Automatic Dynamic Tire Inflator Balancer with Bead Lubrication, Laser Gaging, and Ink Stamp Marking
View More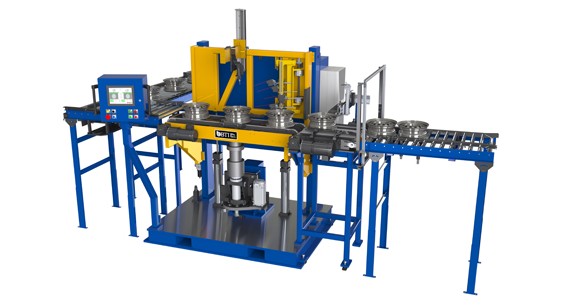
Dynamic Wheel Combination Machine
Fully Automatic Dynamic Wheel Combination Machine featuring Part Identification, Axial and Radial Laser Gaging, and Balance Audit with Orient and Mark
View More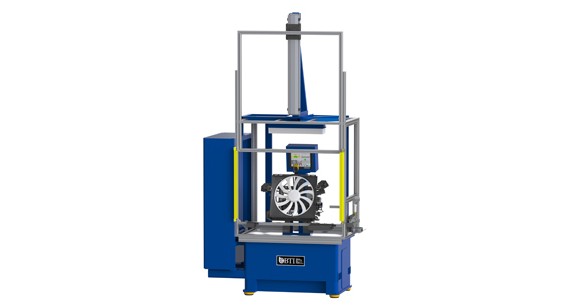
Engine Cooling Fan Module Balancer and Motor Tester
Engine Cooling Fan Module Balancer and Motor Tester
View More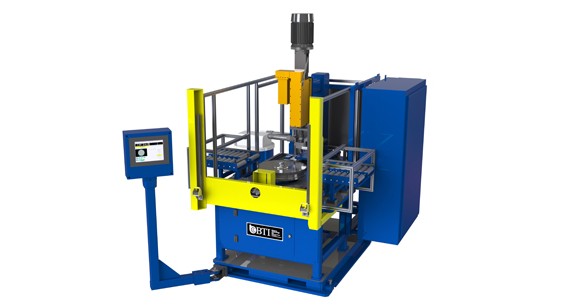
Flywheel Balancer with Automatic Drill Correction
Semi-Automatic Flywheel Balancer with Automatic Drill Correction, Ring Gear Sensor, and Load Assist Elevator
View More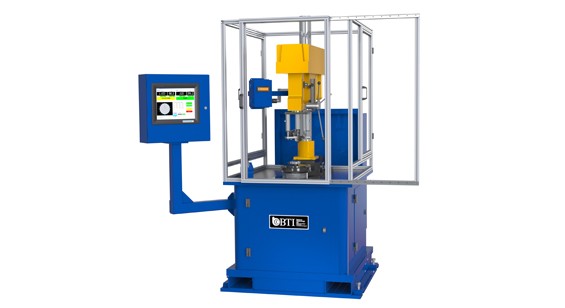
Flywheel Balancer with Manual Drill Correction
Flywheel Balancer with Manual Drill Correction Featuring Drill Depth Readout
View More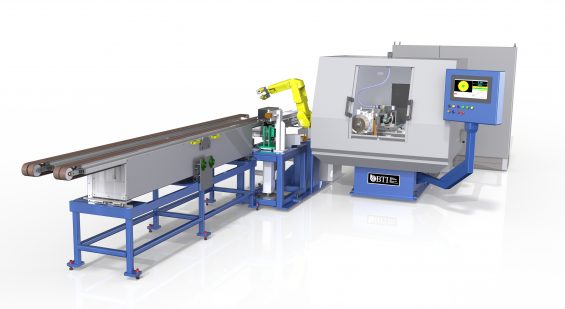
Shaft & Wheel Balancer, Laser Mapping & CBN Grinding
Full Automatic Shaft & Wheel Balancer with Laser Mapping, CBN Grinding, High Pressure Coolant, Ultra-Sonic Part Contact Sensor, Conveyance & Robot Load/Unload
View More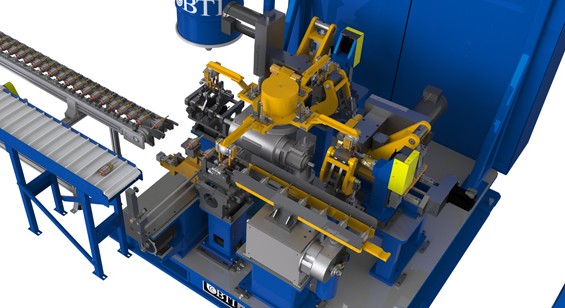
Fully Automatic 5-Station Armature Balancer with 2 Plane Contour
6-Second (600 part per hour) Fully Automatic 5-Station Armature Balancer with 2 Plane Contour or V-Cut Mill Correction
View More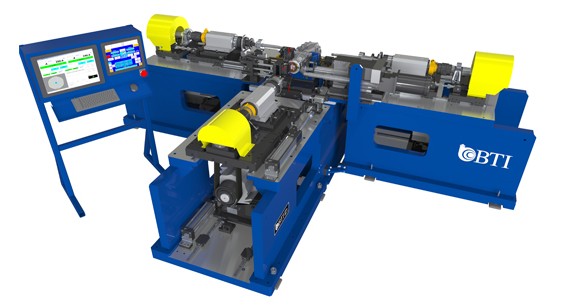
Fully Automatic RDM Balancer and NVH Combination
Fully Automatic RDM Balancer and NVH Combination featuring Drill Correction, Laser Gaging, Drive Shaft Hung Mass Simulation, and Advanced Clutch Conditioning Technology
View More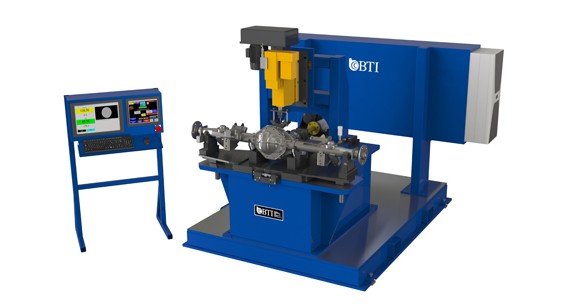
Rear Axle Balancer with Automatic Drill Correction
Fully Automatic Rear Axle Balancer featuring Automatic Drill Correction, Part Marking, and RFID Traceability
View More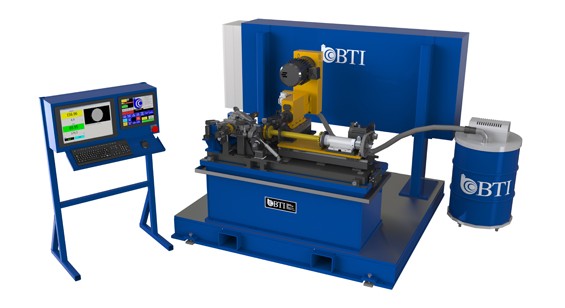
Fully Automatic Rear Drive Module Balancer
Fully Automatic Rear Drive Module Balancer Featuring Automatic Drill Correction, Part Marking, and RFID Traceability
View More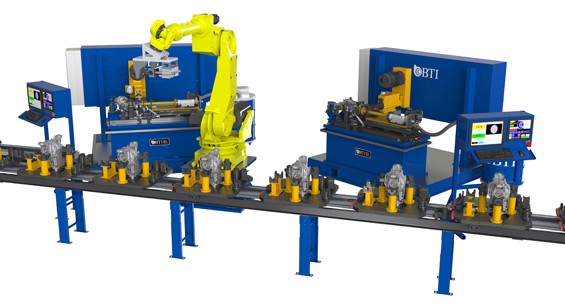
Fully Automatic Rear Drive Module Cell featuring Two Drill Correction Balancers
Fully Automatic Rear Drive Module Cell featuring Two Drill Correction Balancers, Robot with Dual End Effectors, Palletized Part Conveyance, Master Part Housing Stations, Part...
View More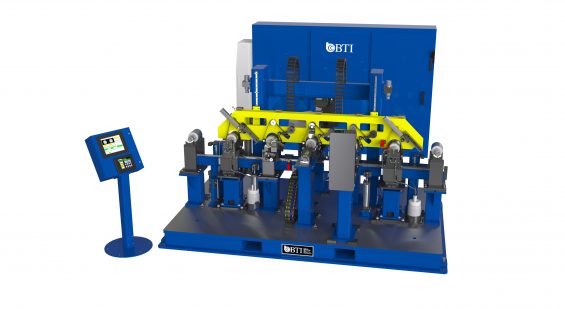
Fully Automatic Six Station Induction & Permanent Magnet Electric Motor Ro...
Fully Automatic Six Station Induction & permanent Magnet Electric Motor Rotor Balancer Featuring Overhead Belt Drive System, Two Drill Correction Stations, Chip Containment and...
View More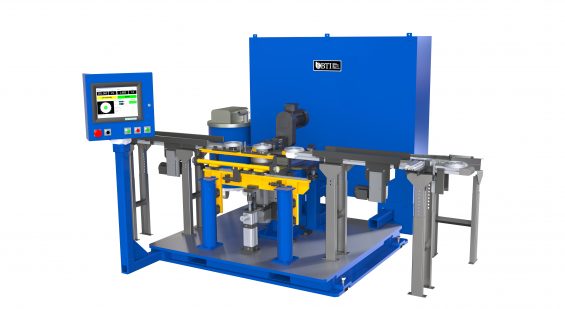
Fully Automatic Stator Balancer with Mill Correction and Walking-Beam Transfer
Fully Automatic Stator Balancer with Mill Correction and Walking-Beam Transfer
View More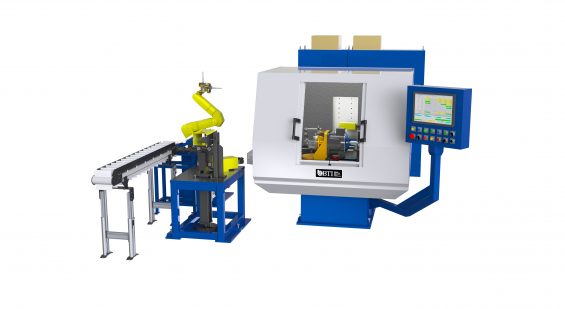
Fully Automatic Turbo Charger Shaft & Wheel Cell
Fully Automatic Turbo Charger Shaft & Wheel Cell Featuring Automatic 2-Plane CBN Wet Grind Correction, Dimensional Gaging, Robotic Part Handling, and Conveyance
View More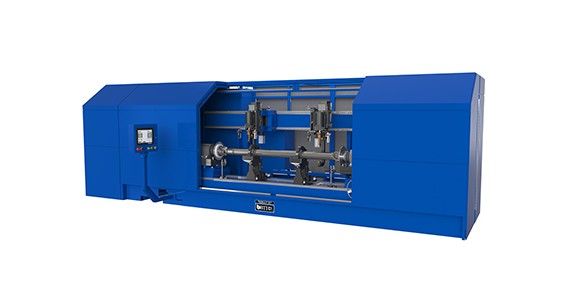
1-2 Piece Driveshaft Balancer, Auto Weld Correction
Fully-Automatic 1 or 2 Piece Driveshaft Balancer with Automatic Resistance Weld Correction for Steel & Aluminum Shafts Featuring Auto Guard Doors, Excessive Vibration Shutoff...
View More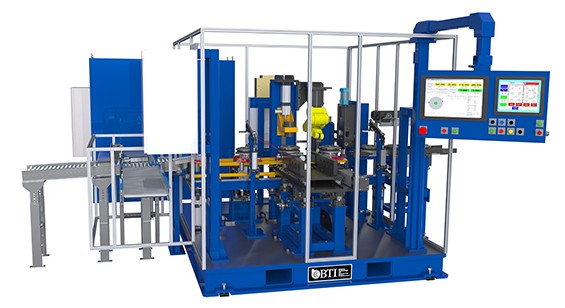
5-Station Turbine Damper Assembly Balancer
Fully-Automatic 5-Station Turbine Damper Assembly Balancer with Automatic Variable & Fixed Length Weight Making, Featuring Projection Weld Correction and Part Sorting
View More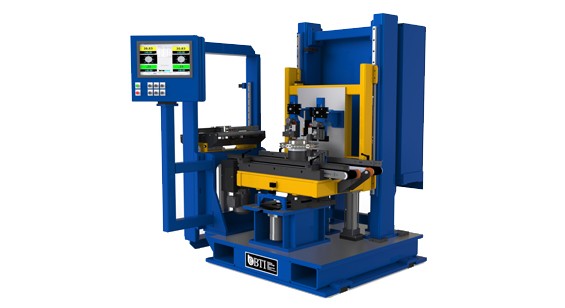
Fully-Automatic Brake Rotor Combination Bore & Multi-Attribute Gage
Fully-Automatic Brake Rotor Combination Bore & Multi-Attribute Gage Featuring Temperature Compensation and Auto Feedback to Upstream Machining Operations
View More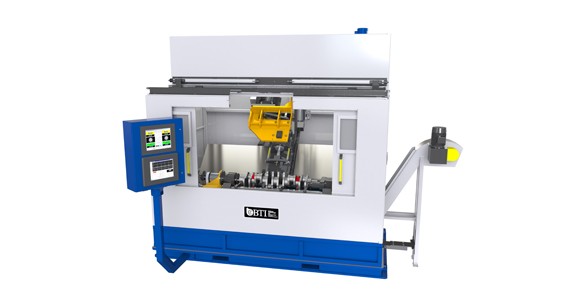
Crankshaft Balancer, Spindle Drill & Gantry Load
Fully-Automatic Crankshaft Balancer with High Pressure Coolant Through The Spindle Drill Correction and Overhead Gantry Load
View More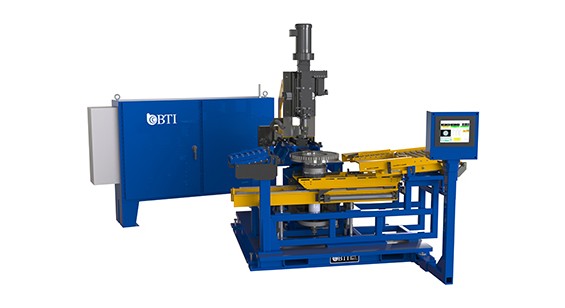
Fully-Automatic Heavy Duty Flywheel Balancer with Automatic Drill Correction and...
Fully-Automatic Heavy Duty Flywheel Balancer with Automatic Drill Correction and Load/Unload Assist Elevator
View More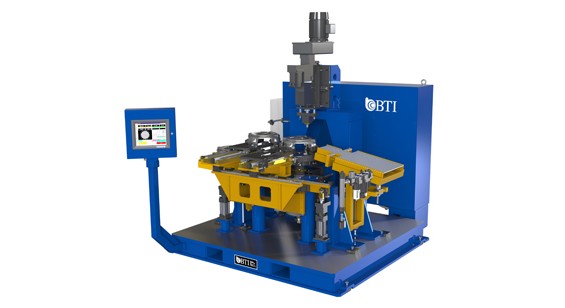
Fully-Automatic Large Clutch Housing Balancer with Automatic Drill Correction
Fully-Automatic Large Clutch Housing Balancer with Automatic Drill Correction
View More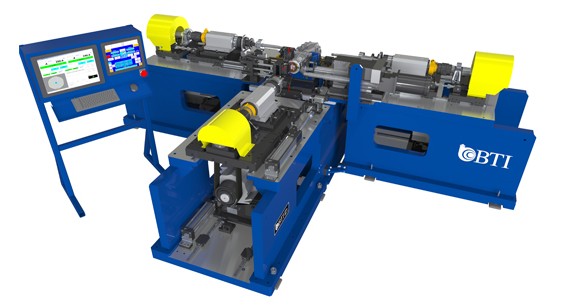
RDM Balancer & NVH Combination w/ Drill Correction
Fully-Automatic RDM Balancer & NVH Combination. Featuring Drill Correction, Laser Gaging, Drive Shaft Hung Mass Simulation and Advanced Clutch Conditioning Technology
View More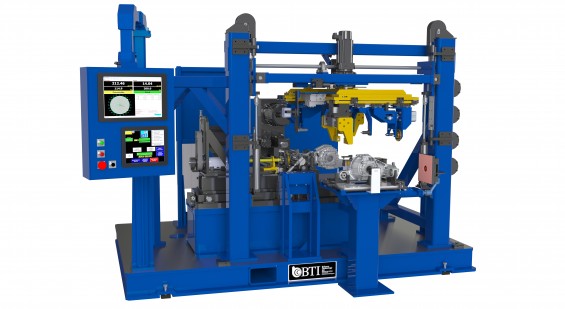
Fully-Automatic RDM Balancer Featuring Automatic Mill or Drill Correction
Fully-Automatic RDM Balancer Featuring Automatic Mill or Drill Correction, 180 Degree Rotary Load/Unload Station, Vision System to Detect Part Orientation, Part ID Scanner &...
View More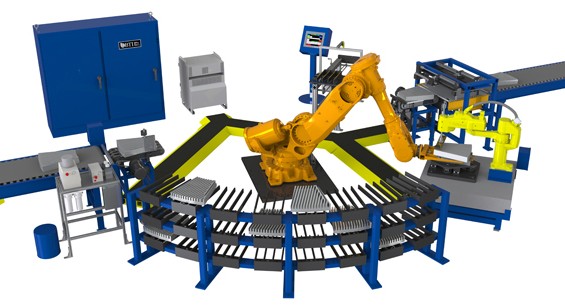
Fully-Automatic Refiner Plate Cell
Fully-Automatic Refiner Plate Cell Featuring Gaging and C.G. Measurement of Individual Plates for Predictive Balance Optimization when Assembled Per the Cell’s Advanced Sequencing and...
View More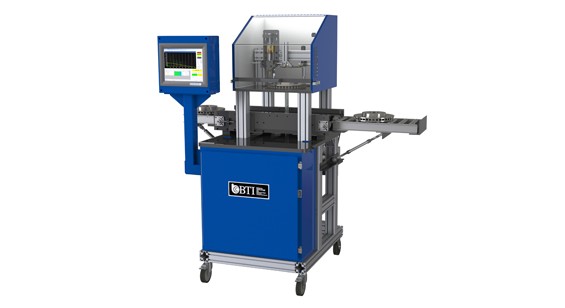
Fully-Automatic Resonant Frequency Measurement Station
Fully-Automatic Resonant Frequency Measurement Station
View More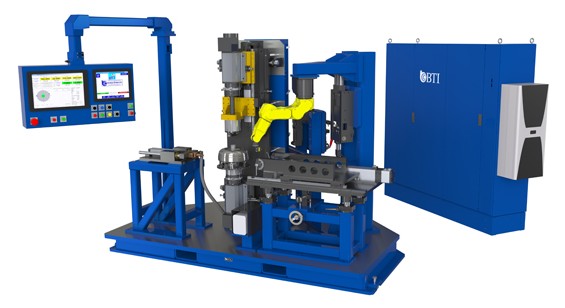
Single Station Torque Convertor Balancer
Fully-Automatic Single Station Torque Convertor Assembly Balancer with Automatic Variable and Fixed Length Weight Making and Weld Correction. Featuring Dual Motorized Spindles for Low...
View More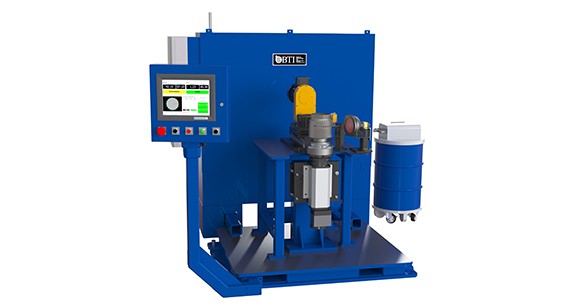
Transmission Clutch Housing Balancer, Drill Correction
Fully-Automatic Transmission Clutch Housing Balancer with Automatic Radial Drill Correction and Chip Containment System
View More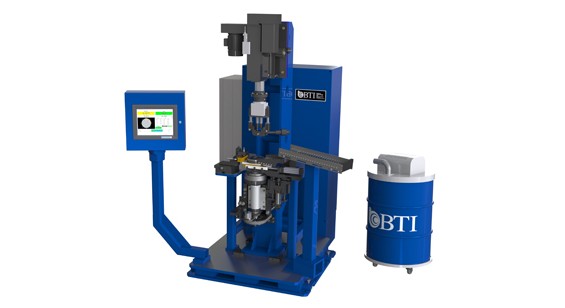
Harmonic Vibration Damper Balancer
Semi-Automatic Harmonic Vibration Damper Balancer with Automatic Servo Drill Correction, Featuring V-groove Dimensional Gaging, Auto Unload and Chip Containment
View More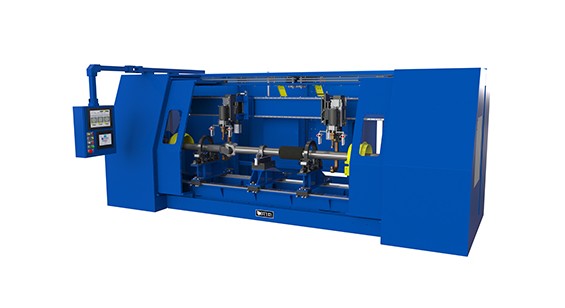
Heavy Duty 1 or 2 Piece Driveshaft Balancer with Resistance Weld Correction
Heavy Duty 1 or 2 Piece Driveshaft Balancer with Resistance Weld Correction Featuring Excessive Vibration Shutoff and Dual Servo Drives for Joint Loading and...
View More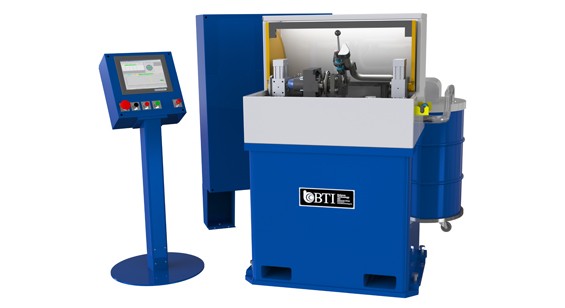
High Speed Assembly Balancer for Automotive Industry
Automatic High Speed Turbo Charger CHRA Core Assembly Balancer with Touch Up Grinder, Oil Pumping with Flow & Temperature Monitoring […]
View More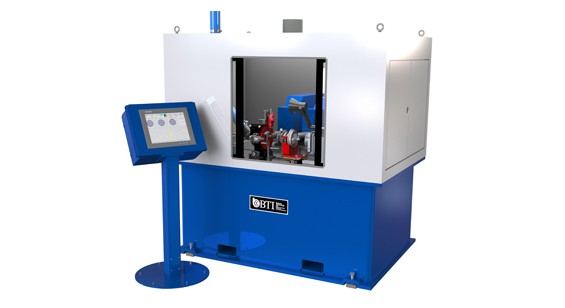
High Speed Turbo Charger Core Assembly 2 Plane Balancer
300,000 rpm High Speed Turbo Charger Core Assembly 2 Plane Balancer with Automatic Mill and Drill Correction, Featuring Pulsation Measurement, “G” Measurement, RPM sweep,...
View More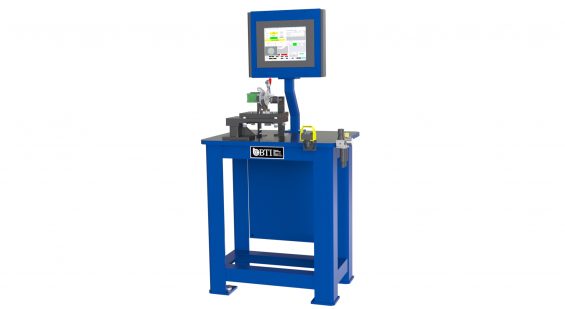
Horizontal Healthcare Fan / Blower Assembly Balancer
Horizontal Healthcare Fan / Blower Assembly Balancer with Programable Power Supply and Quick Connect Wire Harness.
View More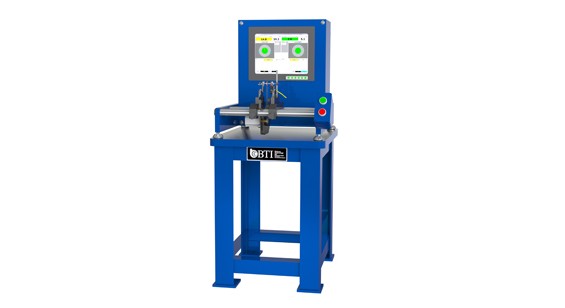
Horizontal Speedometer/Tachometer Needle Balancer
Horizontal Speedometer/Tachometer Needle Balancer
View More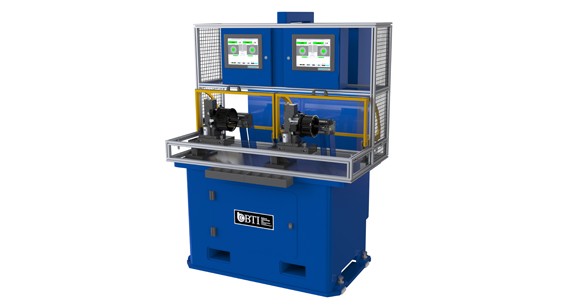
HVAC Fan Module Balancer and Motor Testing
Dual Station HVAC Fan Module Balancer Featuring Blade Counting, Motor Testing and Segmented Weight Correction
View More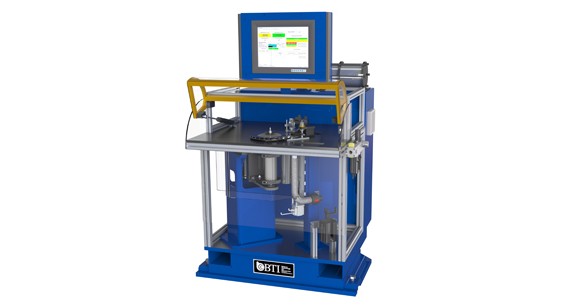
Impeller Balancer with Automatic Mill correction and Laser Gaging of Axial Run-O...
Impeller Balancer with Automatic Mill correction and Laser Gaging of Axial Run-Out
View More
Low- and High-Speed Turbo Charger Core Assembly 2 Plane Balancer
4,000 to 300,000 rpm Low- and High-Speed Turbo Charger Core Assembly 2 Plane Balancer with Touch-Up Grinder, featuring Pulsation Measurement, “G” Measurement, and Oil...
View More
Manual Torsional Test Stand for Front Axle Assemblies.
Manual Torsional Test Stand for Front Axle Assemblies.
View More
Moment Balancer for Helicopter Blades and Propellers
Moment Balancer for Helicopter Blades and Propellers
View More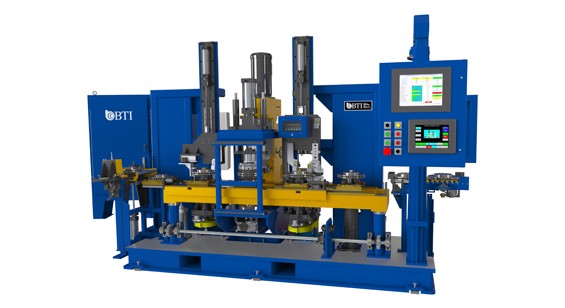
Multi-Station Combination Brake Rotor Machine
Fully Automatic Multi-Station Combination Brake Rotor Machine featuring Balancing with Mill Correction, Dimensional Gaging, Surface Finish Measurement, Eddy Current Crack Detection, and Part Marking
View More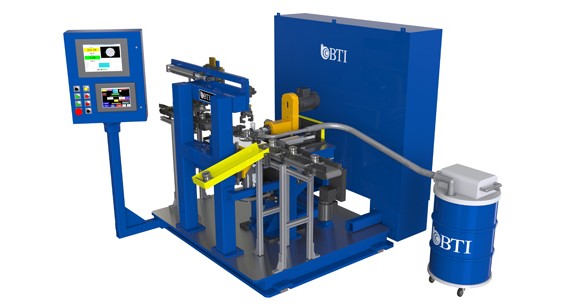
Multi-Station Flange Balancer with Correction Mill
Multi-Station Flange Balancer with Correction Mill
View More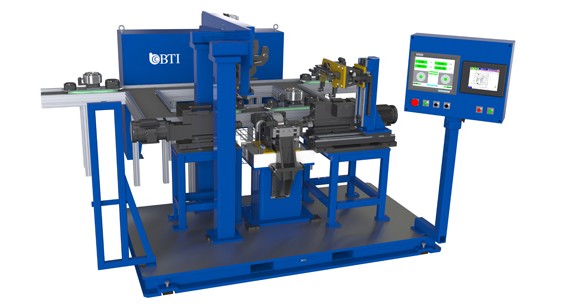
Multi-Station Magnetized Electric Armature Balancer
Fully Automatic Multi-Station Magnetized Electric Armature Balancer featuring Palletized Part Conveyance, Dual-Axial Drill Correction, and Heavy Spot Ink Marking
View More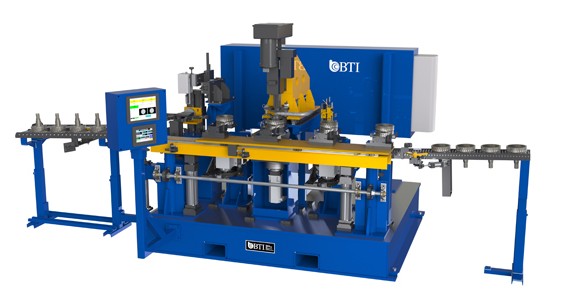
Multi-Station Transmission Carrier Combination Machine
Fully Automatic Multi-Station Transmission Carrier Combination Machine featuring Dimensional Gaging, Balancing with Automatic Drill Correction, Part Orientation Flipper, and Pin Stamp Marker
View More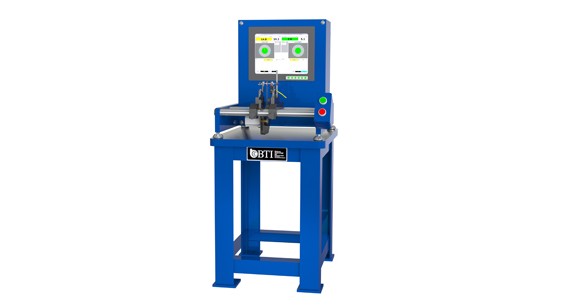
PC Cooling Fan Module Assembly Balancer with Motor Testing
PC Cooling Fan Module Assembly Balancer with Motor Testing
View More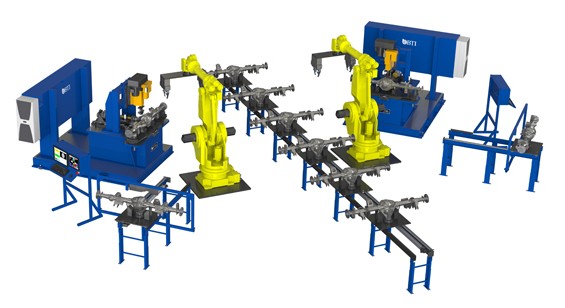
Rear Axle Cell featuring Two Drill Correction Balancers
Fully Automatic Rear Axle Cell featuring Two Drill Correction Balancers, Two Robots, Palletized Part Conveyance, Master Part Housing Stations, Part Marking, and RFID Traceability
View More
Replacement PC’s & PLC’s for all Brands and Models
Replacement PC’s & PLC’s for all Brands and Models
View More
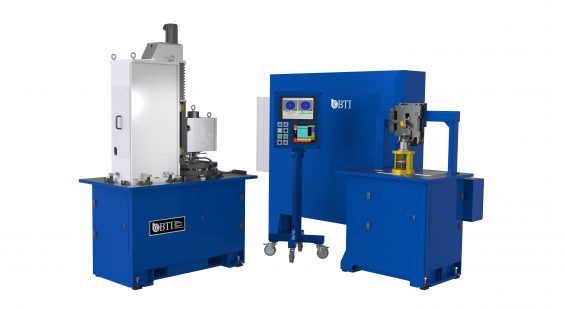
Semi Automatic Two Station Turbine Wheel Mass Center and Audit Machine
Semi Automatic Two Station Turbine Wheel Mass Center and Audit Machine
View More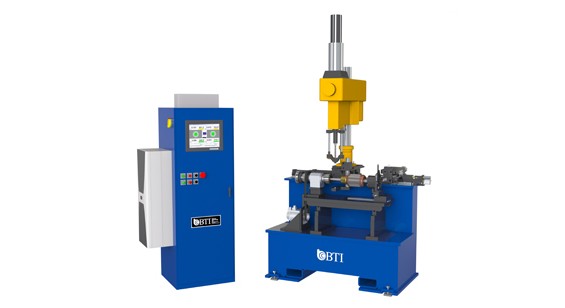
Semi-Automatic Armature Balancer, Drill Correction
Semi-Automatic Armature Balancer with Automatic Drill Correction and Automatic Servo-Controlled Commutator Lathe
View More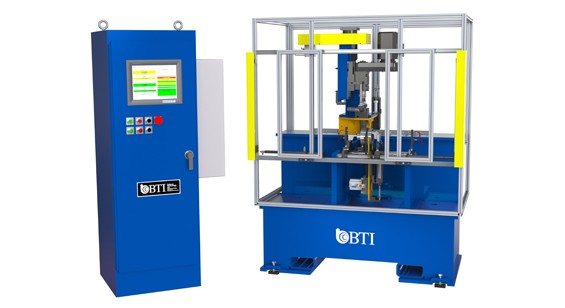
Semi-Automatic Clutch Housing Balancer with Automatic Drill Correction and Chip ...
Semi-Automatic Clutch Housing Balancer with Automatic Drill Correction and Chip Containment
View More
Semi-Automatic Compressor Wheel Air Bearing Audit Station
Semi-Automatic Compressor Wheel Air Bearing Audit Station Featuring Servo Controlled Whisper Drive Technology
View More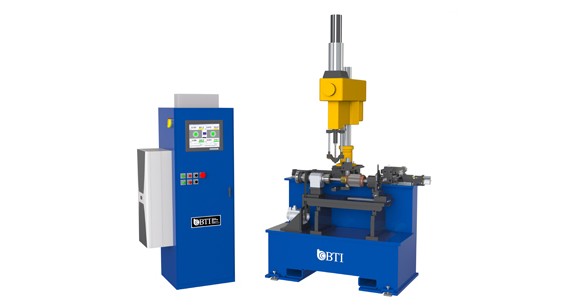
Semi-Automatic Crankshaft Balancer, Hook End Drive
Semi-Automatic Crankshaft Balancer Featuring Hook End Drive, Automatic Drill Correction, Paint Marker and Chip Containment System
View More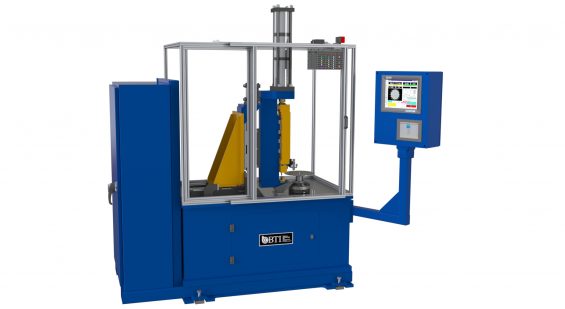
Semi-Automatic Drive Plate Balancer with Punch Correction and Slug Containment.
Semi-Automatic Drive Plate Balancer with Punch Correction and Slug Containment.
View More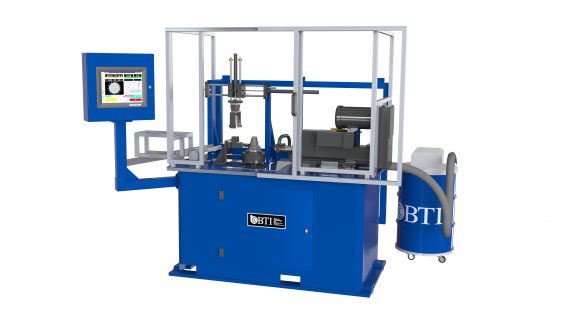
Semi-Automatic Flange Balancer with Mill Correction and Auto-Unload.
Semi-Automatic Flange Balancer with Mill Correction and Auto-Unload.
View More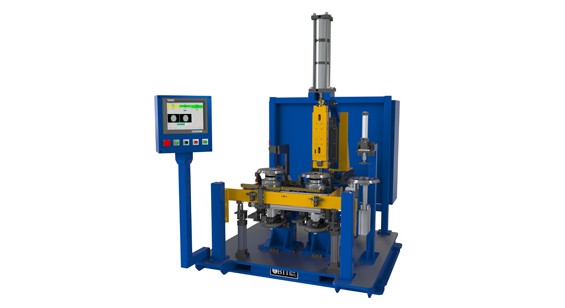
Semi-Automatic Flywheel Balancer
Semi-Automatic Flywheel Balancer with Automatic Pierce Correction, Slug Collection System, Pin Stamp Marking, Radial & Axial Dimensional Gaging
View More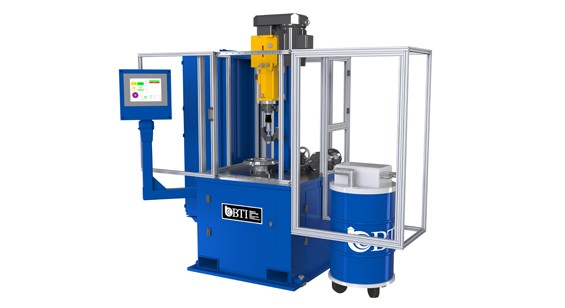
Semi-Automatic Flywheel Balancer with Automatic Drill Correction
Semi-Automatic Flywheel Balancer with Automatic Drill Correction
View More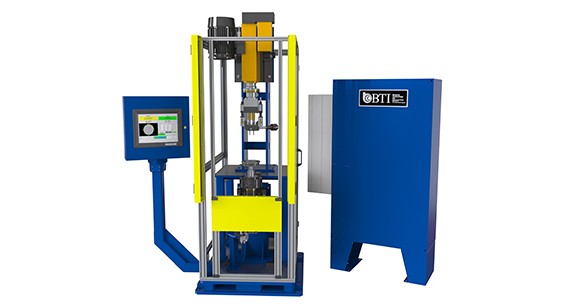
Semi-Automatic Harmonic Damper Balancer with Automatic Dual Drill Correction
Semi-Automatic Harmonic Damper Balancer with Automatic Dual Drill Correction and Vacuum Chip Removal
View More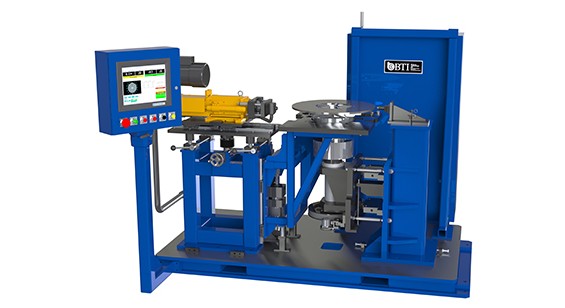
Semi-Automatic Heavy Duty Unvented Brake Rotor Balancer
Semi-Automatic Heavy Duty Unvented Brake Rotor Balancer with Automatic Radial Drill Correction and Load/Unload Assist Elevator
View More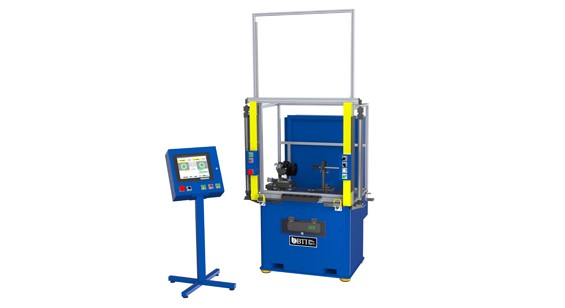
Semi-Automatic HVAC Fan Module Balancer
Semi-Automatic HVAC Fan Module Balancer Featuring Quick Disconnect Tooling for Multiple Part Models, Blade Counting, Motor Testing and Segmented Weight Correction
View More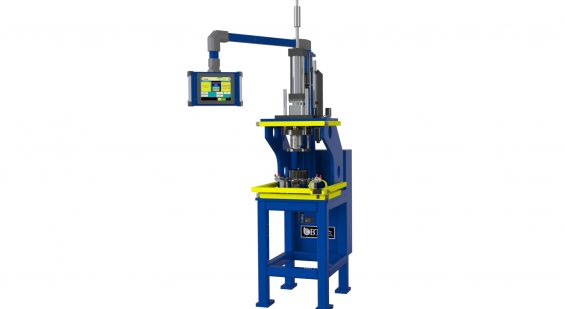
Semi-Automatic HVAC Fan Wheel / Motor Press Station. Capable of Pressing to both...
Semi-Automatic HVAC Fan Wheel / Motor Press Station. Capable of Pressing to both a Force and a Distance.
View More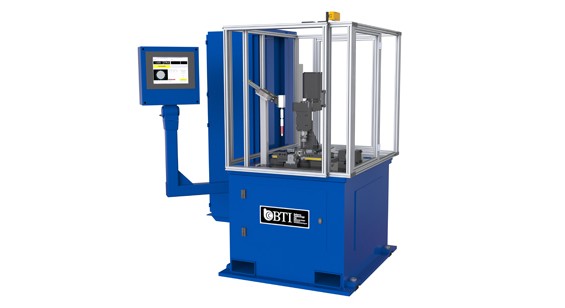
Semi-Automatic Reaction Carrier Balancer with Automatic Mill Correction and Part...
Semi-Automatic Reaction Carrier Balancer with Automatic Mill Correction and Part Marking
View More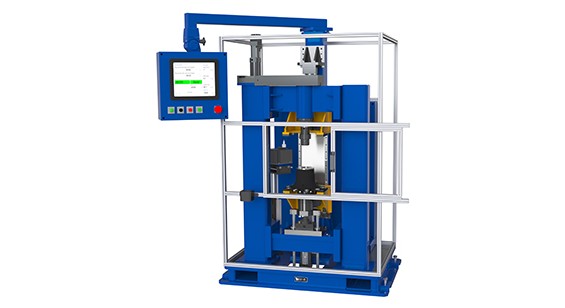
Semi-Automatic Rear Brake Hub Dynamic Axial Endplay and Bore Gage
Semi-Automatic Rear Brake Hub Dynamic Axial Endplay and Bore Gage
View More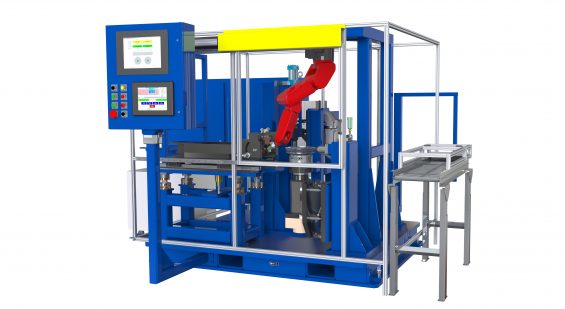
Semi-Auto Single Station Torsional Damper Balancer
Semi-Automatic Single Station Dynamic Torsional Damper Balancer with Automatic Projection Weld Correction
View More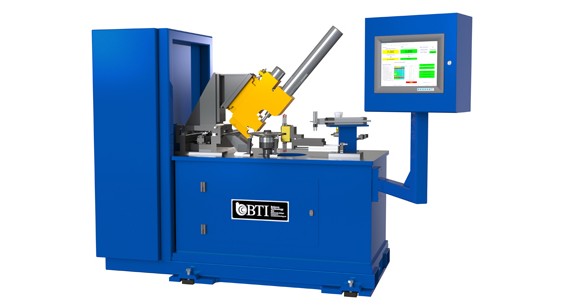
Semi-Automatic Torsional Machine Featuring
Semi-Automatic Torsional Damper Combination Machine Featuring Balancing with Automatic Pierce Correction, Dimensional Gaging, Part Marking, Rivet and Disallowed Area Sensing
View More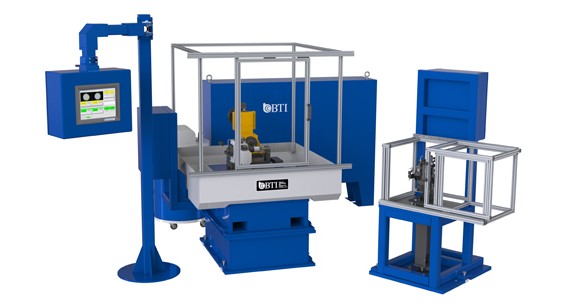
Semi-Automatic Turbo Charger Compressor Wheel Balance
Semi-Automatic Turbo Charger Compressor Wheel Balance Cell Featuring Air-Bearing Measurement Technology and Automatic Mill Correction
View More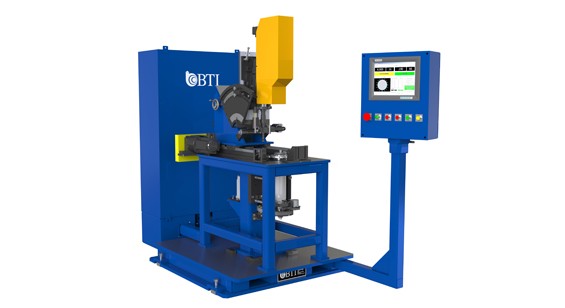
Semi-Automatic X-Ray Target Balancer
Semi-Automatic X-Ray Target Balancer with Automatic Servo Drill Correction Featuring Automatic Drill Changeover to Accommodate a Wide Varity of Parts without Operator Intervention
View More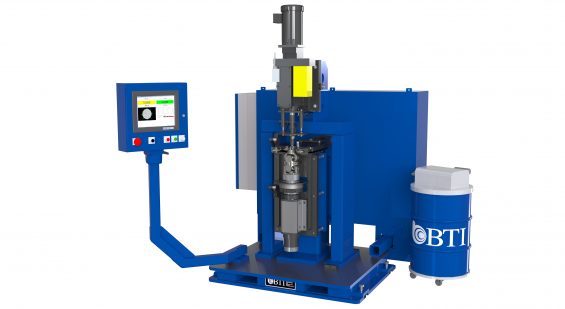
Semi-Automatic Yoke Assembly Balancer
Semi-Automatic Yoke Assembly Balancer with Drill Correction and Chip Containment
View More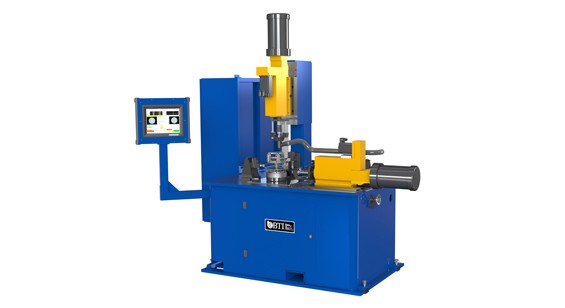
Snowmobile Clutch Balancer
Semi-Automatic Snowmobile Clutch Balancer with Automatic Axial & Radial Drill Correction
View More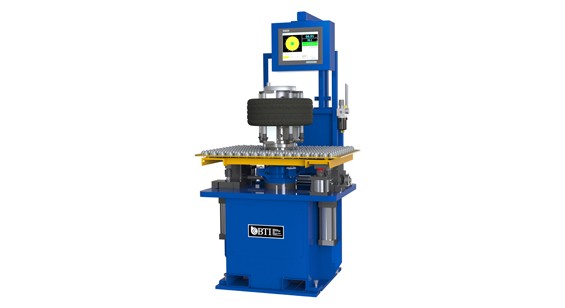
Static Aircraft Tire Balancer with Load Assist Elevator
Static Aircraft Tire Balancer with Load Assist Elevator
View More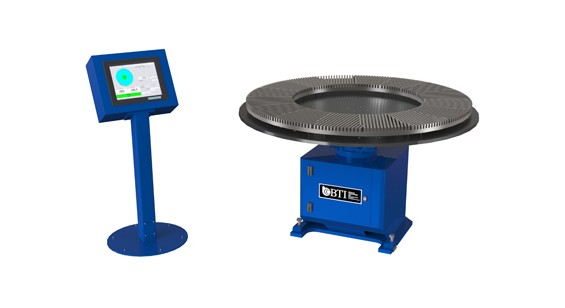
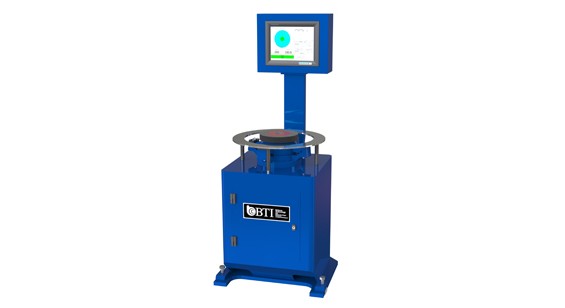
Static Grinding Wheel Audit Station with Pneumatic Tooling
Static Grinding Wheel Audit Station with Pneumatic Tooling
View More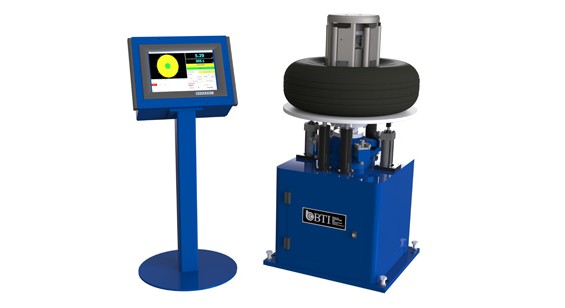
Static Tire Balancer with Pneumatic Paddle Style Tooling and Load Assist Elevato...
Static Tire Balancer with Pneumatic Paddle Style Tooling and Load Assist Elevator
View More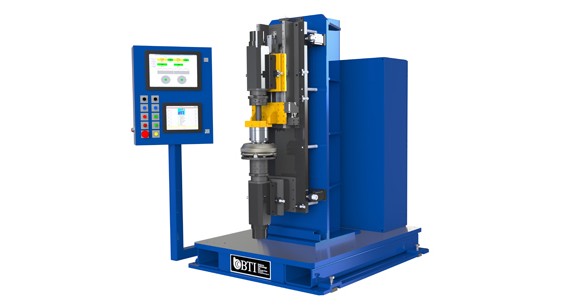
Torque Convertor Measure Station
Torque Convertor Measure Station Featuring Dual Motorized Spindles with Multiple Measurement Techniques (Static Internal, 180 Flip and Differential Measurement)
View More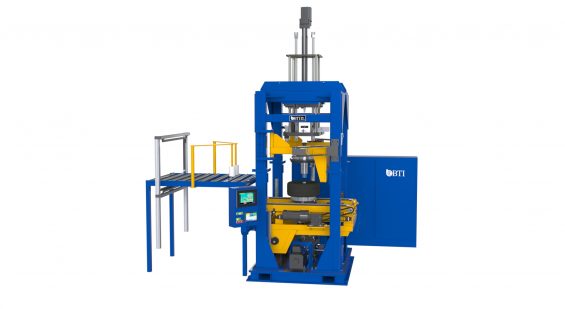
Truck Tire Inflator Balancer
Large Dynamic Truck Tire Inflator Balancer Featuring Radial & Lateral Laser Runout, Bead Lubrication, Load/Unload Elevator & Hot Stamp Unbalance Marking System.
View More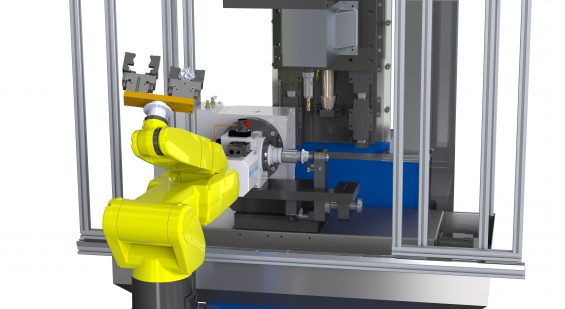
Turbo Charger Compressor Wheel Balancer
Fully Automatic Turbo Charger Compressor Wheel Balancer with 2-Plane BTI Mill Correction Station Featuring Robotic Part handling
View MoreGet Started
Get in touch with us. We're here to assist you.
Connect with our measurement experts and get the technical guidance your application demands.
