Balancing Machine Rebuilds & Retrofits
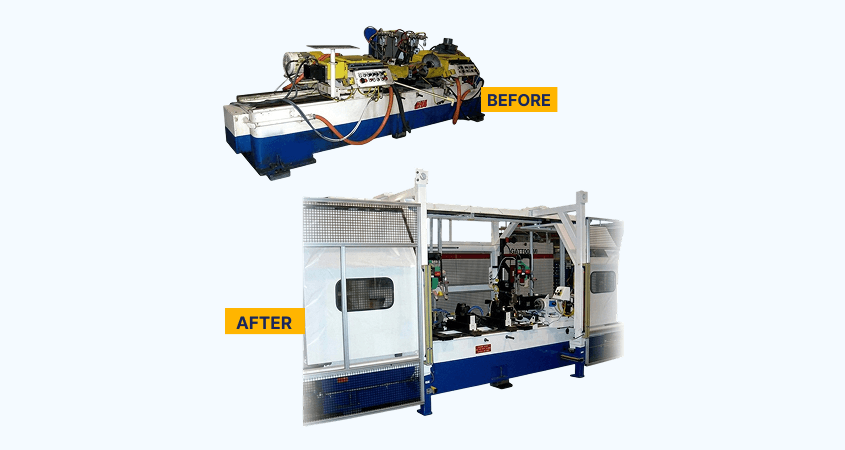
Balance Technology has been building machines since 1968, and a great many of them are still in production. The mechanical structure of a well-built balancing machine, gage or test stand (the base, the bearings, the spindle, the ways) will outlast several generations of the electronics and software that control it. Rebuilding that machine rather than replacing it is often the better engineering decision and almost always the better capital decision.
BTI rebuilds and retrofits balancers, gages and test stands, with scope and acceptance criteria defined after assessment.
Why Machines Get Rebuilt
The controls are obsolete
An industrial PC from fifteen years ago runs an operating system no one will patch, on hardware no one stocks. The spindle it commands may be in excellent condition. This is the single most common reason a machine comes back to us.
The part changed
A new program, a different family, a tighter tolerance or a higher rate. Frequently the existing machine can hold it with new tooling, revised software and a correction station upgrade.
Accuracy has drifted
Wear in bearings, belts, drives and tooling accumulates. Repeatability degrades slowly enough that nobody notices until a customer does.
Safety and compliance standards moved
Guarding, interlocks, light curtains, lockout provisions and electrical standards have all tightened since many machines were built. A plant audit is often what starts the conversation.
Data requirements appeared
A machine that was specified to print a label is now expected to write a record per serial number into a plant quality system.
The plant is moving
Machines get relocated between facilities, and a relocation is the natural moment to bring a machine current and recertify it in its new home.
Common Upgrades
- New industrial computer and current operating system
- PLC replacement and reprogramming
- Motor, servo and drive replacement
- Measurement electronics and transducer replacement
- Repair and replacement of wear items
- Replacement guarding to current standards
- New proximity sensors, cabling, plumbing and pneumatics
- Added automation, including robots and dedicated transfers
- Process and feature additions: new measurements, new stations, new correction methods
- Plant location compliance and certification
- Cleaning and paint
- Refurbished or replaced tooling
Rebuilding a Machine
The scope of a rebuild depends on who built the machine. Select the machine you have to see how the project differs.
When the machine is one we built, we have the original design behind it: the assembly drawings, the electrical schematics, the software, the calibration records and the build history. That changes what a rebuild can be. We are not reverse engineering your machine. We are returning to a design we know and bringing it current.
What Having the Original Design Actually Buys You
We know what it was capable of when it left. The original acceptance data tells us what the machine achieved new. That is the benchmark a rebuild is measured against, rather than a guess about what a machine of that vintage ought to do.
We know which parts are wear items and which are structural. A rebuild scope built on the actual bill of materials spends money on the bearings, drives and tooling that degrade, and leaves alone the castings and weldments that do not.
We can source or make the parts. Where a component is obsolete, we have the drawing and can manufacture it or engineer a current equivalent into the same envelope.
We understand the measurement chain. When accuracy has drifted, knowing how the original measurement system was designed is the difference between diagnosing the cause and replacing components until the symptom goes away.
The upgrade path is real. Adding crack detection, dimensional gaging or surface measurement to an existing BTI balancer turns it into a combination machine, and we know from the drawings whether the base, the spindle and the envelope will carry it.
How a Rebuild Runs
Assessment. We start from the machine’s serial number and pull its build record. Then we look at the machine itself (on site, or here once it arrives) and establish its current condition against what it was built to do.
Scope. A written scope that separates what must be done to restore the machine from what you may want to do to improve it. Those are different budgets and often different decisions, and we would rather you see them separately.
Rebuild. Disassembly, inspection, repair or replacement, reassembly, rewire, new controls and software, and tooling refurbishment as scoped.
Runoff. The machine is run on your parts, against the acceptance criteria agreed in the scope, before it ships. Where the rebuild includes new capability, that capability is demonstrated on your parts too.
Installation and training. Reinstallation, recertification in place, and training for the people who will run and maintain it, who are frequently not the people who were there when it was new.
A machine built by another manufacturer can still be a good machine. If the base is sound, the spindle is true and the mechanical design suits the part, the fact that someone else built it is not a reason to scrap it, even when that someone else no longer supports it, no longer exists, or no longer wants the job.
Balance Technology rebuilds and retrofits balancing machines, gages and test stands built by other manufacturers. It is a different kind of project than rebuilding one of our own, and we are straightforward about the difference: we start without the original drawings, without the source code and without the build record. What we bring instead is more than 14,000 machines of this class designed and built since 1968, which means we can work out what a machine was doing and why.
Why Customers Bring Us Other Manufacturers’ Machines
The original builder is gone. Acquired, closed, or exited the product line. Nobody answers the phone, and the spares are whatever is left on your shelf.
Support exists but doesn’t fit how the plant needs to run.
The controls are obsolete. An unsupported operating system, a PLC out of production, a drive nobody stocks, a proprietary measurement card with no replacement. Meanwhile the iron is fine.
The software is a dead end. Source code was never delivered, the people who wrote it have moved on, and no one can change a part program, a tolerance or a data export format.
The machine never quite worked. This is more common than the industry admits. A machine that was commissioned marginally and has been fought with ever since, where the underlying problem is fixturing, datum scheme or measurement approach rather than components.
You want it to do more. Add a measurement, add a station, add automation, add data.
How We Approach a Machine We Did Not Build
Assessment first, always. We do not quote a competitor rebuild from photographs. We need to understand the mechanical condition, the measurement chain, the control architecture and what the machine is actually doing now versus what it is supposed to do. On a machine of unknown provenance, the assessment is the most important part of the project, and we treat it as its own piece of work.
Keep the iron, replace the intelligence. The usual outcome. Bases, weldments, spindles and ways from a reputable builder are frequently excellent and expensive to reproduce. Controls, software, sensors, drives and tooling are where obsolescence lives and where we can bring the machine fully current with our own systems.
Our control system, our software. When we retrofit, the machine gets a BTI control system and BTI software. That is the point: afterward, the machine is supportable by us, with part programs you can change, data you can export, and a phone number that is answered. A retrofit that leaves the proprietary black box in place solves nothing.
Re-establish the measurement chain. We work out how the machine locates the part, what it measures against, and whether that datum scheme matches your print. On machines that never performed well, this is usually where the problem has been hiding.
Prove it on your parts. Acceptance is run against criteria written into the scope, on your parts, before the machine goes back to work.
Adding Capability
A retrofit is often the cheapest way to get a capability you do not currently have. If a competitor’s balancer already spins your part on a precise axis, adding eddy current crack detection, dimensional gaging, surface measurement or resonant frequency testing to that spindle turns it into a combination machine for a fraction of what a new combination machine costs.
Whether the existing structure will carry the addition (the envelope, the rigidity, the access, the cycle time) is a question the assessment answers. Sometimes the answer is no, and we say so before anyone spends money.
What We Cannot Do
We will not tell you we can do something we have not established we can do.
We do not reverse engineer proprietary software to keep it running. If the existing software is the problem, the answer is to replace it with ours, not to patch something we did not write and cannot support.
We do not warrant the parts of the machine we did not touch. A scope that replaces the controls does not make us responsible for a spindle bearing we never opened, and we will be explicit in the scope about where that line falls.
Where the mechanical design is fundamentally unsuited to what you now need (wrong capacity, wrong speed range, wrong correction method, structure worn past economical repair) we will recommend a new machine, even though a retrofit would have been easier to sell.
Rebuild or Replace
We build new machines, so we have an obvious interest here, and we try to be straight about it.
Rebuild usually wins when the base, spindle and structure are sound, the machine’s fundamental capacity still suits the part, and the problems are in controls, wear items, tooling or compliance. Most machines that come back to us are in that category.
Replacement usually wins when the part family has outgrown the machine’s capacity or speed range, when the required cycle time is beyond what the mechanical design can reach, when the structure itself is damaged or worn past economical repair, or when what you actually need is a different machine that happens to resemble the one you have.
The assessment tells us which. We will say so.
What to Send Us to Start
- Manufacturer, model and serial number, and any documentation you still have
- Photographs of the machine, the control cabinet and the HMI
- What it does now, what it is supposed to do, and where the gap is
- Part drawings, with the datums and tolerances that matter
- Required throughput
- Any capability you want added
- Whatever the plant knows about its history: repairs, relocations, modifications
Do not worry about gaps in that list. Missing documentation is the normal condition of these projects, not a disqualifier.
Frequently Asked Questions
How old is too old?
We have rebuilt machines from the 1970s. Age matters far less than condition and than whether the original capacity fits what you need now. Send us the serial number and we can start from the build record.
Do we have to ship the machine to you?
Not always. Control upgrades, software, tooling and some mechanical work can be done in your plant. Full rebuilds (particularly anything involving the spindle, the base or a rewire) are better done here, where the machine can be properly disassembled and run off.
Can you make it do something it never did?
Often. Adding measurement stations, correction methods, automation or data handling to an existing machine is routine work for us. Whether a particular addition fits depends on the machine’s structure and envelope, which is exactly what the assessment answers.
What if nobody here knows how the machine was originally set up?
That is normal and it is not a problem. The build record is ours, not yours. Give us the serial number.
What if we bought the machine used from someone else?
Still fine. If we built it, we have its record, regardless of how many owners it has had since.
Will you work on a machine from any manufacturer?
We work on balancing machines, gages and test stands from a wide range of builders, domestic and imported. The assessment determines whether a specific machine is a sensible rebuild candidate. We have not found the brand to be the deciding factor: condition and fit to the part are.
We have no drawings and no software. Is that fatal?
No. It is the usual starting point. We establish what the machine does by examining it, and we replace the control and measurement layers with our own, which we do have the drawings and source for.
Can you support it afterward?
Yes, for what we installed. After a control and software retrofit, the parts of the machine that fail and change over time are ours, which is most of the reason customers do this.
Is a retrofit cheaper than a new machine?
Usually, substantially. But not always: a machine needing major mechanical work plus full controls can approach the cost of new, without the warranty or the service life. The assessment is what tells you which situation you are in, and we would rather you know before committing.
Can you relocate and recertify a machine at the same time?
Yes, and a plant move is a good moment to do it. The machine is coming apart anyway.
If you’re not looking for a rebuild or retrofit, BTI can provide new equipment, too. BTI engineers and manufactures other types of industrial precision measurement and testing equipment, including static and dynamic balancing equipment, dimensional gages, mass centering equipment, eddy current crack detection systems, surface finish measurement equipment, NVH equipment (noise vibration and harshness), functional test stands, spinners, motor testers, and Resonant Frequency Measurement Systems. We also engineer and manufacture specialized test systems, including torque-to-turn, backlash, end play, and destructive test equipment.
Additionally, BTI’s unique ability to combine the aforementioned technologies into one fully integrated system enables our clients to reduce capital expenditures, increase product quality, and minimize floor space requirements. There is no need for costly conveyors and escapements to connect independent machines together; nor do you need to train operators on multiple machines. There is one seamless, easy-to-use operator interface with unprecedented networking, statistical, and diagnostic capability.
Whether you need a fully integrated, combined technology system (e.g., a balancer/gage/NVH combo) or independent machines, let our team of mechanical, electrical, and software engineers design and build a configured-to-order system for you.
If you don’t see the product you are looking for, or have specific questions, please contact us.
Other solutions
200,000 lb Capacity Horizontal Balancer for Steam and Gas Turbines
200,000 lb Capacity Horizontal Balancer for Steam and Gas Turbines
View More
30,000 rpm Automatic Spin Tester for Induction & Permanent Magnet Electric ...
30,000 rpm Automatic Spin Tester for Induction & Permanent Magnet Electric Vehicle Rotors.
View More
300,000 RPM Turbo Charger Balancer, Wheel Milling
Fully-Automatic 300,000 rpm High Speed Turbo Charger Assembly Balancer with Automatic Compressor Wheel Milling & Drilling Correction. Featuring Servo Controlled Air Drive System, Oil...
View More
300,000 rpm Turbo Charger Core Assembly 2 Plane Balancer
4,000 to 300,000 rpm Low and High Speed Turbo Charger Core Assembly 2 Plane Balancer with Touch Up Grinder, Featuring Pulsation Measurement & “G”...
View More
5-Station Armature Balancer with 2 Plane Contour
6-Second (600 part per hour) Fully Automatic 5-Station Armature Balancer with 2 Plane Contour or V-Cut Mill Correction
View More
5-Station Torque Convertor Assembly Balancer
Fully Automatic 5-Station Torque Convertor Assembly Balancer with Automatic Variable and Fixed Length Weight Making and Weld Correction, featuring Automatic Walking Beam Transfer, Oil...
View More
6-Station Armature Balancer w/ Axial Drill Correction
220 Part Per Hour Fully-Automatic 6-Station Armature Balancer Featuring Dual Axial Drill Correction, Walking-Beam Transfer, Overhead Belt Drive and Part Sorting
View More
Induction & Permanent Magnet Rotor Cell
Automated Induction & Permanent Magnet Electric Rotor Cell Featuring two 6-Station balancers, six 30,000 rpm Automatic Spin Testers and Four Robots
View More
Automatic 2-Station Induction Balance Solution
Automatic 2-Station Induction & Permanent Magnet Electric Rotor Cell Featuring two Independent Balance Stations, Dual Drills on Each Station, Scissor […]
View More
Automatic Crankshaft Balancer with Dual Servo MQL Drill Correction
Fully Automatic Crankshaft Balancer with Dual Servo MQL Drill Correction and Overhead Gantry Load Screen reader support enabled. Fully Automatic Crankshaft Balancer with Dual...
View More
Low Speed Turbo Charger CHRA Assembly Balancer
Automatic Low Speed Turbo Charger CHRA Core Assembly Balancer with Dual Drive Technology, Featuring both Belt and Servo Controlled Air Drive Systems as well...
View More
Automatic Permanent Magnet Rotor Balancer
Fully Automatic Permanent Magnet Rotor Balancer, featuring Automatic 2-Plane Axial Drill Correction, Pneumatic Pick and Place Transfer, and Palletized Part Conveyance
View More
Automatic Rear Axle Balancer With Automatic Drill Correction
1000 lb Fully Automatic Rear Axle Balancer Featuring Automatic Drill Correction and Part Marking
View More
Automatic Single Station Induction & Permanent Magnet Electric Rotor Cell F...
Automatic Single Station Induction & Permanent Magnet Electric Rotor Cell Featuring Dual Drills and Scissor Belt Drive
View More
Automatic Torsional Test Stand for Steering Column Tulip Assemblies.
Automatic Torsional Test Stand for Steering Column Tulip Assemblies.
View More
Automatic Turbo Charger Compressor Wheel
Fully Automatic Turbo Charger Compressor Wheel Cell Featuring Automatic 2-Plane Mill Correction, Dimensional Gaging, Eddy Current Surface Defect Detection, 2D Laser Marking, Robotic Part...
View More
Balancer with Elevator Mill Correction Station
Single station Brake Rotor Balancer with Elevator Load/Unload and Onboard BTI Mill Correction Station. Featuring Dimensional Gaging of Key Attributes such as Flatness, Parallelism,...
View More
Bench-top Horizontal Balancer for Measuring Unbalance
Bench-top Horizontal Balancer for Measuring Unbalance of Computer Hard Drive Disc Reader Heads
View More
Brake Rotor Bore Gage with Temperature Compensation and Auto Feedback to Upstrea...
Brake Rotor Bore Gage with Temperature Compensation and Auto Feedback to Upstream Machining Operations
View More
BTI’s Patented Spindle-Less CAT, BT & HSK Tool Holder Balancer
BTI’s Patented Spindle-Less CAT, BT & HSK Tool Holder Balancer
View More
Combination Machine Featuring Dimensional Gaging
Fully-Automatic Combination Machine Featuring Dimensional Gaging and Surface Roughness Measurement of Torque Converter Assemblies
View More
Compressor Wheel Cell Gaging & Surface Detection
Fully Automatic Turbo Charger Compressor Wheel Cell Featuring Dimensional Gaging, Eddy Current Surface Defect Detection, 2D Laser Marking and Conveyance
View More
Crack Detection Brake Rotors System
Fully-Automatic Eddy Current Crack Detection System for Brake Rotors
View More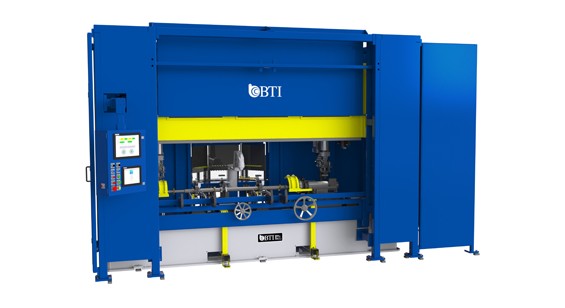
Driveshaft Balancer with Automatic Spot Weld Correction
Fully Automatic 1, 2, and 3 Piece Driveshaft Balancer with Automatic Spot Weld Correction via Magazine Feed Weights, featuring Auto Guard Doors, 5-Plane Balance...
View More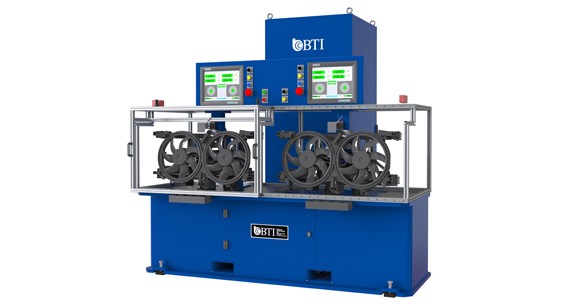
Dual Engine Fan Balancer
Two Station Dual Engine Cooling Fan Balancer Featuring Advanced Blade Counting, Speed and Direction Verification System and Electrical Motor & PWM Function Tests
View More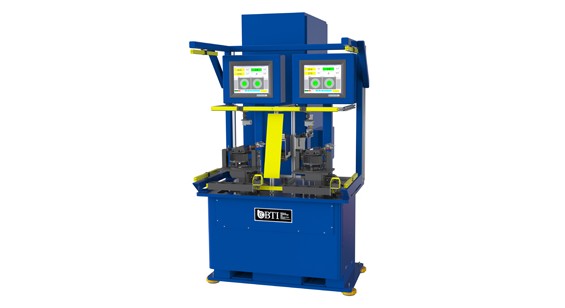
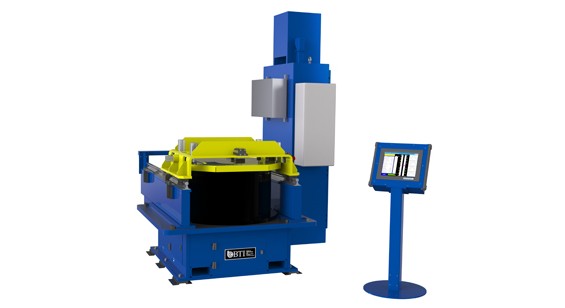
Durability Tester for Grinding Wheels
Semi-Automatic High Speed Durability Tester for Grinding Wheels
View More
Dynamic Aluminum Fan Balancer with Automatic Rivet Correction
Dynamic Aluminum Fan Balancer with Automatic Rivet Correction
View More
Dynamic Brake Rotor Balancer
Semi-Automatic Single Station Dynamic Brake Rotor Balancer with Automatic Mill Correction
View More
Dynamic Tire Inflator Balancer with Bead Lubrication
Fully Automatic Dynamic Tire Inflator Balancer with Bead Lubrication, Laser Gaging, and Ink Stamp Marking
View More
Dynamic Wheel Combination Machine
Fully Automatic Dynamic Wheel Combination Machine featuring Part Identification, Axial and Radial Laser Gaging, and Balance Audit with Orient and Mark
View More
Engine Cooling Fan Module Balancer and Motor Tester
Engine Cooling Fan Module Balancer and Motor Tester
View More
Flywheel Balancer with Automatic Drill Correction
Semi-Automatic Flywheel Balancer with Automatic Drill Correction, Ring Gear Sensor, and Load Assist Elevator
View More
Flywheel Balancer with Manual Drill Correction
Flywheel Balancer with Manual Drill Correction Featuring Drill Depth Readout
View More
Shaft & Wheel Balancer, Laser Mapping & CBN Grinding
Full Automatic Shaft & Wheel Balancer with Laser Mapping, CBN Grinding, High Pressure Coolant, Ultra-Sonic Part Contact Sensor, Conveyance & Robot Load/Unload
View More
Fully Automatic 5-Station Armature Balancer with 2 Plane Contour
6-Second (600 part per hour) Fully Automatic 5-Station Armature Balancer with 2 Plane Contour or V-Cut Mill Correction
View More
Fully Automatic RDM Balancer and NVH Combination
Fully Automatic RDM Balancer and NVH Combination featuring Drill Correction, Laser Gaging, Drive Shaft Hung Mass Simulation, and Advanced Clutch Conditioning Technology
View More
Rear Axle Balancer with Automatic Drill Correction
Fully Automatic Rear Axle Balancer featuring Automatic Drill Correction, Part Marking, and RFID Traceability
View More
Fully Automatic Rear Drive Module Balancer
Fully Automatic Rear Drive Module Balancer Featuring Automatic Drill Correction, Part Marking, and RFID Traceability
View More
Fully Automatic Rear Drive Module Cell featuring Two Drill Correction Balancers
Fully Automatic Rear Drive Module Cell featuring Two Drill Correction Balancers, Robot with Dual End Effectors, Palletized Part Conveyance, Master Part Housing Stations, Part...
View More
Fully Automatic Six Station Induction & Permanent Magnet Electric Motor Ro...
Fully Automatic Six Station Induction & permanent Magnet Electric Motor Rotor Balancer Featuring Overhead Belt Drive System, Two Drill Correction Stations, Chip Containment and...
View More
Fully Automatic Stator Balancer with Mill Correction and Walking-Beam Transfer
Fully Automatic Stator Balancer with Mill Correction and Walking-Beam Transfer
View More
Fully Automatic Turbo Charger Shaft & Wheel Cell
Fully Automatic Turbo Charger Shaft & Wheel Cell Featuring Automatic 2-Plane CBN Wet Grind Correction, Dimensional Gaging, Robotic Part Handling, and Conveyance
View More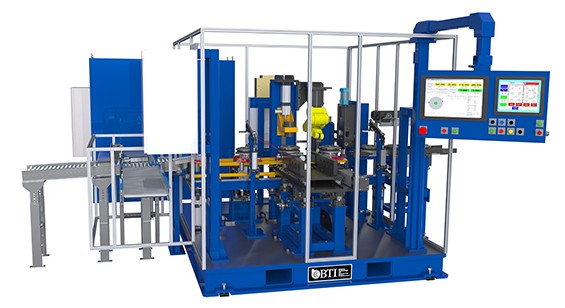
5-Station Turbine Damper Assembly Balancer
Fully-Automatic 5-Station Turbine Damper Assembly Balancer with Automatic Variable & Fixed Length Weight Making, Featuring Projection Weld Correction and Part Sorting
View More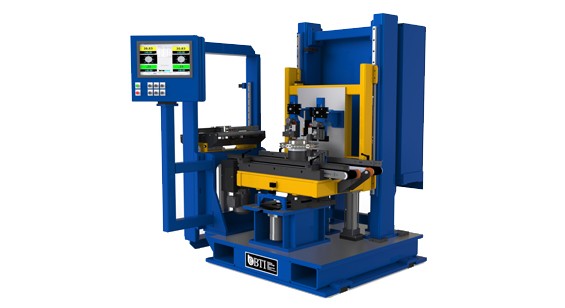
Fully-Automatic Brake Rotor Combination Bore & Multi-Attribute Gage
Fully-Automatic Brake Rotor Combination Bore & Multi-Attribute Gage Featuring Temperature Compensation and Auto Feedback to Upstream Machining Operations
View More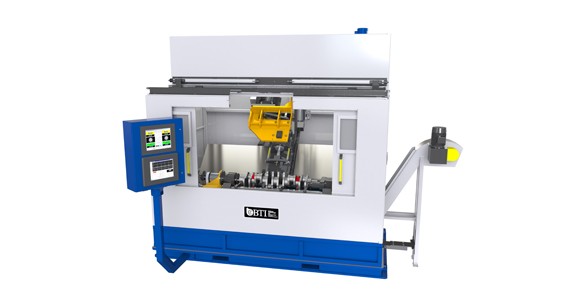
Crankshaft Balancer, Spindle Drill & Gantry Load
Fully-Automatic Crankshaft Balancer with High Pressure Coolant Through The Spindle Drill Correction and Overhead Gantry Load
View More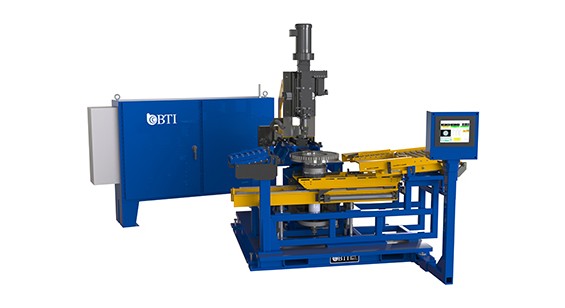
Fully-Automatic Heavy Duty Flywheel Balancer with Automatic Drill Correction and...
Fully-Automatic Heavy Duty Flywheel Balancer with Automatic Drill Correction and Load/Unload Assist Elevator
View More
Fully-Automatic Large Clutch Housing Balancer with Automatic Drill Correction
Fully-Automatic Large Clutch Housing Balancer with Automatic Drill Correction
View More
RDM Balancer & NVH Combination w/ Drill Correction
Fully-Automatic RDM Balancer & NVH Combination. Featuring Drill Correction, Laser Gaging, Drive Shaft Hung Mass Simulation and Advanced Clutch Conditioning Technology
View More
Fully-Automatic RDM Balancer Featuring Automatic Mill or Drill Correction
Fully-Automatic RDM Balancer Featuring Automatic Mill or Drill Correction, 180 Degree Rotary Load/Unload Station, Vision System to Detect Part Orientation, Part ID Scanner &...
View More
Fully-Automatic Refiner Plate Cell
Fully-Automatic Refiner Plate Cell Featuring Gaging and C.G. Measurement of Individual Plates for Predictive Balance Optimization when Assembled Per the Cell’s Advanced Sequencing and...
View More
Fully-Automatic Resonant Frequency Measurement Station
Fully-Automatic Resonant Frequency Measurement Station
View More
Single Station Torque Convertor Balancer
Fully-Automatic Single Station Torque Convertor Assembly Balancer with Automatic Variable and Fixed Length Weight Making and Weld Correction. Featuring Dual Motorized Spindles for Low...
View More
Transmission Clutch Housing Balancer, Drill Correction
Fully-Automatic Transmission Clutch Housing Balancer with Automatic Radial Drill Correction and Chip Containment System
View More
Harmonic Vibration Damper Balancer
Semi-Automatic Harmonic Vibration Damper Balancer with Automatic Servo Drill Correction, Featuring V-groove Dimensional Gaging, Auto Unload and Chip Containment
View More
High Speed Assembly Balancer for Automotive Industry
Automatic High Speed Turbo Charger CHRA Core Assembly Balancer with Touch Up Grinder, Oil Pumping with Flow & Temperature Monitoring […]
View More
High Speed Turbo Charger Core Assembly 2 Plane Balancer
300,000 rpm High Speed Turbo Charger Core Assembly 2 Plane Balancer with Automatic Mill and Drill Correction, Featuring Pulsation Measurement, “G” Measurement, RPM sweep,...
View More
Horizontal Healthcare Fan / Blower Assembly Balancer
Horizontal Healthcare Fan / Blower Assembly Balancer with Programable Power Supply and Quick Connect Wire Harness.
View More
Horizontal Speedometer/Tachometer Needle Balancer
Horizontal Speedometer/Tachometer Needle Balancer
View More
HVAC Fan Module Balancer and Motor Testing
Dual Station HVAC Fan Module Balancer Featuring Blade Counting, Motor Testing and Segmented Weight Correction
View More
Impeller Balancer with Automatic Mill correction and Laser Gaging of Axial Run-O...
Impeller Balancer with Automatic Mill correction and Laser Gaging of Axial Run-Out
View More
Low- and High-Speed Turbo Charger Core Assembly 2 Plane Balancer
4,000 to 300,000 rpm Low- and High-Speed Turbo Charger Core Assembly 2 Plane Balancer with Touch-Up Grinder, featuring Pulsation Measurement, “G” Measurement, and Oil...
View More
Manual Torsional Test Stand for Front Axle Assemblies.
Manual Torsional Test Stand for Front Axle Assemblies.
View More
Moment Balancer for Helicopter Blades and Propellers
Moment Balancer for Helicopter Blades and Propellers
View More
Multi-Station Combination Brake Rotor Machine
Fully Automatic Multi-Station Combination Brake Rotor Machine featuring Balancing with Mill Correction, Dimensional Gaging, Surface Finish Measurement, Eddy Current Crack Detection, and Part Marking
View More
Multi-Station Flange Balancer with Correction Mill
Multi-Station Flange Balancer with Correction Mill
View More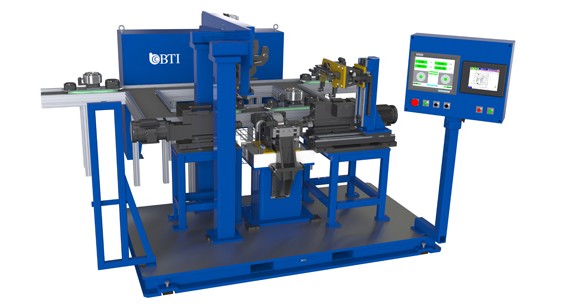
Multi-Station Magnetized Electric Armature Balancer
Fully Automatic Multi-Station Magnetized Electric Armature Balancer featuring Palletized Part Conveyance, Dual-Axial Drill Correction, and Heavy Spot Ink Marking
View More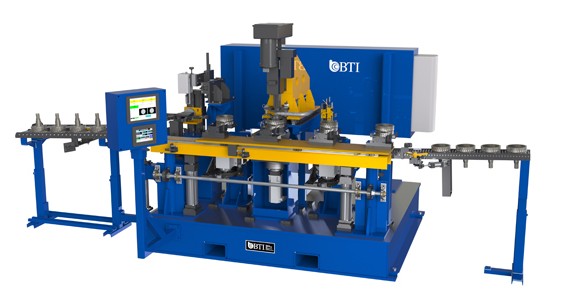
Multi-Station Transmission Carrier Combination Machine
Fully Automatic Multi-Station Transmission Carrier Combination Machine featuring Dimensional Gaging, Balancing with Automatic Drill Correction, Part Orientation Flipper, and Pin Stamp Marker
View More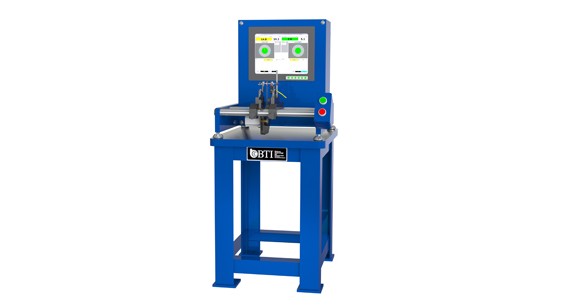
PC Cooling Fan Module Assembly Balancer with Motor Testing
PC Cooling Fan Module Assembly Balancer with Motor Testing
View More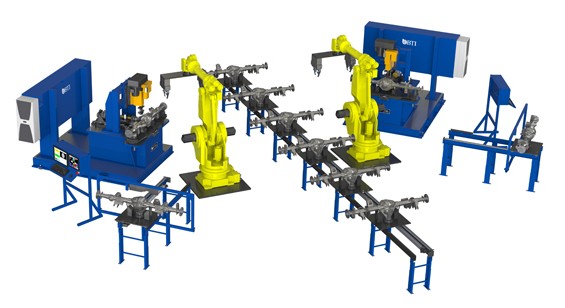
Rear Axle Cell featuring Two Drill Correction Balancers
Fully Automatic Rear Axle Cell featuring Two Drill Correction Balancers, Two Robots, Palletized Part Conveyance, Master Part Housing Stations, Part Marking, and RFID Traceability
View More
Replacement PC’s & PLC’s for all Brands and Models
Replacement PC’s & PLC’s for all Brands and Models
View More
Semi Automatic Two Station Turbine Wheel Mass Center and Audit Machine
Semi Automatic Two Station Turbine Wheel Mass Center and Audit Machine
View More
Semi-Automatic Armature Balancer, Drill Correction
Semi-Automatic Armature Balancer with Automatic Drill Correction and Automatic Servo-Controlled Commutator Lathe
View More
Semi-Automatic Clutch Housing Balancer with Automatic Drill Correction and Chip ...
Semi-Automatic Clutch Housing Balancer with Automatic Drill Correction and Chip Containment
View More
Semi-Automatic Compressor Wheel Air Bearing Audit Station
Semi-Automatic Compressor Wheel Air Bearing Audit Station Featuring Servo Controlled Whisper Drive Technology
View More
Semi-Automatic Crankshaft Balancer, Hook End Drive
Semi-Automatic Crankshaft Balancer Featuring Hook End Drive, Automatic Drill Correction, Paint Marker and Chip Containment System
View More
Semi-Automatic Drive Plate Balancer with Punch Correction and Slug Containment.
Semi-Automatic Drive Plate Balancer with Punch Correction and Slug Containment.
View More
Semi-Automatic Flange Balancer with Mill Correction and Auto-Unload.
Semi-Automatic Flange Balancer with Mill Correction and Auto-Unload.
View More
Semi-Automatic Flywheel Balancer
Semi-Automatic Flywheel Balancer with Automatic Pierce Correction, Slug Collection System, Pin Stamp Marking, Radial & Axial Dimensional Gaging
View More
Semi-Automatic Flywheel Balancer with Automatic Drill Correction
Semi-Automatic Flywheel Balancer with Automatic Drill Correction
View More
Semi-Automatic Harmonic Damper Balancer with Automatic Dual Drill Correction
Semi-Automatic Harmonic Damper Balancer with Automatic Dual Drill Correction and Vacuum Chip Removal
View More
Semi-Automatic Heavy Duty Unvented Brake Rotor Balancer
Semi-Automatic Heavy Duty Unvented Brake Rotor Balancer with Automatic Radial Drill Correction and Load/Unload Assist Elevator
View More
Semi-Automatic HVAC Fan Module Balancer
Semi-Automatic HVAC Fan Module Balancer Featuring Quick Disconnect Tooling for Multiple Part Models, Blade Counting, Motor Testing and Segmented Weight Correction
View More
Semi-Automatic HVAC Fan Wheel / Motor Press Station. Capable of Pressing to both...
Semi-Automatic HVAC Fan Wheel / Motor Press Station. Capable of Pressing to both a Force and a Distance.
View More
Semi-Automatic Reaction Carrier Balancer with Automatic Mill Correction and Part...
Semi-Automatic Reaction Carrier Balancer with Automatic Mill Correction and Part Marking
View More
Semi-Automatic Rear Brake Hub Dynamic Axial Endplay and Bore Gage
Semi-Automatic Rear Brake Hub Dynamic Axial Endplay and Bore Gage
View More
Semi-Auto Single Station Torsional Damper Balancer
Semi-Automatic Single Station Dynamic Torsional Damper Balancer with Automatic Projection Weld Correction
View More
Semi-Automatic Torsional Machine Featuring
Semi-Automatic Torsional Damper Combination Machine Featuring Balancing with Automatic Pierce Correction, Dimensional Gaging, Part Marking, Rivet and Disallowed Area Sensing
View More
Semi-Automatic Turbo Charger Compressor Wheel Balance
Semi-Automatic Turbo Charger Compressor Wheel Balance Cell Featuring Air-Bearing Measurement Technology and Automatic Mill Correction
View More
Semi-Automatic X-Ray Target Balancer
Semi-Automatic X-Ray Target Balancer with Automatic Servo Drill Correction Featuring Automatic Drill Changeover to Accommodate a Wide Varity of Parts without Operator Intervention
View More
Semi-Automatic Yoke Assembly Balancer
Semi-Automatic Yoke Assembly Balancer with Drill Correction and Chip Containment
View More
Snowmobile Clutch Balancer
Semi-Automatic Snowmobile Clutch Balancer with Automatic Axial & Radial Drill Correction
View More
Static Aircraft Tire Balancer with Load Assist Elevator
Static Aircraft Tire Balancer with Load Assist Elevator
View More
Static Grinding Wheel Audit Station with Pneumatic Tooling
Static Grinding Wheel Audit Station with Pneumatic Tooling
View More
Static Tire Balancer with Pneumatic Paddle Style Tooling and Load Assist Elevato...
Static Tire Balancer with Pneumatic Paddle Style Tooling and Load Assist Elevator
View More
Torque Convertor Measure Station
Torque Convertor Measure Station Featuring Dual Motorized Spindles with Multiple Measurement Techniques (Static Internal, 180 Flip and Differential Measurement)
View More
Truck Tire Inflator Balancer
Large Dynamic Truck Tire Inflator Balancer Featuring Radial & Lateral Laser Runout, Bead Lubrication, Load/Unload Elevator & Hot Stamp Unbalance Marking System.
View More
Turbo Charger Compressor Wheel Balancer
Fully Automatic Turbo Charger Compressor Wheel Balancer with 2-Plane BTI Mill Correction Station Featuring Robotic Part handling
View MoreGet Started
Get in touch with us. We're here to assist you.
Connect with our measurement experts and get the technical guidance your application demands.