Household Appliances & Power Tools
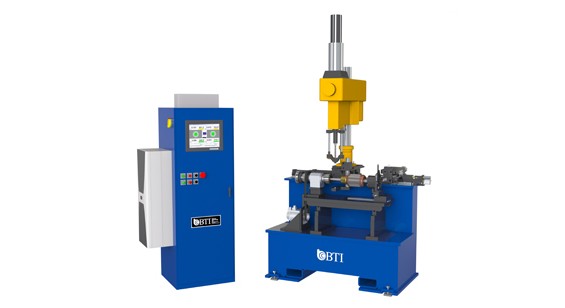
Balance Technology Inc. builds balancing machines and measurement systems for appliance and power tool manufacturing: motor armatures and rotors, washer drums and baskets, blower wheels and fans, pump impellers, tool rotors and spindles, and grinder and saw arbors. BTI has been designing this equipment in Whitmore Lake, Michigan since 1968. This is high-volume work, and that changes what the machine has to be. A balancer on an appliance or power tool line is a production asset measured on cycle time and uptime as much as on measurement accuracy. It has to hold tolerance at takt, load and unload quickly, and run for years with minimal intervention.What BTI Balances in Appliances and Power Tools
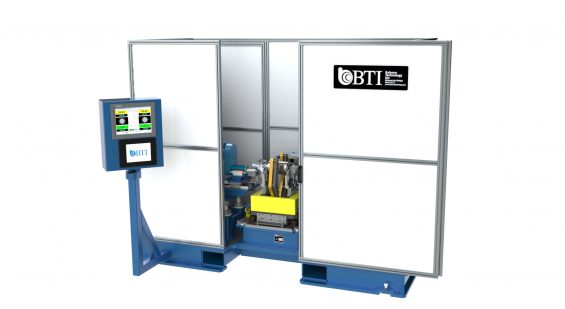
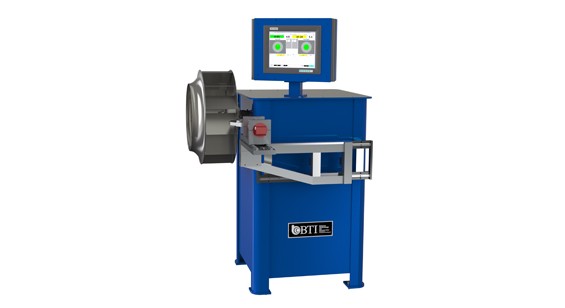
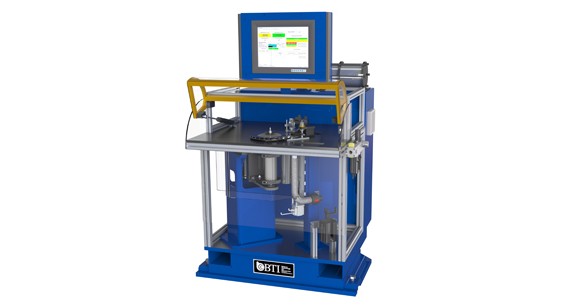
BTI balancing machines are built on four platforms (VNR (vertical non-rotator), H (horizontal cradle), VR (vertical rotator) and P (platform suspension)) plus spinners and test stands. The platform follows the part geometry and how it has to be held; the correction method follows the material and where there is room to add or remove mass.| Component | Typical platform | Correction method |
|---|---|---|
| Motor armatures and rotors | H, VR | Mill, drill, weight-add |
| Washer drums and baskets | VNR, P | Weight-add |
| Blower wheels and fans | VNR, H | Drill, weight-add |
| Pump impellers | VR | Mill, weight-add |
| Power tool rotors and spindles | VR, spinner | Grind, mill |
| Grinder and saw arbors | VR | Grind, mill |
| Vacuum motor fans | VNR, VR | Drill, weight-add |
How a Machine Gets Sized
A BTI machine designation names a platform and a class. The number is a class, not a part weight limit: it describes the size and load envelope of the base. Sizing works from the tooling and the part together, not the part alone. Tooling is not specified until the part prints are reviewed and the fixture is concepted, and the heavier the tooling-plus-part assembly is relative to the class, the less repeatable the measurement becomes. A shop that needs one machine to cover a wide range of parts, and does not need tight repeatability, can run a much broader weight range on a given class than a production program can. Tell BTI the part weight and BTI will name a class the same day. See BTI machine platforms for the full platform and class architecture.Balance Grade and Tolerance
Appliance and power tool rotors are light and fast, which places most of them at the tighter end of the grade range. Balance tolerances are set by ISO 21940-11, which superseded ISO 1940-1. The standard assigns a balance quality grade G, and the permissible residual specific unbalance follows from that grade and the service speed: eper = (G × 60) ÷ (2π × n) where eper is permissible residual specific unbalance in g·mm/kg, G is the balance quality grade in mm/s, and n is the service speed in rev/min. Permissible residual unbalance is then U = eper × m, divided across the correction planes.| Grade | Typical components |
|---|---|
| G 6.3 | Fans, pump impellers, normal electric armatures |
| G 2.5 | Power tool rotors and special electric armatures |
| G 1 | Precision spindles and high-speed tool assemblies |
| G 0.4 | The tightest grade in the standard, for precision grinder spindles |
High Volume and Cycle Time
At production volumes the balancing operation has to fit the line rather than the other way around. That means the measurement, the correction and the part handling are specified together: a machine that measures accurately but cannot load and unload at takt is not a solution. It also changes how correction is chosen. Milling a defined band is repeatable and fast on a fixture built for one part family; drilling suits cast components with material to remove; weight-add covers finished or coated parts that cannot be cut. Which one fits is settled when the fixture is concepted from the part print, alongside the required production rate. Where a line already runs capable mechanical bases, a PC upgrade often recovers measurement performance and modern controls without replacing the machine.Correction Methods
| Method | Where it fits |
|---|---|
| Mill | Controlled removal on a defined correction band, suited to volume |
| Drill | Cast components with material available to remove |
| Grind | Hardened or finished surfaces, including tool spindles |
| Weight-add | Drums, baskets and finished assemblies |
| Adhesive and applied weight | Plastics and coated parts |
Standards
BTI certifies machines to ISO 21940, SAE International balancing specifications, and DIN specifications. Where a program carries a measurement system capability requirement, BTI evaluates the part and the process first, then confirms what is achievable and commits to it in the machine specification.Frequently Asked Questions
Can a balancer keep up with an appliance line takt time?
That is a specification question rather than a yes or no. Tell BTI the required production rate along with the part print and BTI will confirm what the machine and tooling have to be to hold tolerance at that rate.
Why do small power tool rotors need tight grades?
Permissible residual unbalance falls as service speed rises and scales with rotor mass. A light rotor at high speed therefore lands at a small residual figure, which is why these parts sit at G 2.5 or tighter.
Does BTI rebuild or retrofit existing balancing machines?
Yes, including machines built by other manufacturers. See BTI rebuilds and retrofits, competitor rebuilds and retrofits, and PC upgrades for machines still mechanically sound.
What information does BTI need to quote a machine?
The part print, the part weight, the service speed, the balance tolerance if one is specified, and the required production rate. Lead times are quoted in weeks at the time of quotation and move with current backlog.

Connect with us
To contact us regarding your project - or if you have any questions - please click the button below :
Request a QuoteGet Started
Get in touch with us. We're here to assist you.
Connect with our measurement experts and get the technical guidance your application demands.