Computers
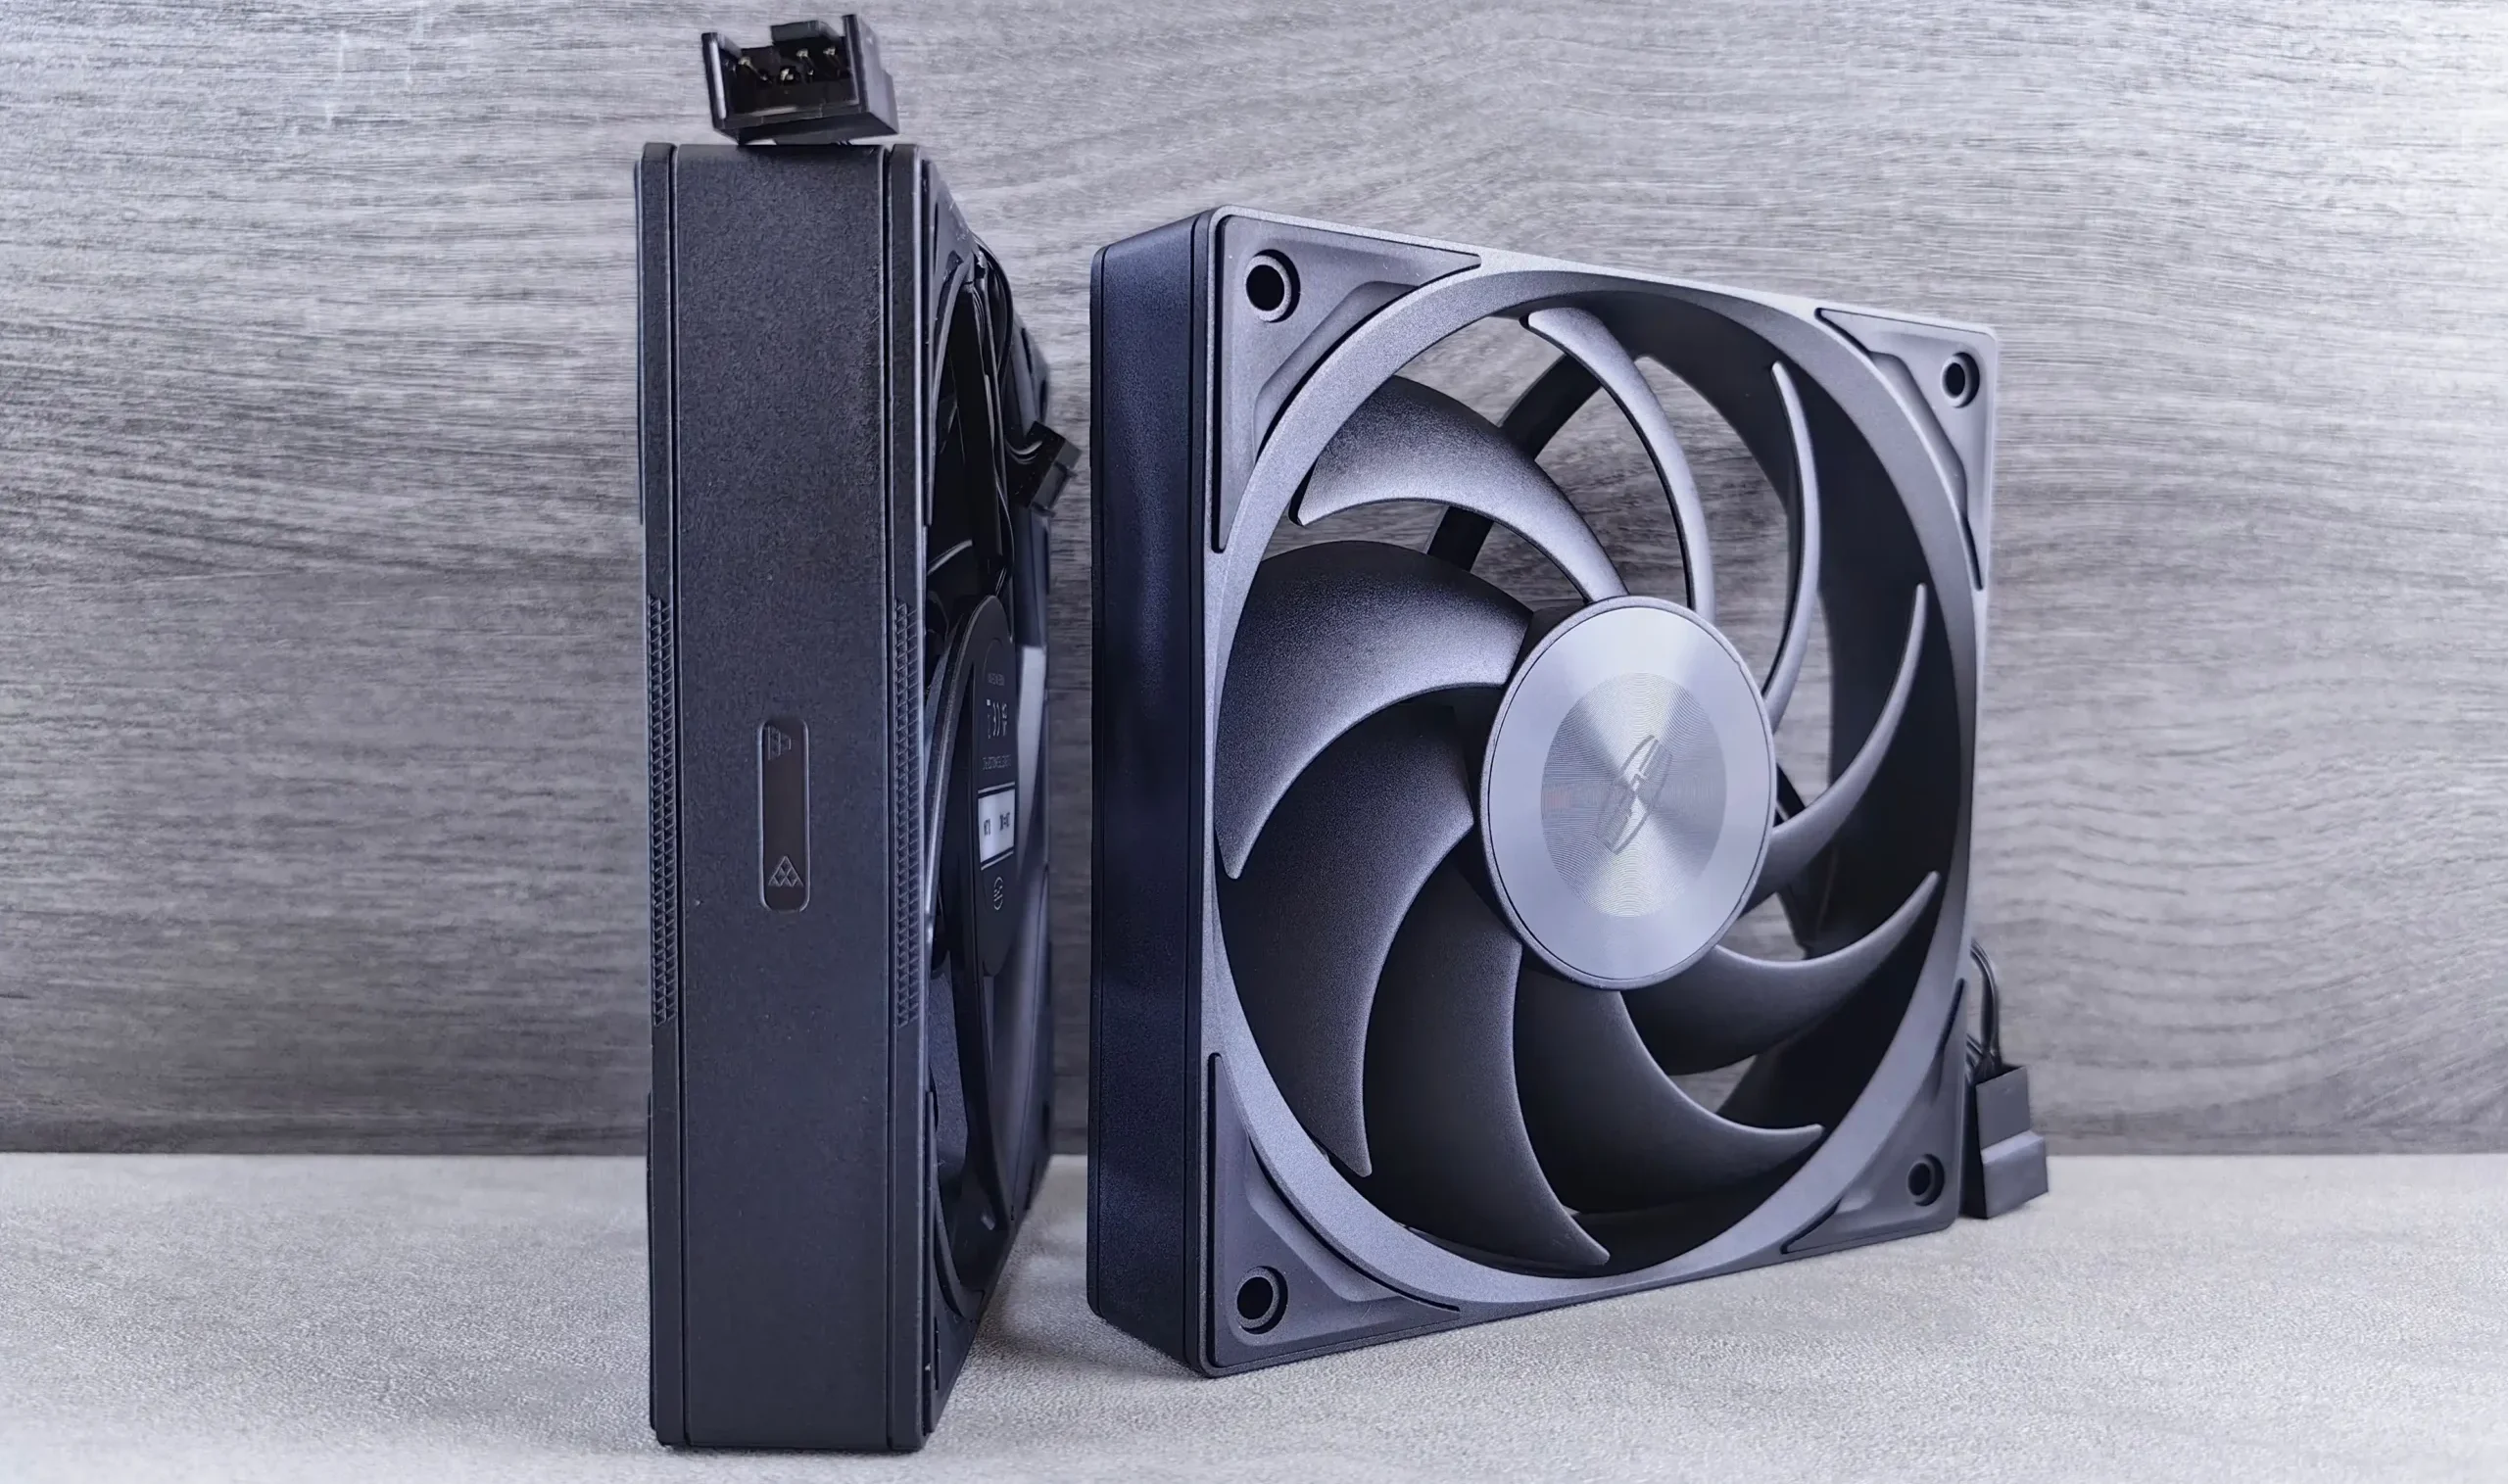
Balance Technology Inc. builds balancing machines and measurement systems for computer and data storage manufacturing — drive spindles and head readers, cooling fans and blower wheels, small motor rotors, and server and data centre fan modules. BTI has been designing this equipment in Whitmore Lake, Michigan since 1968.
Computing hardware sits at the extreme end of the balancing problem: the rotors are among the smallest and fastest anywhere in manufacturing. A drive spindle weighing a few tens of grams at high rotational speed has a permissible residual unbalance so small that fixturing and measurement resolution, not correction, set the limit on what is achievable.
What BTI Balances in Computing Hardware
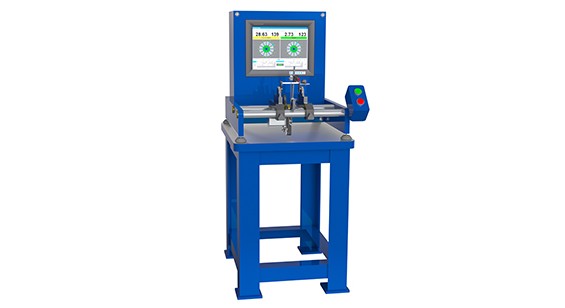
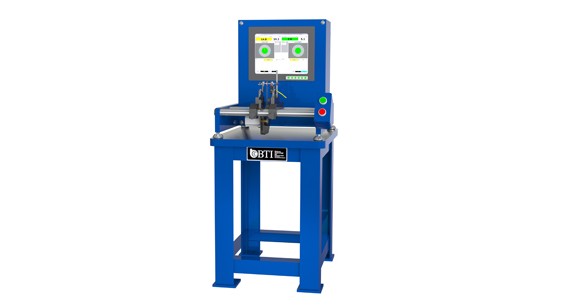
BTI balancing machines are built on four platforms — VNR (vertical non-rotator), H (horizontal cradle), VR (vertical rotator) and P (platform suspension) — plus spinners and test stands. The platform follows the part geometry and how it has to be held; the correction method follows the material and where there is room to add or remove mass.
| Component | Typical platform | Correction method |
|---|---|---|
| Drive spindles and head readers | Spinner, VR | Grind, weight-add |
| Cooling fans and blower wheels | VNR, VR | Drill, weight-add |
| Small motor armatures and rotors | H, VR | Mill, weight-add |
| Server and data centre fan modules | VNR, P | Weight-add |
| Optical and media drive spindles | Spinner | Grind |
| Precision spindles | VR, spinner | Grind, mill |
How a Machine Gets Sized
A BTI machine designation names a platform and a class. The number is a class, not a part weight limit — it describes the size and load envelope of the base.
Sizing works from the tooling and the part together, not the part alone. Tooling is not specified until the part prints are reviewed and the fixture is concepted, and the heavier the tooling-plus-part assembly is relative to the class, the less repeatable the measurement becomes. A shop that needs one machine to cover a wide range of parts, and does not need tight repeatability, can run a much broader weight range on a given class than a production program can.
Tell BTI the part weight and BTI will name a class the same day. See BTI machine platforms for the full platform and class architecture.
Balance Grade and Tolerance
Computing components run at the highest service speeds and the lowest masses of any industry BTI serves, which puts them at the tightest grades in the standard. Balance tolerances are set by ISO 21940-11, which superseded ISO 1940-1. The standard assigns a balance quality grade G, and the permissible residual specific unbalance follows from that grade and the service speed:
eper = (G × 60) ÷ (2π × n)
where eper is permissible residual specific unbalance in g·mm/kg, G is the balance quality grade in mm/s, and n is the service speed in rev/min. Permissible residual unbalance is then U = eper × m, divided across the correction planes.
| Grade | Typical components |
|---|---|
| G 6.3 | Cooling fans and normal electric armatures |
| G 2.5 | Small high-speed motor rotors and special armatures |
| G 1 | Precision spindles and drive assemblies |
| G 0.4 | The tightest grade in the standard, for precision grinder spindles |
Work out a specific tolerance with the ISO balance tolerance calculator.
Very Small Rotors at Very High Speed
Permissible residual unbalance scales with rotor mass and falls as service speed rises. Both terms work against you here at once: the rotors are light and they turn fast. The resulting tolerance is small enough that how repeatably the part is held becomes the dominant variable, ahead of the measurement system itself.
That makes this a tooling problem before it is a machine problem. BTI concepts the fixture from the part print, so the holding method, the drive and the correction access are settled together rather than in sequence. Where a surface is finished or coated and cannot be cut, correction moves to weight-add or to an operation earlier in the build.
Data Centre Cooling at Scale
Fan modules are a different problem from drive spindles, and an increasingly large one. Individually they are unremarkable; installed by the thousand in a single facility they are a meaningful contributor to acoustic load and to maintenance intervals. Residual unbalance that would be invisible in one unit becomes a fleet-level reliability figure when the same part ships in volume.
That argues for balancing as a production operation with consistent tolerance rather than a sampled check, which in turn shapes the machine specification around cycle time and part handling alongside measurement accuracy.
Correction Methods
| Method | Where it fits |
|---|---|
| Grind | Hardened and finished surfaces, including drive spindles |
| Mill | Controlled removal on a defined correction band |
| Drill | Components with material available to remove |
| Weight-add | Fan modules and assemblies where removal is not permitted |
| Adhesive and applied weight | Plastics, coated parts and finished assemblies |
Standards
BTI certifies machines to ISO 21940, SAE International balancing specifications, and DIN specifications. Where a program carries a measurement system capability requirement, BTI evaluates the part and the process first, then confirms what is achievable and commits to it in the machine specification.
Frequently Asked Questions
How small a rotor can BTI balance?
There is no fixed lower limit — it is a question of fixturing and measurement resolution. Send the part print and the service speed and BTI will confirm what is achievable before quoting.
Why is fixturing the limiting factor on small rotors?
Because the permissible residual unbalance is so small that any variation in how the part is located between runs is large relative to the tolerance. Repeatable holding is what makes the measurement meaningful.
Does BTI rebuild or retrofit existing balancing machines?
Yes, including machines built by other manufacturers. See BTI rebuilds and retrofits, competitor rebuilds and retrofits, and PC upgrades for machines still mechanically sound.
What information does BTI need to quote a machine?
The part print, the part weight, the service speed, the balance tolerance if one is specified, and the required production rate. Lead times are quoted in weeks at the time of quotation and move with current backlog.

Connect with us
To contact us regarding your project - or if you have any questions - please click the button below :
Request a QuoteGet Started
Get in touch with us. We're here to assist you.
Connect with our measurement experts and get the technical guidance your application demands.