Machine Tool
BTI builds balancing and measurement systems for machine tool manufacturing and tool rooms — spindles, tool holders, grinding wheels and the motor rotors that drive them. In a machine tool the balance problem is recursive: the machine that cuts a part to tolerance has to hold a tighter balance tolerance than the part it is cutting.
What BTI Balances in Machine Tool
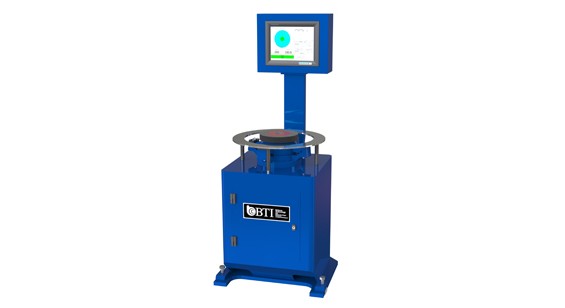
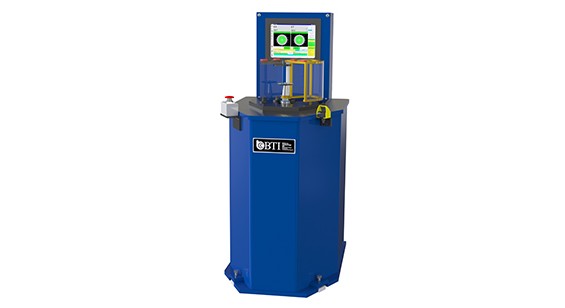
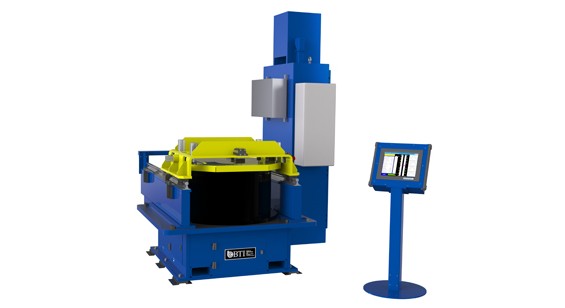
BTI balancing machines are built on four platforms — VNR (vertical non-rotator), H (horizontal cradle), VR (vertical rotator) and P (platform suspension) — plus tool holder balancers, spinners and test stands. The platform follows the part geometry and how it has to be held; the correction method follows the material and where there is room to add or remove mass.
| Component | Typical platform | Correction method |
|---|---|---|
| Spindles and spindle cartridges | H | Mill, grind |
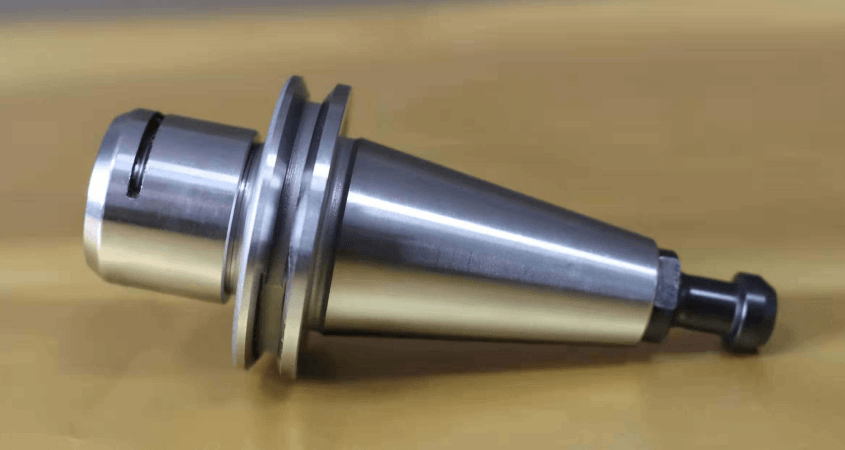
| Tool holders (HSK, CAT, BT) | THB | Set-screw, ring |
| Grinding wheels and adaptors | VNR, VR | Weight-add |
| Spindle motor rotors | H | Mill, drill |
| Chucks, faceplates and fixtures | VNR | Drill |
How a Machine Gets Sized
A BTI machine designation names a platform and a class. A P-5 is the platform suspension base, class 5. The number is a class, not a part weight limit — it describes the size and load envelope of the base.
Sizing works from the tooling and the part together, not the part alone. Tooling is not specified until the part prints are reviewed and the fixture is concepted, and the heavier the tooling-plus-part assembly is relative to the class, the less repeatable the measurement becomes. A shop that needs one machine to cover a wide range of parts, and does not need tight repeatability, can run a much broader weight range on a given class than a production program can.
Tell BTI the part weight and BTI will name a class the same day. See BTI machine platforms for the full platform and class architecture.
Balance Grade and Tolerance
Balance tolerances are set by ISO 21940-11, which superseded ISO 1940-1. The standard assigns a balance quality grade G, and the permissible residual specific unbalance follows from that grade and the service speed:
eper = (G × 60) ÷ (2π × n)
where eper is permissible residual specific unbalance in g·mm/kg, G is the balance quality grade in mm/s, and n is the service speed in rev/min. Permissible residual unbalance is then U = eper × m, divided across the correction planes.
| Grade | Typical components |
|---|---|
| G 2.5 | Machine-tool drives |
| G 1 | Grinding-machine drives, small armatures with special requirements |
| G 0.4 | Spindles, discs and armatures of precision grinders |
G 0.4 is the tightest grade in ISO 21940-11, and it belongs to this industry.
Work out a specific tolerance with the ISO balance tolerance calculator.
Balance the Tool, Not Only the Machine
A perfectly balanced spindle turning an unbalanced tool holder still produces chatter. At high spindle speeds a small residual unbalance generates force that shows up directly in surface finish and tool life, because unbalance force rises with the square of rotational speed. This is why tool holder balancing is a shop-floor operation rather than a one-time OEM step, and why BTI builds tool holder balancers as a standard model line.
Correction Methods
| Method | Where it fits |
|---|---|
| Drill | Cast and forged parts with material available to remove |
| Mill | Controlled removal on a defined correction band |
| Grind | Hardened or finished surfaces |
| Weld-on weight | Shafts and assemblies, adding rather than removing mass |
| Clip-on or press-on weight | Wheels, fan wheels and rims |
| Adhesive and applied weight | Modules, plastics and assemblies |
Standards
BTI certifies machines to ISO 21940, SAE International balancing specifications, and DIN specifications. Where a program carries a measurement system capability requirement, BTI evaluates the part and the process first, then confirms what is achievable and commits to it in the machine specification.
Frequently Asked Questions
Does a tool holder need rebalancing after a tool change?
Any change to the assembly changes its unbalance. Shops running high-speed spindles typically balance the holder-and-tool assembly as a unit rather than the holder alone.
What balance grade does a grinding spindle need?
ISO 21940-11 places spindles, discs and armatures of precision grinders at G 0.4, the tightest grade in the standard. General machine-tool drives sit at G 2.5.
Does BTI rebuild or retrofit existing balancing machines?
Yes, including machines built by other manufacturers. See BTI rebuilds and retrofits, competitor rebuilds and retrofits, and PC upgrades.
How are BTI lead times quoted?
Lead times are quoted in weeks at the time of quotation. They move with current backlog, so BTI confirms the schedule for a specific machine as part of the quote rather than publishing a fixed figure.
What information does BTI need to quote?
The part print, the part weight, the service speed, the balance tolerance if one is specified, and the required production rate.
Related applications: spindle and tool holder balancers, armatures, rotors and motor assemblies. Related equipment: machine tool equipment, balancers.

Connect with us
To contact us regarding your project - or if you have any questions - please click the button below :
Request a QuoteGet Started
Get in touch with us. We're here to assist you.
Connect with our measurement experts and get the technical guidance your application demands.